High-Efficiency belt conveyors Solutions for US Industrial Logistics

Optimizing material handling across North America with precision-engineered components for maximum throughput and minimal downtime.

High-Efficiency belt conveyors Solutions for US Industrial Logistics

Providing the United States manufacturing sector with robust, continuous transport systems designed for heavy-duty industrial environments.

Material Handling Landscape in the United States

Analyzing the operational challenges of US-based continuous transport systems.

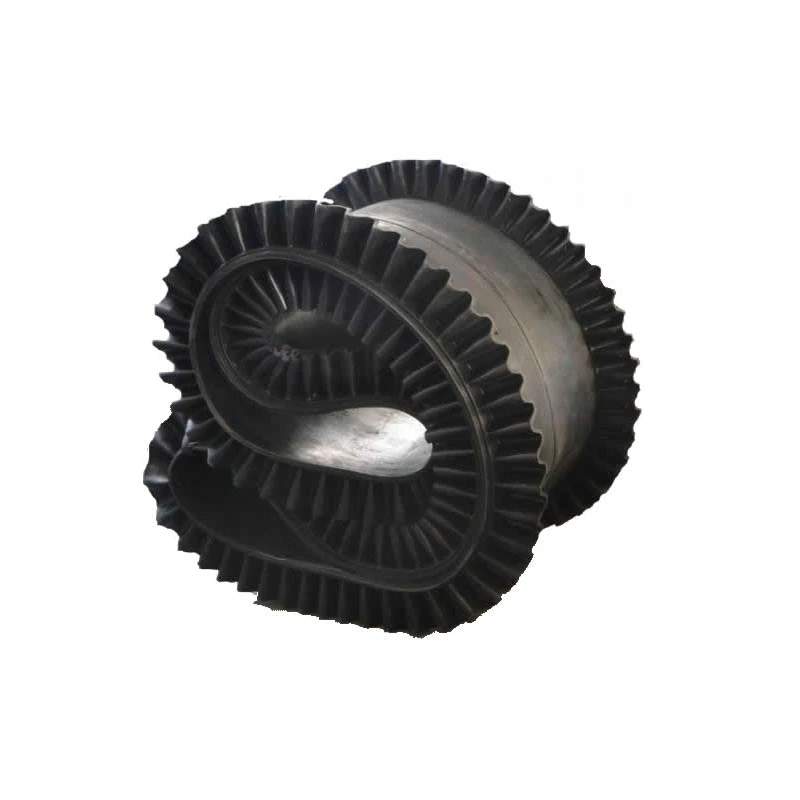
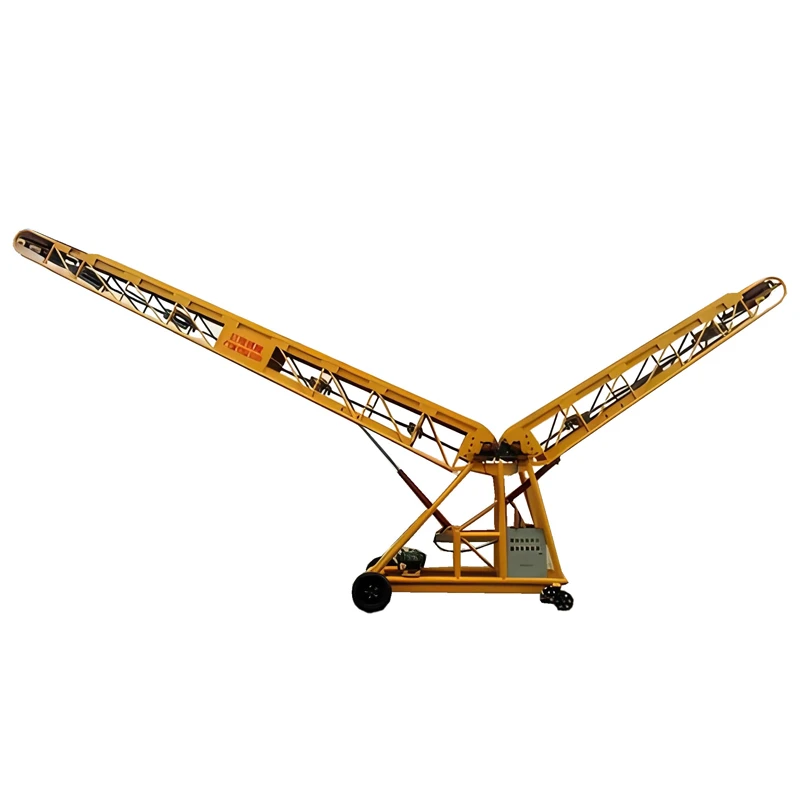
In the United States, the material handling industry faces unique pressures from the vast geographic scale of supply chains and the extreme climatic variations between the Midwest and the Sun Belt. Industrial facilities increasingly rely on high-performance conveyor belt systems to bridge the gap between automated production and logistics hubs.

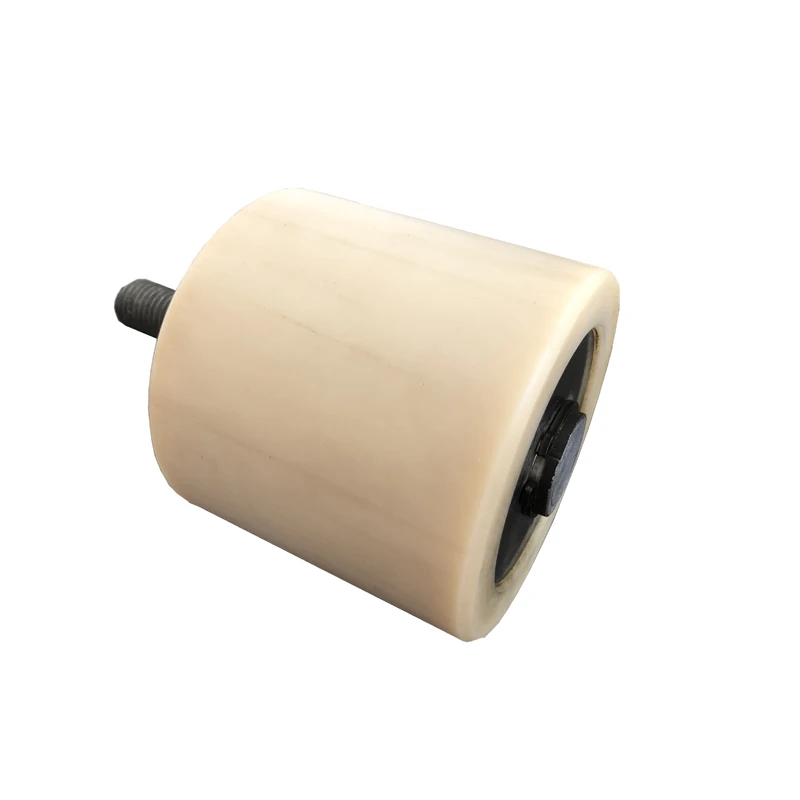
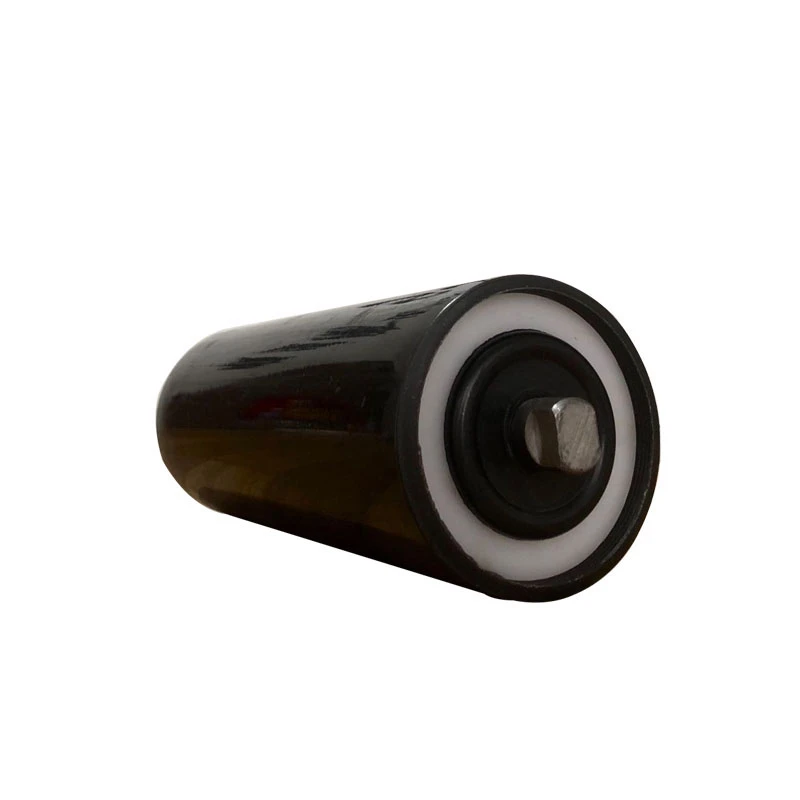
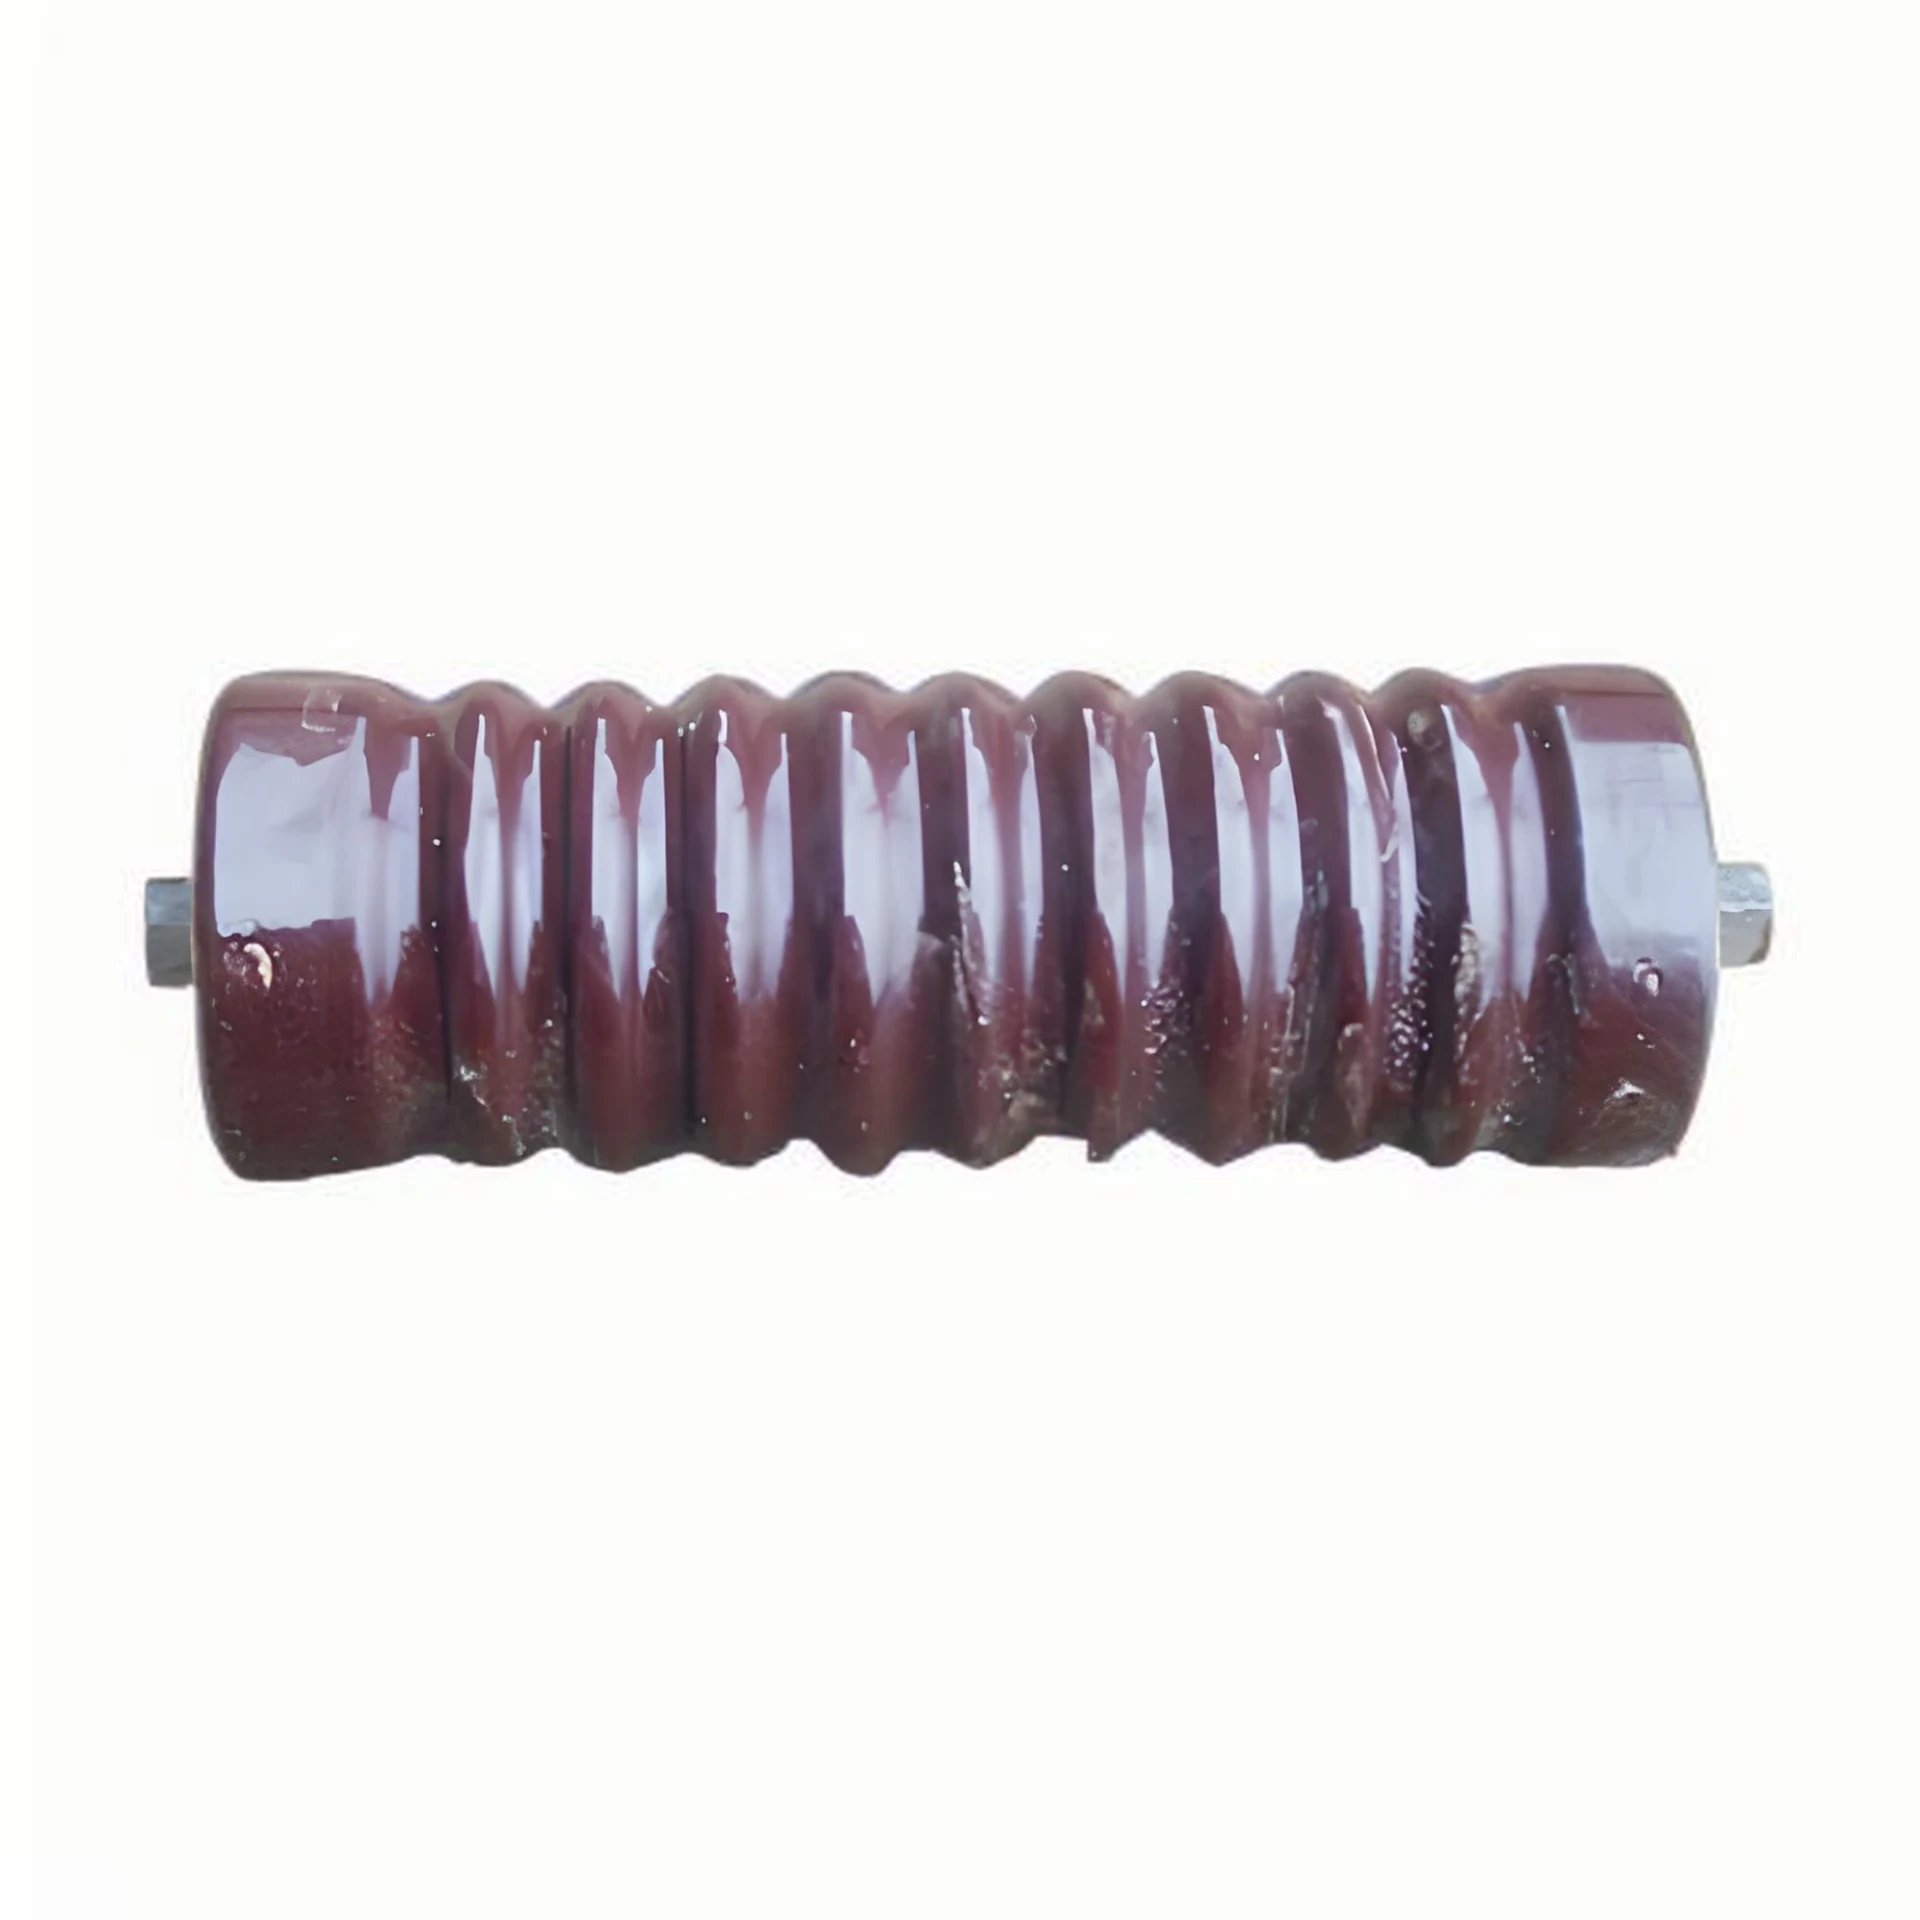
Labor shortages in the US manufacturing sector have accelerated the demand for autonomous and low-maintenance systems. This has led to a surge in the adoption of specialized components like the impact roller, which reduces belt wear in high-load loading zones, thereby lowering the frequency of manual maintenance interventions.

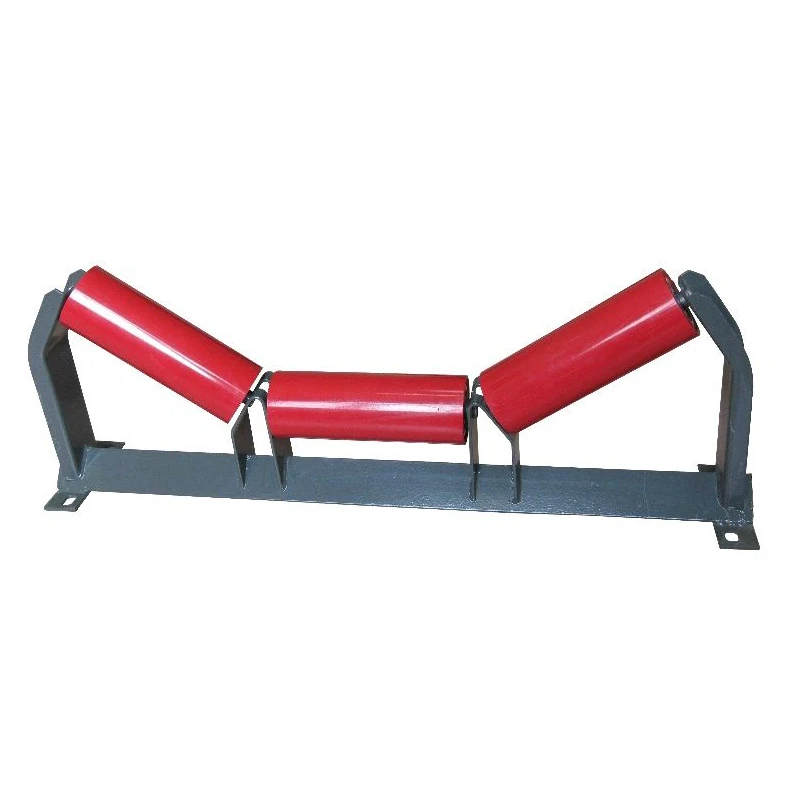
Furthermore, the push toward "Reshoring" in North America is revitalizing old industrial zones. These facilities require modernized gravity conveyor roller setups to integrate legacy warehouses with modern, high-speed sorting technologies, ensuring seamless flow in high-volume distribution centers.
Evolution of Continuous Conveying Technology

From mechanical simplicity to intelligent material flow.

Market Development History

During the early 20th century, US industry relied on basic rubber belts and heavy steel frames. The focus was purely on capacity, with little regard for energy efficiency or belt longevity, leading to frequent failures at transition points.

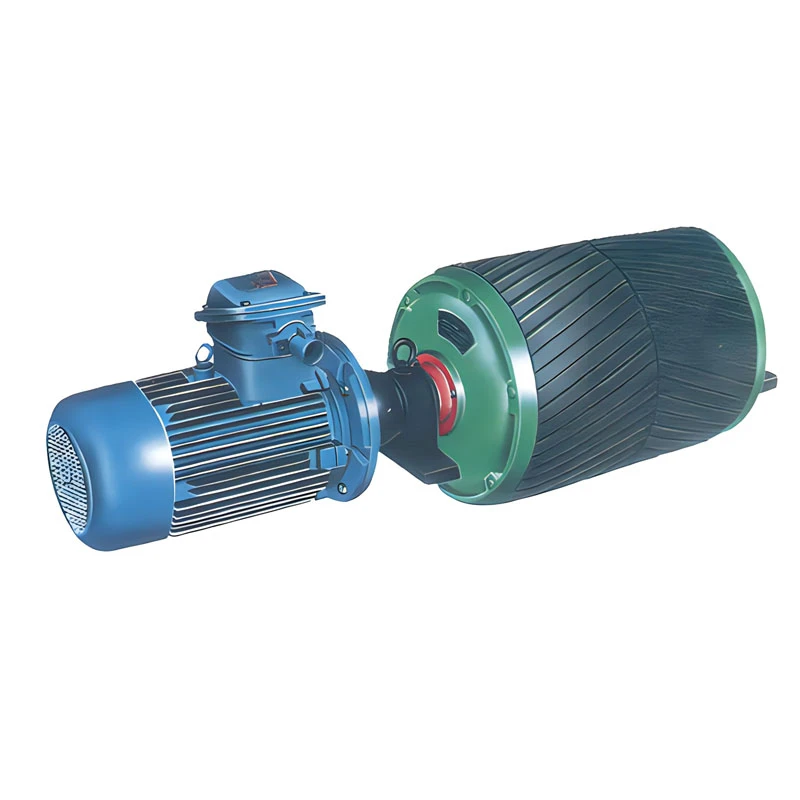
By the 1980s and 90s, the introduction of synthetic polymers and precision-machined pulleys, such as the specialized bend pulley, allowed for more complex conveyor geometries and reduced friction, significantly increasing the lifespan of the system.

Entering the 21st century, the shift moved toward "Smart Conveying." The integration of sensors and high-durability alloys has transformed the basic belt system into a data-driven asset capable of predictive maintenance and real-time load balancing.

Future Development Trends

IoT-Integrated Monitoring

Future systems will embed sensors directly into rollers to monitor heat and vibration, predicting failures before they stop the production line.

Sustainable Material Composites

The industry is moving toward biodegradable and recycled polymers for belts to meet stringent US environmental regulations.

Energy-Recovery Systems

Development of regenerative braking in decline conveyors to feed electricity back into the plant's power grid.

Industry Trends and Future Outlook

Strategic forecasting for North American continuous transport equipment.


AI-Driven Predictive Maintenance
Utilizing machine learning to analyze roller wear patterns and automate replacement schedules.

Modular System Design
Standardized components for rapid deployment and scaling in e-commerce fulfillment centers.

Low-Friction Coatings
Advanced nano-coatings for rollers to reduce energy consumption and noise pollution.

Hybrid Material Belts
Combining steel cord strength with polymer flexibility for extreme-duty mining applications.

Industry Outlook

The US market is shifting from simple bulk transport to "intelligent sorting." Based on current search trends, there is a significant increase in queries regarding energy-efficient conveyor components, signaling a transition toward Green Manufacturing.

Over the next 3-5 years, we expect a convergence of robotics and conveyor systems, where the conveyor is no longer a passive tool but an active part of the AI warehouse ecosystem, optimizing paths in real-time.

Localized Application Scenarios in North America

Tailored solutions for the diverse industrial needs of the United States.

01. Midwest Agricultural Processing

Handling heavy grain and seed loads using reinforced belt systems and high-impact rollers to withstand the abrasive nature of organic materials during peak harvest seasons.

02. East Coast E-commerce Hubs

Implementing high-speed gravity conveyor roller arrays in sorting centers to manage the massive volume of last-mile delivery parcels.

03. Western Mining & Mineral Extraction

Deploying heavy-duty belts and specialized bend pulleys in steep-incline environments of the Rocky Mountains to ensure stable ore transport.

04. Southern Automotive Assembly Lines

Integrating precision-timed conveyor belts for chassis movement, ensuring millimeter-accuracy in robotic welding and assembly cells.

05. Gulf Coast Petrochemical Plants

Using corrosion-resistant conveyor components designed to survive the high humidity and salty air of coastal industrial zones.

Brand Story

Global Development Journey of Hebei Roulle Machinery Equipment Technology Co., Ltd.

Foundation & Engineering Focus

Established with a vision to solve the most critical friction and wear problems in continuous transport, focusing on precision metallurgy.

Technological Breakthroughs

Developed proprietary alloy coatings that extended the lifespan of rollers by 40%, setting a new industry standard for durability.

Expansion into North America

Localized our product line to meet ASTM standards, ensuring seamless integration into the US industrial infrastructure.

Innovation in Automation

Launched the first generation of "Smart-Ready" components, enabling digital integration for global logistics giants.

Global Leadership Vision

Striving to become the world's most trusted partner for sustainable and efficient material handling solutions.

Comprehensive Product Portfolio for the US Market

Engineered components for seamless integration into North American industrial standards.

Common Questions for US Industrial Operators

Expert answers to the most frequent technical queries in material handling.

How to choose the right conveyor belt material for extreme US winter climates?

For cold climates, we recommend low-temperature resistant rubber or PVC compounds that maintain flexibility and prevent cracking at sub-zero temperatures.

What is the typical lifespan of an industrial impact roller in high-load zones?

Depending on the material, a high-quality impact roller typically lasts 12-24 months; however, using reinforced shells can extend this by 50%.

Can a bend pulley be customized for specific belt widths in US manufacturing plants?

Yes, our pulleys are fully customizable to match specific belt widths and tension requirements to prevent belt slippage and edge wear.

How do gravity conveyor rollers improve efficiency in sorting centers?

They eliminate the need for powered motors in simple transfer zones, reducing energy costs and maintenance while maintaining rapid parcel flow.

What are the signs that my belt conveyors need urgent maintenance?

Look for belt misalignment, unusual vibration in the rollers, or audible squeaking, which usually indicates bearing failure.

Are your components compliant with US safety and industrial standards?

Absolutely. All our products are engineered to meet or exceed the relevant ASTM and ANSI standards for industrial safety and performance.

Ready to Optimize Your Material Flow?

Our engineering team is ready to provide custom conveyor solutions for your facility in the United States.

Contact Us Now

If you are interested in our products, you can choose to leave your information here, and we will be in touch with you shortly.