The efficiency of modern material handling depends heavily on the ability to manage high-impact loads without compromising system integrity. In heavy-duty industrial environments, the integration of an impact roller conveyor system ensures that materials are transitioned smoothly, reducing the risk of belt damage and operational downtime. By absorbing the energy of falling materials, these systems protect the core components of the conveyor line.
Across global mining, quarrying, and manufacturing sectors, the demand for durability has led to the development of specialized belts and rollers that can withstand extreme stress. The challenge lies in balancing tensile strength with flexibility, ensuring that the equipment can operate at high speeds over long distances while maintaining a low elongation rate. This balance is critical for maintaining precise tensioning and reducing maintenance costs.
To achieve maximum longevity, industries are increasingly turning to advanced steel wire rope technologies. When paired with a high-quality impact roller conveyor, these belts provide exceptional resistance to tearing and impact, making them indispensable for high-speed, long-distance transportation of heavy materials.
The Mechanics of High-Impact Conveying Systems
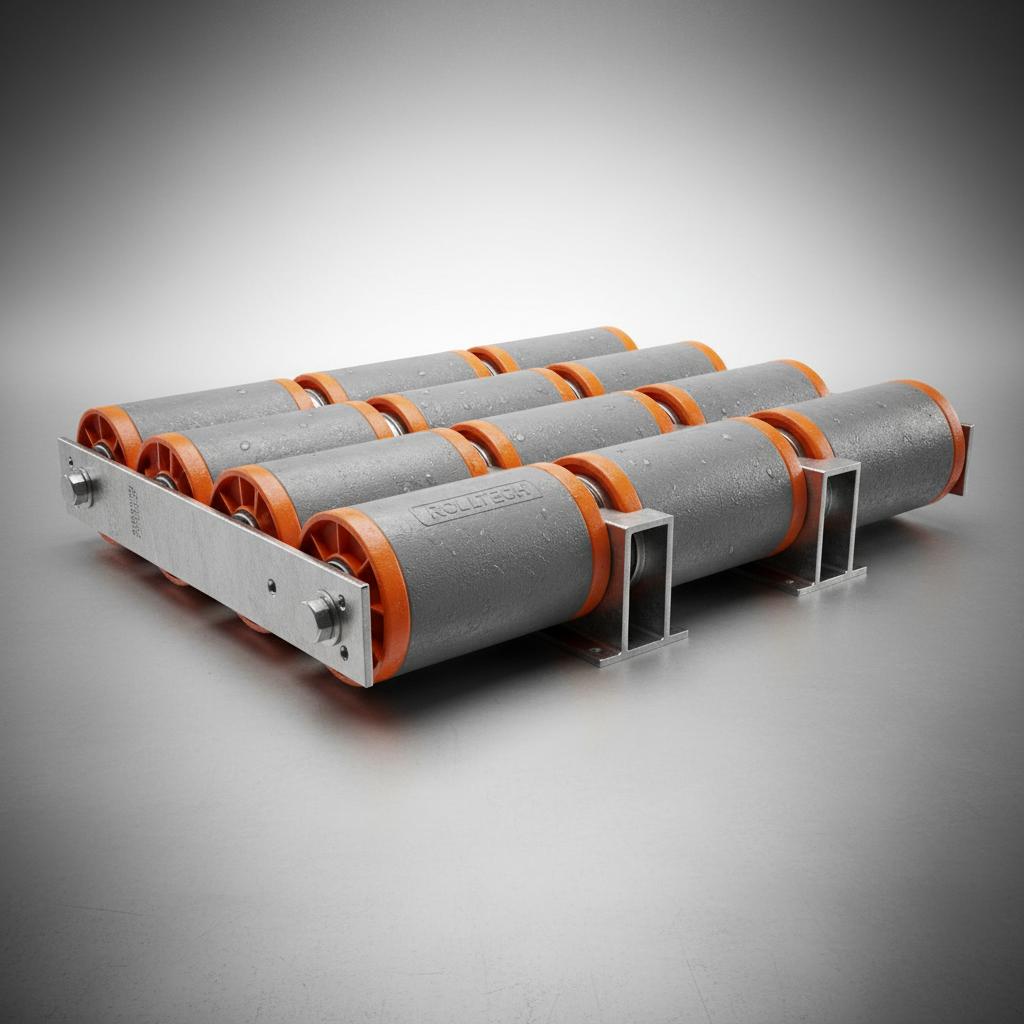
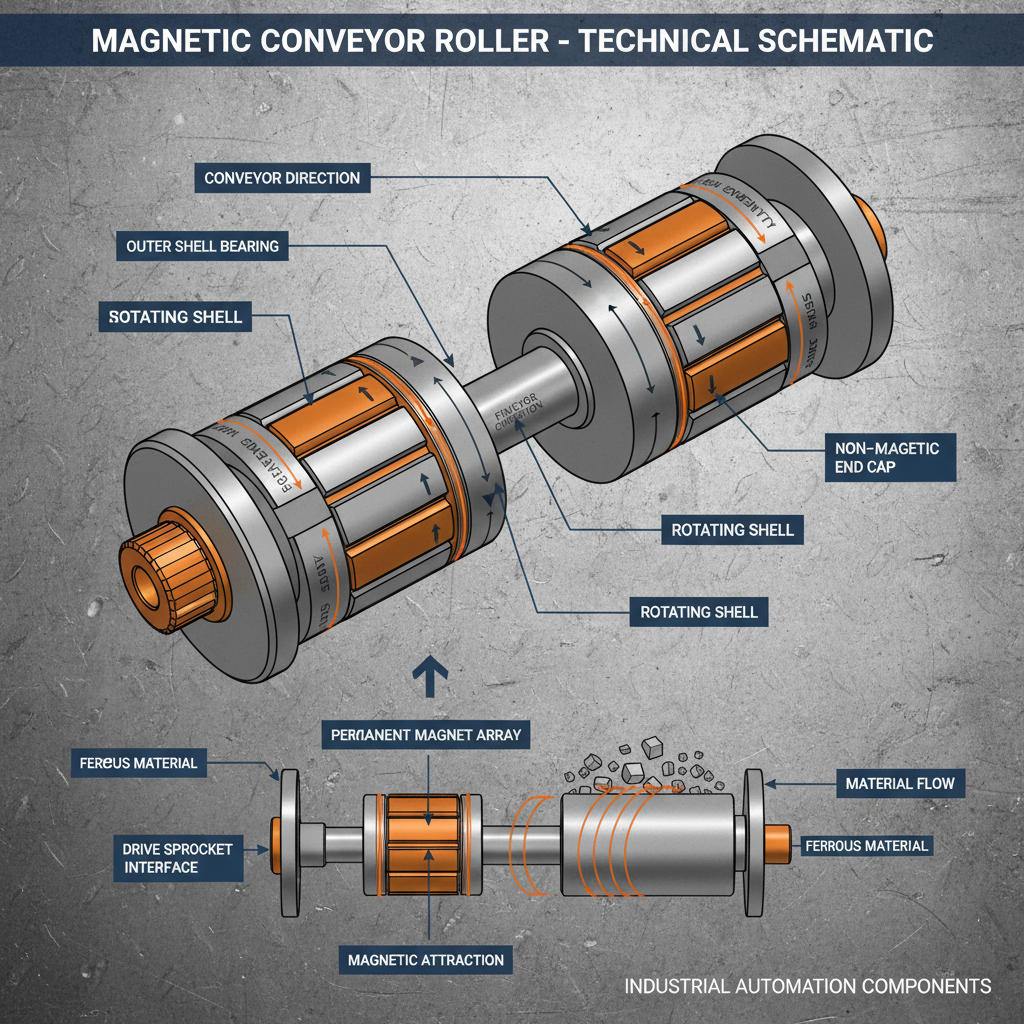
High-impact conveying systems are designed to handle the brutal force of material loading, where heavy lumps of ore or aggregates drop from significant heights onto the belt. An impact roller conveyor works by utilizing specialized rollers that absorb and distribute the shock, preventing the belt from bottoming out against the frame and avoiding premature carcass failure.
The synergy between the impact-absorbing rollers and the belt's own elasticity is what defines the system's efficiency. By utilizing a steel wire rope skeleton, the belt maintains its shape and linear running performance even under extreme dynamic loads, ensuring that material flow remains constant and the risk of misalignment is minimized.
Material Composition for Enhanced Durability
The structural integrity of an impact-resistant system begins with the belt's composition. A steel wire rope conveyor belt is engineered as a composite, featuring a core of high-strength rubber and steel wire ropes. This combination allows for a high safety factor and exceptional tensile strength, which is necessary for the high-speed demands of modern material handling.
Beyond the skeleton, the cover layers play a pivotal role in protecting the inner wire. These layers are designed to be anti-mold, anti-moth, and anti-aging, ensuring that the belt can withstand harsh environmental exposure. The use of high-quality rubber provides the necessary heat resistance and tear strength required for industrial longevity.
Furthermore, the edge adhesive and core adhesive ensure that the steel wire is firmly bonded to the rubber. This seamless integration results in excellent dynamic performance, allowing the belt to flex and bend without the wire rope detaching or causing internal friction, which is a common failure point in lower-grade belts.
Core Benefits of Steel Wire Rope Integration
One of the most significant advantages of integrating steel wire rope into an impact roller conveyor setup is the dramatic reduction in elongation. Unlike fabric-based belts that stretch significantly over time, steel wire rope belts exhibit extremely small elongation, which means shorter tensioning stroke distances and fewer manual adjustments.
The combination of a soft body and good groove-forming ability allows the impact roller conveyor to handle varying material sizes more effectively. This flexibility ensures that the belt contours to the load, improving the linear running performance and reducing material spillage along the conveyor edges.
Finally, the reliability of the joints in these systems cannot be overstated. A well-constructed joint ensures a long service life and minimizes the risk of catastrophic failure during peak load periods. This reliability, coupled with the ability to refurbish the belt surface after damage, makes it a cost-effective solution for long-term operations.
Performance Metrics in Industrial Applications
Measuring the success of an impact roller conveyor installation requires looking at specific technical indicators. Key metrics include the tensile strength of the belt, the rate of elongation under load, and the wear rate of the cover rubber. For most heavy-duty applications, compliance with standards like GB9770 is essential to guarantee safety and performance.
Depending on the specific environment, users may opt for specialized types. For instance, the impact and tear resistance type can improve impact resistance by 1-2 times and tear resistance by 0.5-1 times compared to standard belts. In arctic conditions, cold-resistant types are utilized, maintaining operational flexibility at temperatures as low as -60 ℃.
Efficiency Rating of Different Impact Roller Conveyor Configurations
Global Applications and Use Cases
The application of the impact roller conveyor is widespread in the global mining industry, particularly in regions like Australia, Canada, and Brazil, where massive quantities of iron ore and copper are transported. In these settings, the belts must withstand not only the weight of the material but also the corrosive nature of the minerals.
Beyond mining, these systems are critical in large-scale power plants for coal handling and in cement factories for limestone transport. In remote industrial zones where maintenance access is limited, the low elongation and high durability of steel wire rope belts reduce the frequency of site visits, significantly lowering the total cost of ownership.
Overcoming Operational Challenges
One of the most common challenges in impact conveying is the "bottoming out" effect, where the belt is pushed completely through the roller, hitting the conveyor frame. This leads to rapid wear and eventual carcass failure. The solution is the strategic placement of impact idlers and the use of belts with high flexural flexibility, which distribute the load more evenly.
Another issue is the accumulation of debris in the rollers, which can lead to seizure and friction burns on the belt. Implementing high-quality bearing housings and using polymer-coated rollers can mitigate this risk. Regular monitoring of the belt's surface is also essential; since steel wire rope belts can be refurbished, surface damage can be repaired without replacing the entire belt.
Finally, the challenge of extreme temperature fluctuations can make standard rubber brittle. By utilizing cold-resistant rubber compounds that function at -60 ℃, operators in polar regions can maintain consistent throughput without the risk of the belt cracking under the stress of an impact roller conveyor system.
Technical Specifications and Standards
Ensuring a system meets industrial standards is the only way to guarantee safety in high-tension environments. All performance indicators for these belts are developed to comply with GB9770, providing a benchmark for tensile strength, elongation, and abrasion resistance. This standardization allows for interoperability and predictable performance across different equipment brands.
Customization is often necessary for unique industrial needs. Whether it is adjusting the covering adhesive for specific chemical resistance or increasing the rubber thickness for extreme impact zones, the ability to tailor the belt to the specific impact roller conveyor configuration is a key technical advantage.
The following table summarizes the core technical distinctions between standard and high-performance impact conveying components to assist in system selection.
Comparative Analysis of Impact Conveying Belt Specifications
| Belt Type |
Impact Resistance |
Elongation Rate |
Recommended Use |
| Standard Fabric |
Low |
High |
Light Material Handling |
| Steel Wire Rope |
Very High |
Very Low |
Long-distance / High-speed |
| Impact-Enhanced |
Extreme |
Low |
Heavy Ore Loading Zones |
| Cold Resistant |
Medium-High |
Low |
Arctic / Frozen Regions |
| Tear Resistant |
High |
Medium-Low |
Sharp Material Transport |
| Refurbished Steel |
High |
Very Low |
Cost-effective Maintenance |
FAQS
Steel wire rope belts provide exceptional tensile strength and minimal elongation compared to fabric belts. This allows them to handle the heavy dynamic loads encountered in impact zones without stretching, ensuring that the belt remains properly aligned on the rollers and reducing the need for frequent tensioning adjustments.
Yes, one of the primary advantages of these high-strength belts is that they can be refurbished. If the cover layer is damaged by sharp materials or excessive impact, the surface can be repaired or replaced without having to discard the expensive steel wire rope carcass, extending the overall life of the equipment.
The cold-resistant variety is engineered with specialized rubber compounds that maintain flexibility and impact absorption at temperatures as low as -60 ℃. This prevents the belt from becoming brittle, which would otherwise lead to cracking and failure when hit by heavy materials in arctic environments.
The impact and tear resistance type is specifically enhanced to improve impact resistance by 1-2 times and tear resistance by 0.5-1 times. This is achieved through modified rubber chemistry and denser carcass construction, making it ideal for loading points where materials are dropped from significant heights.
On the contrary, the high linear running performance and stability of steel wire rope belts actually help reduce misalignment. Because they do not stretch unevenly under load, the belt maintains a more consistent path across the rollers, provided the system is properly installed.
For high-performance conveyor belts, compliance with GB9770 is a key indicator of quality. This standard ensures that the belt meets specific requirements for tensile strength, adhesion between the rubber and the wire rope, and overall durability under industrial stress.
Conclusion
The integration of steel wire rope belts within an impact roller conveyor system represents the pinnacle of durability in material handling. By combining high tensile strength, minimal elongation, and exceptional impact resistance, these systems solve the most pressing challenges of heavy-duty transportation—reducing downtime, minimizing maintenance, and ensuring operational safety.
As industrial demands shift toward higher speeds and more extreme environments, investing in high-specification, standardized components is no longer optional but a necessity for competitiveness. We recommend conducting a thorough site analysis to determine whether a standard, tear-resistant, or cold-resistant configuration is best suited for your specific operational needs to maximize the ROI of your conveyor system. Visit our website: www.hgconveyorbelt.com