In the complex ecosystem of material handling, the stability of a conveyor system depends heavily on the components that support the belt throughout its entire cycle. One of the most critical yet often overlooked elements is the return roller, which ensures that the unloaded belt returns to the starting point without sagging or drifting. By providing consistent support, these rollers prevent belt misalignment and significantly reduce the mechanical stress placed on the entire system.
Globally, the demand for efficient bulk material transport has surged, pushing industries to optimize every millimeter of their conveyor lines. Without high-quality support in the return section, companies face frequent downtime due to belt deviations or premature wear. The integration of precision-engineered rollers allows for a seamless transition of the belt, ensuring that the circulation remains smooth and the energy consumption of the drive motor is kept to a minimum.
Understanding the technical nuances of the return roller is essential for any plant manager looking to lower maintenance costs and improve safety. From mining operations to airport logistics, these components play a pivotal role in enhancing operational stability and reducing the risk of belt loss of control.
The Fundamental Role of Return Rollers in Conveying
The return roller, often referred to as a parallel roller, is specifically designed for the return section of a conveyor system. Its primary function is to support the unloaded conveyor belt as it travels back toward the head pulley, ensuring that the belt maintains a flat profile and does not sag under its own weight. By maintaining this alignment, the roller prevents the belt from rubbing against the structure, which would otherwise lead to rapid edge wear and potential belt failure.
Beyond simple support, these rollers are crucial for the overall stability of the conveying system. When properly installed, they reduce frictional resistance, which in turn lowers the amount of torque required from the conveyor drive. This not only extends the lifespan of the belt but also contributes to a more stable and predictable flow of materials, effectively reducing the risk of accidents caused by belt misalignment or sudden loss of control.
Technical Design and Operational Efficiency
The efficiency of a conveyor system is often a reflection of its smallest parts. A well-engineered return roller is designed to minimize the rolling resistance, allowing the belt to glide with minimal energy loss. By focusing on the precision of the bearing housing and the smoothness of the roller shell, manufacturers can ensure that the belt circulates with maximum fluidity, which directly translates to higher conveying speeds and improved throughput for the facility.
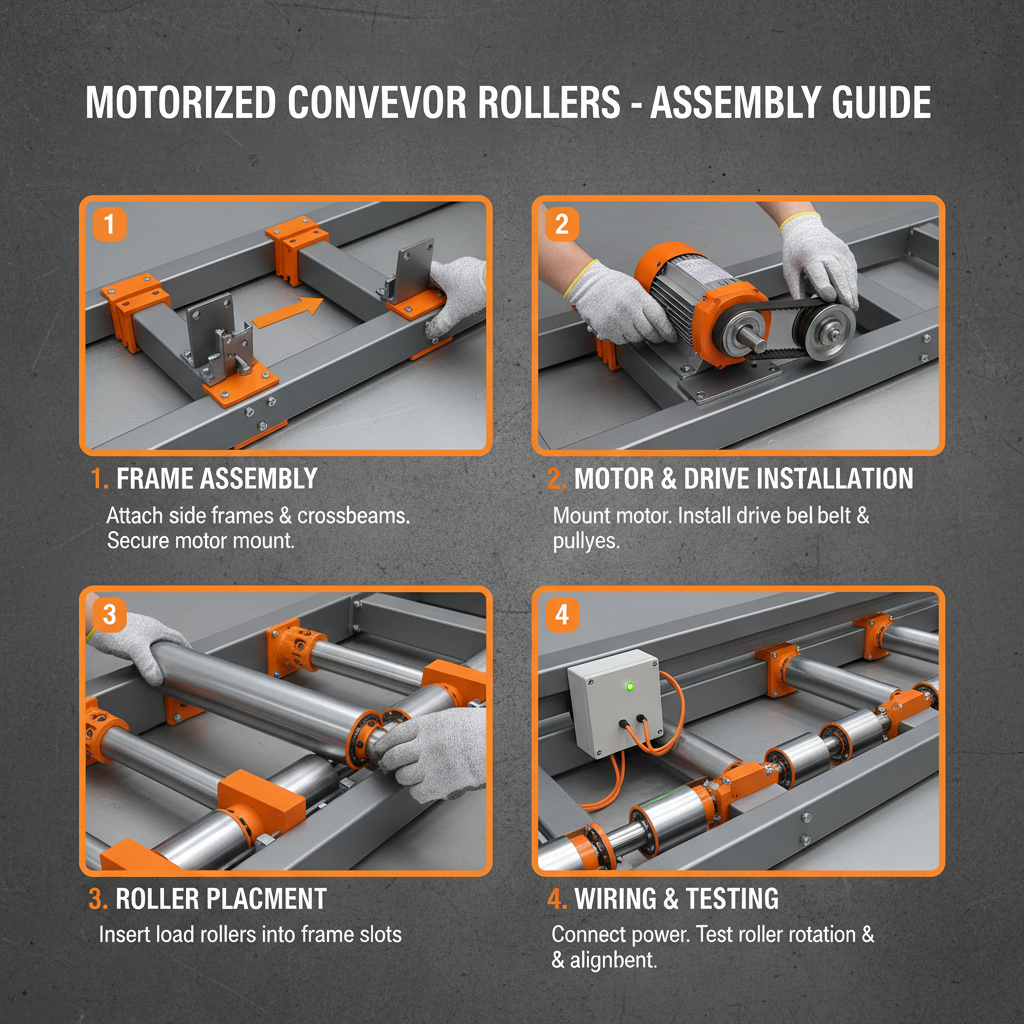
Maintenance is another critical factor in technical design. Modern rollers are built to be simple to understand, easy to install, and quick to replace. This modular approach means that logistics enterprises can perform routine checks and swaps without necessitating a complete system shutdown. The ability to rapidly replace a worn component ensures that the conveyor remains operational, minimizing costly downtime in high-pressure environments like ports or warehouses.
Furthermore, the operational stability provided by these rollers helps in balancing the tension across the belt width. By providing a consistent contact point, the return roller mitigates the vibrations that can occur during high-speed operations. This balance is essential for preventing the belt from shifting laterally, which is one of the most common causes of material spillage and structural damage in industrial conveyor setups.
Key Advantages for Logistics and Industrial Transport
One of the most immediate benefits of implementing high-quality return rollers is the drastic reduction in maintenance costs. Because these components reduce the frictional wear on the underside of the conveyor belt, the interval between belt replacements is extended. This logical cost-saving measure allows logistics companies to allocate resources toward other critical upgrades while maintaining a reliable transport line.
The high cost-effectiveness of the return roller makes it an attractive option for diverse sectors. Its simple design allows it to be used independently or coupled with other conveying equipment, such as impact idlers or self-aligning rollers. This versatility ensures that whether the environment is a dusty cement plant or a sterile pharmaceutical warehouse, the support system can be tailored to the specific needs of the operation.
From a safety perspective, the stability offered by a return roller is invaluable. By reducing the risk of belt drift and loss of control, these components protect workers from potential accidents associated with belt snaps or material overflows. The emotional peace of mind that comes from a stable, predictable system allows operators to focus on efficiency rather than constantly monitoring for equipment failure.
Comparative Performance of Support Components
When comparing different support mechanisms, the choice of roller diameter and material plays a significant role in overall performance. A larger diameter roller can often distribute the load more effectively, reducing the pressure on the belt surface, while specialized materials like polymers can offer better corrosion resistance in chemical environments. The goal is to find the perfect balance between load capacity and rotational efficiency.
To better understand how different configurations impact performance, we can look at a rating system based on operational efficiency, durability, and cost-effectiveness across various return roller types.
Performance Metrics for Different Return Roller Types
Global Industrial Applications and Versatility
The application of the return roller spans across nearly every major industrial sector. In the mining and steel industries, where heavy-duty materials are transported over vast distances, these rollers are essential for maintaining belt integrity under extreme loads. Similarly, in cement and power plants, they ensure that abrasive materials do not compromise the return journey of the belt, keeping the plant running 24/7.
Beyond heavy industry, these rollers are integral to modern logistics hubs. Airports, docks, and large-scale warehouses utilize them to power the sorting and distribution of parcels. The ability of the return roller to work in tandem with other conveying equipment makes it a universal solution for any facility that relies on continuous material movement to maintain its supply chain.
Sustainability and Environmental Impact
Environmental sustainability is becoming a primary driver in industrial equipment selection. The return roller contributes to a "greener" operation by effectively reducing electricity consumption. By lowering the rolling friction and improving the balance of the conveyor belt, the motor does not have to work as hard to pull the belt, resulting in a measurable decrease in energy usage over time.
Furthermore, the reduction of noise and dust pollution is a significant benefit. High-precision rollers operate more quietly than substandard alternatives, creating a better working environment for employees. By preventing belt misalignment, they also reduce the amount of material that spills onto the floor, which in turn minimizes the need for chemical cleaning agents and reduces airborne particulate matter.
The long-term value of using durable rollers also lies in waste reduction. Components that last longer mean fewer replacements and less industrial scrap entering landfills. This shift toward longevity and efficiency aligns with global ISO standards for sustainable manufacturing, proving that small technical improvements can lead to significant environmental gains.
Specifications and Selection Criteria for Rollers
Choosing the right return roller requires a deep understanding of the conveyor belt width and the specific environment of the application. The diameter of the roller and its length must be perfectly matched to the belt to avoid uneven pressure points. For instance, a belt width of 500mm typically requires a roller with a specific length to ensure full support across the return path.
Material selection is equally important. While steel is excellent for high-load applications, stainless steel is preferred for the chemical and food industries due to its corrosion resistance. The bearing type and housing seal also determine how well the roller will perform in wet or dusty conditions, making the technical specifications the most critical part of the procurement process.
To assist in the selection process, the following table outlines the standard sizing and matching for common return roller configurations used across various industries.
Standard Return Roller Specifications and Belt Compatibility
| Roller Model (DiaLength) |
Compatible Belt Width |
Primary Industry Use |
Load Capacity Score |
| Φ89600mm |
500mm |
Logistics/Warehouse |
6/10 |
| Φ89750mm |
650mm |
Chemical/Power |
7/10 |
| Φ89950mm |
800mm |
Cement/Mining |
8/10 |
| Φ1081150mm |
1000mm |
Steel/Heavy Mining |
9/10 |
| Φ1081400mm |
1200mm |
Port/Bulk Cargo |
10/10 |
| Φ1081600mm |
1400mm |
Heavy Industrial |
10/10 |
FAQS
The carry roller is designed to support the belt while it is loaded with materials, often utilizing a trough shape to center the material. In contrast, the return roller is a parallel cylinder used on the underside of the belt to support it while unloaded, ensuring smooth circulation back to the start.
Inspection intervals vary by industry, but in high-dust environments like mining or cement, monthly checks are recommended. Signs of wear include abnormal noise, visible flat spots on the roller shell, or belt drifting, all of which indicate the roller needs replacement to prevent belt damage.
Yes, provided the correct materials are selected. For corrosive environments, stainless steel rollers or specialized polymer-coated rollers are used to prevent oxidation and chemical degradation, ensuring the longevity of the conveyor system in acid or alkali conditions.
By providing a smooth, low-friction surface for the unloaded belt, the return roller reduces the overall rolling resistance of the system. This means the conveyor drive motor requires less energy to move the belt, leading to lower electricity bills and reduced carbon emissions.
Misalignment can cause the conveyor belt to track off-center, leading to edge wear and potential spillage. It can also create uneven tension across the belt, which increases the risk of belt tearing and puts unnecessary strain on the bearings of other rollers in the system.
Generally, yes. As long as the roller width matches the conveyor belt width and the material of the roller is compatible with the belt's operational environment (e.g., heat-resistant or cold-resistant), they can be used with most standard rubber, PVC, or steel-cord belts.
Conclusion
The return roller is an indispensable component of any professional conveying system, providing the critical support necessary for the unloaded belt to return smoothly and stably. By reducing friction, preventing belt misalignment, and lowering maintenance costs, it transforms a simple belt loop into a high-efficiency industrial tool. Whether applied in the rigorous conditions of a mine or the fast-paced environment of a logistics hub, its role in enhancing safety and operational throughput cannot be overstated.
As industries move toward greater automation and sustainability, the focus on precision components like the return roller will only grow. Investing in high-quality, correctly sized rollers is not just a maintenance decision, but a strategic move to improve the total cost of ownership and environmental footprint of your material handling operations. For more information on high-performance conveyor parts, visit our website: www.hbroule.com