In the complex world of material handling, the stability of the return journey is just as critical as the loaded delivery. The belt conveyor return roller serves as the unsung hero of this process, ensuring that the empty belt returns to the drive pulley without sagging, oscillating, or wearing prematurely. By providing continuous support to the underside of the belt, these rollers maintain the structural integrity of the entire conveyor loop.
Across global industrial sectors, from massive mining operations in Australia to automated logistics centers in Europe, the efficiency of a system is often judged by its uptime. A failure in the return path can lead to belt misalignment or catastrophic tears, resulting in costly downtime. Consequently, selecting a high-performance return roller is not merely a maintenance choice but a strategic decision to ensure operational continuity and safety.
Understanding the technical nuances of the belt conveyor return roller allows engineers to optimize energy consumption and reduce mechanical stress. When integrated with a robust drive system, such as those provided by Hebei Roule, these rollers work in harmony to create a seamless flow of materials. Investing in premium return components ensures that the belt remains centered and protected throughout its entire cycle.
Global Relevance of Belt Conveyor Return Roller
On a global scale, the demand for efficient bulk material handling is rising in tandem with the expansion of the mining and infrastructure sectors. According to ISO standards for conveyor components, the precision of the return path is paramount to preventing belt drift. The belt conveyor return roller is essential in these high-capacity environments to ensure that the belt maintains its trajectory, thereby reducing the risk of edge damage and unexpected system failures.
In regions with extreme climates, such as the frozen terrains of Canada or the humid jungles of Southeast Asia, the environmental stress on return rollers is immense. Without specialized materials, standard rollers succumb to corrosion or seizing, which increases the friction on the belt and places additional strain on the drive motor and reducer. This global challenge necessitates the development of rollers that can withstand abrasive dust and extreme temperature fluctuations.
Defining the Belt Conveyor Return Roller
A belt conveyor return roller is a specialized cylindrical component installed beneath the return side of a conveyor belt. Unlike carry rollers, which support the load, the return roller's primary purpose is to support the empty belt as it travels back from the discharge end to the loading point. It prevents the belt from sagging between support intervals, which would otherwise increase the tension required from the drive motor and lead to inefficient power consumption.
In modern industrial contexts, these rollers are more than just simple pipes; they are engineered precision tools. They often incorporate advanced bearings and sealed housings to prevent the ingress of contaminants. By maintaining a flat or slightly V-shaped profile, they help in the automatic centering of the belt, ensuring that the system operates within a tight tolerance to avoid rubbing against the conveyor frame.
From a humanitarian and safety perspective, the reliability of the return roller reduces the need for frequent manual interventions in dangerous industrial zones. When a belt slips or deviates due to a failed return roller, workers are often forced to perform emergency adjustments near moving parts. High-quality, low-maintenance rollers minimize these risks, enhancing the overall safety culture of the manufacturing plant.
Core Components for Maximum Durability
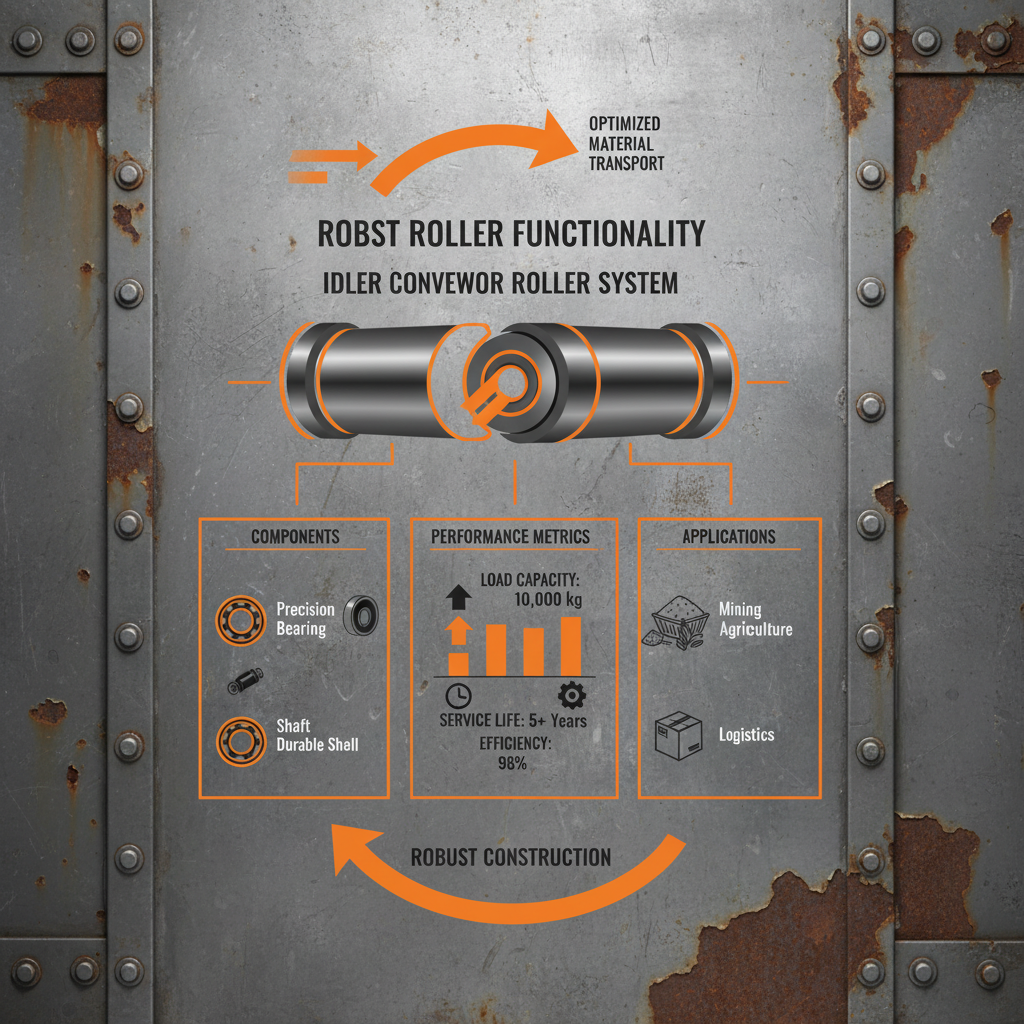
The durability of a belt conveyor return roller depends heavily on its material composition. High-grade steel tubes are common, but for corrosive environments, stainless steel or polymer coatings are employed. The shell must be perfectly concentric to avoid vibration, which could otherwise transfer stress to the conveyor's structural frame and reduce the lifespan of the overall system.
At the heart of every belt conveyor return roller is the bearing assembly. Precision-engineered bearings, often paired with robust bearing housings, ensure low rolling resistance. This reduction in friction is critical because it directly lowers the torque demand on the conveyor motor, contributing to significant energy savings over thousands of operational hours.
Sealing technology is the final pillar of reliability. Advanced labyrinth seals or rubber gaskets prevent dust, water, and abrasive particles from entering the bearing race. When the belt conveyor return roller is properly sealed, it can operate for years without lubrication, which is especially vital in remote mining sites where maintenance access is limited.
Industrial Applications and Use Cases
In the mining and metallurgy industries, the return path is often exposed to falling debris and abrasive dust. Here, heavy-duty belt conveyor return roller configurations are used to prevent "material build-up," which can cause the belt to track off-center. By utilizing V-shaped return rollers, operators can naturally guide the belt back to the center without requiring constant manual adjustment.
In food processing and pharmaceutical plants, hygiene is the priority. In these scenarios, the belt conveyor return roller is typically constructed from stainless steel or food-grade polymers. These materials prevent contamination and allow for high-pressure wash-downs. The seamless design ensures that no organic matter traps in the roller gaps, maintaining strict compliance with global health and safety regulations.
Efficiency Impact of Different Return Roller Materials
Long-Term Value and Reliability
The long-term value of investing in a premium belt conveyor return roller manifests in the reduction of Total Cost of Ownership (TCO). While lower-cost alternatives may seem attractive initially, they often lead to increased belt wear and more frequent replacement cycles. A high-quality roller reduces the friction coefficient, which means the conveyor motor operates more efficiently, leading to lower electricity bills over the life of the equipment.
Beyond the financial gains, there is the element of operational trust. When a plant manager knows that the return path is supported by reliable components, the anxiety surrounding unexpected shutdowns vanishes. This reliability fosters an environment of innovation, where the focus shifts from "fixing what is broken" to "optimizing for higher throughput," ultimately driving the company's competitive edge in the global market.
Future Trends in Roller Technology
The industry is moving toward "smart conveyors," where the belt conveyor return roller is integrated with IoT sensors. These sensors can monitor vibration levels and temperature in real-time, alerting maintenance teams to a failing bearing before it causes a belt tear. This shift from reactive to predictive maintenance is a cornerstone of the Industry 4.0 transformation in material handling.
Sustainability is also driving a change in materials. We are seeing a rise in the use of recycled high-density polymers and bio-based lubricants within the roller assemblies. These innovations reduce the environmental footprint of the conveyor system without sacrificing the load-bearing capacity or the lifespan of the return rollers.
Furthermore, the integration of self-aligning mechanisms is becoming standard. Future return rollers will likely feature adaptive geometries that adjust to belt tension changes automatically, further reducing the need for manual tracking adjustments and enhancing the overall autonomous capability of the conveyor line.
Overcoming Common Operational Challenges
One of the most persistent challenges is material build-up on the return roller, which can distort the roller's shape and push the belt off course. To solve this, engineers often pair the belt conveyor return roller with high-efficiency belt cleaners. These cleaners remove debris from the belt before it reaches the return path, ensuring the rollers remain clean and functional.
Another common issue is the "seized roller" syndrome, where a bearing fails and the roller stops spinning, acting as a brake against the moving belt. This creates intense friction and can burn through the belt cover in a matter of hours. The solution lies in using high-performance seals and choosing bearings that are specifically rated for the humidity and dust levels of the specific operating environment.
Finally, belt mistracking remains a hurdle. By strategically spacing the return rollers and incorporating a few "trainer rollers" into the return path, operators can maintain perfect alignment. This systemic approach ensures that the belt conveyor return roller performs its role within a balanced ecosystem, maximizing the efficiency of the drive motor and reducer.
Comparative Analysis of Return Roller Configurations
| Roller Type |
Wear Resistance |
Alignment Ability |
Maintenance Need |
| Flat Steel Roller |
Moderate |
Low |
Medium |
| V-Shape Roller |
High |
Very High |
Low |
| Polymer Roller |
Very High |
Moderate |
Very Low |
| Stainless Roller |
Maximum |
Low |
Low |
| Rubber Coated |
Moderate |
Moderate |
Medium |
| Ceramic Roller |
Maximum |
Low |
Very Low |
FAQS
The carry roller is located on the top side of the conveyor and is designed to support the weight of the loaded material. In contrast, the belt conveyor return roller is located on the bottom side and supports the empty belt as it returns to the start. Return rollers focus more on belt alignment and reducing sag, whereas carry rollers focus on load distribution and weight capacity.
Inspection frequency depends on the environment. In heavy-duty mining, a monthly visual check is recommended. In clean warehouse environments, quarterly inspections may suffice. Key signs of wear include audible squeaking, visible flat spots on the roller shell, or belt mistracking, which often indicates a seized return roller.
Polymer rollers offer excellent corrosion resistance and lower weight, making them ideal for many settings. However, in extreme high-temperature environments or applications with massive belt tensions, steel rollers are still preferred for their superior structural rigidity and heat tolerance. The choice depends on the specific chemical and thermal load of the site.
Belt drift is often caused by material build-up on the rollers, which changes their diameter and pushes the belt sideways. It can also be caused by misaligned frames or a seized roller. Installing V-shaped return rollers or adding high-efficiency belt cleaners can significantly improve tracking stability.
Yes, significantly. A seized or worn belt conveyor return roller increases the rolling resistance (friction). This forces the motor and reducer to work harder to pull the belt, increasing energy consumption and heat generation. High-precision bearings in the return rollers ensure minimal resistance and optimal energy efficiency.
V-shaped return rollers act as a passive centering device. Because of their geometry, the belt naturally tends to settle in the center of the "V" groove. This reduces the frequency of manual tracking adjustments and prevents the belt edges from rubbing against the conveyor structure, thereby extending the belt's overall lifespan.
Conclusion
The belt conveyor return roller may seem like a simple component, but it is fundamental to the stability, safety, and efficiency of any material handling system. From the precision of its bearing assembly to the resilience of its outer shell, every detail contributes to the reduction of mechanical friction and the prevention of costly belt failures. By integrating high-quality return rollers with advanced drive systems and predictive maintenance, industrial operators can ensure a seamless, low-energy operational flow.
Looking forward, the transition toward smart, sensor-enabled rollers and sustainable materials will further redefine the standards of conveyor reliability. For companies aiming to minimize downtime and maximize throughput, prioritizing the quality of return path components is an essential strategy. We invite you to explore our full range of precision-engineered conveyor solutions to optimize your production line. Visit our website: www.hbroule.com