- Tel: +8615128135888
- Email: hg@chinaconveyerbelt.com

The global industrial landscape is witnessing a significant shift toward high-durability material handling systems, where the selection of a specialized conveyor belt company is becoming critical for operational continuity. In environments characterized by extreme humidity, chemical exposure, or strict hygienic mandates, standard carbon steel components often fail prematurely, leading to costly unplanned downtime and safety risks.
The core engineering challenge lies in balancing mechanical load-bearing capacity with chemical inertness. As industries like pharmaceutical manufacturing and chemical processing scale their automation, the demand for rollers that resist both oxidation and magnetic interference has surged, forcing a re-evaluation of traditional roller materials.
This analysis explores the technical superiority of stainless steel configurations over rubber and nylon alternatives, providing a framework for engineering teams to optimize their conveyor lifecycles and reduce long-term maintenance overhead.


The operational principle of a stainless steel roller is based on reducing the coefficient of friction between the moving belt and the support structure. As materials transition along the belt, the roller rotates around a precision-machined shaft, utilizing high-grade bearings to ensure continuous, low-resistance movement.
Unlike standard rollers, these components are engineered with a specific focus on surface smoothness to prevent material adhesion. This is particularly critical in food and pharmaceutical lines where any accumulation of residue could lead to contamination or systemic failure.
Selecting the correct roller requires a deep analysis of the tube wall thickness and shaft diameter. A thicker tube wall increases the roller's resistance to deformation under high-tonnage loads, which is essential for mining or heavy industrial applications where stability prevents belt misalignment.
Bearing configuration is equally vital; the choice between sealed ball bearings and specialized bushings determines the roller's sensitivity to dust and moisture. In underground power plants, an anti-static and low-damping sealing structure is implemented to protect the internal mechanism from conductive particulates, thereby improving overall energy efficiency.
The interaction between the roller surface and the belt material also dictates the overall system tension. Stainless steel's inherent hardness ensures that the roller maintains its cylindrical integrity over millions of rotations, preventing the "flat spotting" common in lower-grade polymer rollers.
The distinction between 304 and 316 stainless steel is often misunderstood by procurement teams, yet it defines the lifespan of the equipment. Grade 304 is the industrial baseline, providing excellent resistance to general oxidation and moisture, making it suitable for most food processing and indoor packaging environments.
From a cost-benefit perspective, utilizing 316 in a low-corrosion environment results in unnecessary capital expenditure. Therefore, a site-specific audit of the chemical environment is required before finalizing the material specification for any conveyor belt company project.
When comparing roller materials, the decision matrix typically involves a trade-off between weight, corrosion resistance, and load capacity. While nylon offers lightweight benefits and rubber provides necessary cushioning, they both lack the structural rigidity and chemical immunity of stainless steel.
The following assessment provides a normalized engineering score across five key performance indicators, illustrating why stainless steel is preferred for high-criticality industrial zones.
In practical application, stainless steel rollers are indispensable under conveyor iron removers in power plants. In these zones, the magnetic field of the iron remover would attract standard steel rollers, causing catastrophic mechanical interference. Stainless steel's non-magnetic properties ensure the rollers remain stable while the system effectively removes metallic contaminants from the bulk material.
Furthermore, in pharmaceutical cleanrooms, the smooth metallic luster and non-porous surface of these rollers facilitate rapid sterilization. This eliminates the risk of microbial growth and ensures that the conveyor system adheres to global sanitary standards, reducing the frequency of manual scrubbing and chemical cleaning.
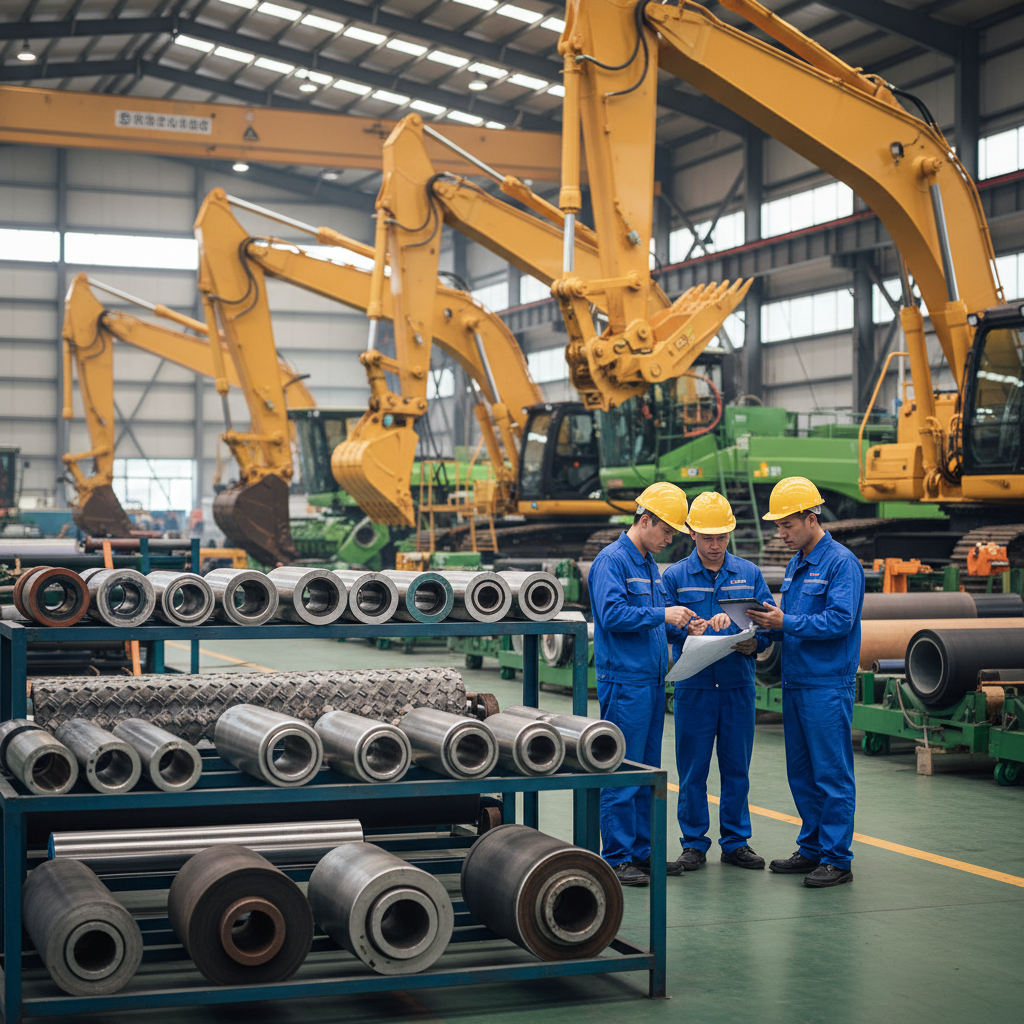
The manufacturing workflow begins with the precise selection of raw stainless steel tubes, which are then processed to exact dimensional tolerances. Any deviation in the tube's circularity can cause belt tracking issues, leading to premature belt edge wear and increased friction.
Crucial to the roller's longevity is the integration of the sealing structure. A high-performance seal prevents the ingress of moisture and acidic particulates into the bearing housing. When seals fail, the lubricant is contaminated, leading to increased rotational resistance and eventual bearing seizure.
Final quality control involves a series of rotation tests and dimensional audits. For a professional conveyor belt company, ensuring that the shaft-end configuration perfectly matches the existing bracketry is the difference between a seamless installation and an operational bottleneck.
Selecting the right roller requires balancing the operating environment with the required load capacity. Using a high-duty configuration in a light-load application is an inefficient use of resources, while under-specifying rollers in a chemical plant leads to rapid corrosion.
The following matrix provides an evaluation framework for matching roller configurations to specific industrial deployment scenarios based on common engineering requirements.
Buyers should evaluate the total cost of ownership, considering that while stainless steel has a higher initial procurement cost, its extended service life significantly reduces the frequency of replacement cycles.
| Configuration Type | Material Specification | Environmental Resistance | Recommended Use Case |
|---|---|---|---|
| Basic Profile | SS 304 / Standard Wall | Moderate Humidity | General Packaging |
| Standard Profile | SS 304 / Reinforced Wall | Moisture / Dust | Food Processing |
| High-Duty Profile | SS 316 / Heavy Wall | Strong Acid / Alkali | Chemical Production |
| Precision Profile | SS 316 / Tight Tolerance | Sterile / High-Washdown | Pharmaceuticals |
| Mining Profile | SS 304 / Impact-Resistant | High Abrasion / Wet | Underground Coal |
| Marine Profile | SS 316 / High Moly | Chloride / Salt Spray | Port Terminals |
The primary advantage is the superior load-bearing capacity and corrosion resistance. While nylon is lightweight and resists some chemicals, it can deform under heavy continuous loads and is susceptible to degradation from UV exposure or high temperatures. Stainless steel provides structural rigidity and total immunity to rust in humid environments, ensuring the conveyor belt remains properly supported without sagging.
The sealing structure acts as the first line of defense for the internal bearings. In industrial settings, dust and moisture can penetrate the bearing housing, displacing lubricant and causing friction-induced heat. A high-quality, low-damping seal prevents this contamination, maintaining low rotational resistance and extending the mean time between failures (MTBF) of the component.
You should specify Grade 316 when the conveyor is exposed to chlorides, salt water, or highly aggressive acids. 304 is sufficient for general food-grade and moisture-rich environments, but it will pit and corrode in marine or heavy chemical processing zones. 316's molybdenum content provides the necessary chemical stability to prevent surface perforation in these extreme conditions.
Yes, professional manufacturers can customize the face length, tube thickness, and shaft-end configuration. Customization is essential when replacing rollers in legacy systems where standard sizes may cause belt mistracking. Providing accurate drawings or samples ensures the new rollers fit the existing bracketry without requiring modifications to the conveyor frame.
Key indicators include abnormal noise during rotation, visible surface pitting, or a noticeable increase in belt friction. If the roller no longer rotates freely, it may be due to bearing failure or seal breach. Regular inspections should check for shaft misalignment and surface wear, as a seized roller can quickly damage the conveyor belt, leading to expensive belt replacement.
Price is primarily driven by the material grade (316 vs 304), the wall thickness of the tube, the precision of the machining, and the type of bearings used. Order quantity also affects unit cost due to production setup time. Buyers should evaluate the total value, as higher-quality materials and seals reduce the frequency of replacement, lowering the overall operational expenditure.
The transition toward stainless steel conveyor components is a response to the increasing demands for hygiene and durability in modern industrial processing. By aligning material grades (304 vs 316) with specific environmental hazards and ensuring high-integrity sealing, companies can significantly stabilize their production throughput.
Ultimately, the decision to partner with a technically capable conveyor belt company depends on their ability to provide customized, specification-driven solutions rather than generic products. Investing in precision-engineered rollers is the most effective strategy for mitigating the risks of corrosion and mechanical failure in critical material handling systems.