- Tel: +8615128135888
- Email: hg@chinaconveyerbelt.com

Flame Retardant Whole Core Conveyor Belt China Factory and Suppliers

The Whole Core Flame-Retardant Conveyor Belt is a high-performance industrial solution specifically engineered for hazardous environments where fire safety is paramount. Designed primarily for underground coal mine transportation, as well as metallurgical and chemical industries, these belts utilize an advanced impregnation and vulcanization process. By treating the entire belt core with a specialized polyvinyl chloride (PVC) paste, Roule ensures a product that combines high tensile strength and large capacity with critical safety features, including anti-static, impact-resistant, and corrosion-resistant properties.
Available in both PVC and PVG types, these belts are optimized for different operational inclinations and durability requirements. Whether navigating the strict safety regulations of a power plant or the abrasive conditions of a steel mill, our whole-core structure prevents delamination and suppresses flame propagation. By integrating flame-retardant agents directly into the rubber compound, the belt self-extinguishes once the heat source is removed, ensuring operational stability and protecting personnel in the world's most challenging work environments.
Detailed Parameters
| Core Type | Whole Core Flame-Retardant | PVC Type Cover | Adhesive ≥ 0.8mm (Single-sided) |
|---|---|---|---|
| PVG Type Cover | Nitrile Rubber + PVC (1.5mm-4.5mm) | Max Inclination (PVC) | Less than 16° |
| Max Inclination (PVG) | Less than 20° | Key Properties | Flame Retardant, Anti-static, Wear-resistant |
| Production Process | Vulcanization & Plasticizing | Carcass Structure | High-tensile Synthetic Fiber |
| Application Areas | Mining, Metallurgy, Chemical | Safety Certification | International Fire Resistance Standards |
Key Advantages
Superior Fire Safety
Engineered to delay combustion and self-extinguish quickly, preventing the spread of fire in high-risk zones.
Extended Service Life
Integrated whole-core design eliminates layered separation, reducing maintenance and replacement frequency.
High Tensile Strength
Withstands heavy loads without deformation, ensuring stable transportation in large-scale industrial operations.
Anti-Static Surface
Specially formulated to dissipate static electricity, minimizing the risk of ignition from electrical discharge.
Customizable Specs
Adjustable cover thickness and surface textures to meet specific metallurgical or mining application needs.
Strict Quality Control
Every belt undergoes drum friction and flame propagation tests in our 6,000sqm facility.
Product Gallery


Management Platforms
Material Handling
Optimized for bulk material transport in coal mines and chemical plants.
Process Optimization
Advanced vulcanization processes ensure uniform bonding and high adhesion.
Safety Compliance
Meets international standards for fire resistance and anti-static performance.
Maintenance Alerts
Reduced wear and tear lead to longer operational intervals between checks.
Inventory Control
Standardized sizing for easy replacement and stock management.
Energy Efficiency
Low-resistance surfaces reduce strain on conveyor motors and power costs.
Investment Return Comparison
| Metric | Ordinary Conveyor Belt | Roule Flame-Retardant Belt |
|---|---|---|
| Fire Risk | High (Combustible) | Low (Self-extinguishing) |
| Service Life | Standard | Extended (Whole-core design) |
| Maintenance Cost | Frequent Replacements | Low (Reduced delamination) |
| Safety Compliance | Basic | Full International Standards |
| Operational Downtime | Higher risk of failure | Minimized through durability |
Frequently Asked Questions
PVC belts feature a PVC cover adhesive (≥0.8mm) and are suitable for inclinations below 16°. PVG belts use a blend of Nitrile rubber and PVC (1.5mm-4.5mm), allowing for steeper inclinations up to 20°.
The whole-core structure eliminates traditional layers, preventing delamination and ensuring that flame-retardant agents are integrated throughout the belt, not just on the surface.
Yes, our belts are designed with corrosion-resistant and flame-retardant properties, making them ideal for chemical and metallurgical material transportation.
We incorporate specialized anti-static additives into the rubber compound to dissipate electricity generated by friction, preventing sparks in combustible environments.
All belts undergo rigorous testing, including flame propagation, drum friction, and tensile strength assessments within our modern 6,000-square-meter production facility.
On the contrary, the integrated core structure reduces the likelihood of layer separation and wear, leading to lower maintenance costs and fewer replacements over time.
Ready to Enhance Your Industrial Safety and Efficiency?
Contact Us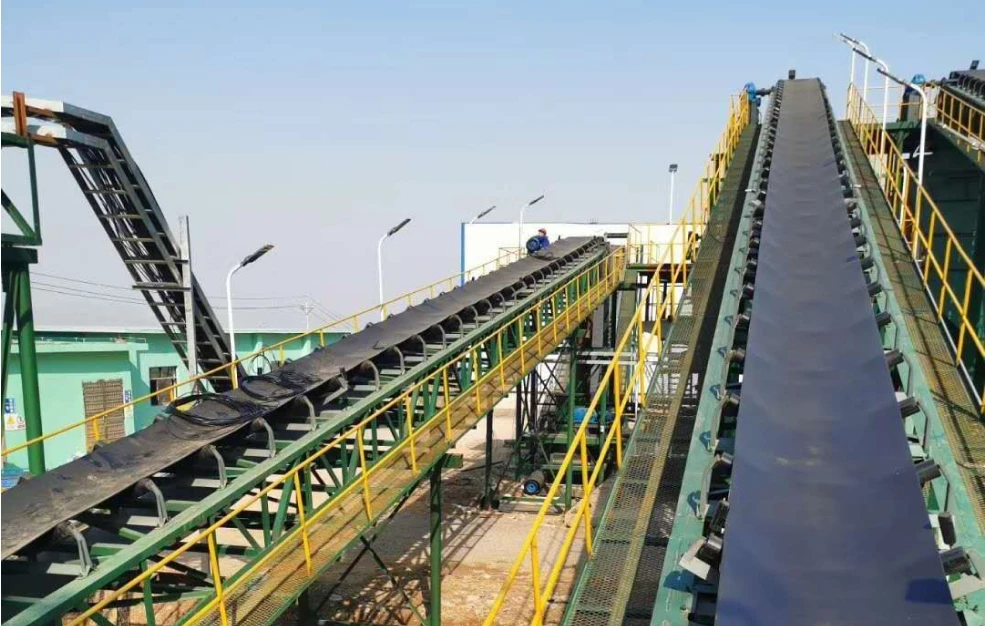
Global Reach of Our High-Quality Conveyor Solutions
Global Reach of Our High-Quality Conveyor SolutionsOur conveyor products, including rollers, belts, drums, and accessories, have been successfully exported to numerous countries across industries like mining, ports, metallurgy, coal, and chemicals. With certifications like ISO, CE, and SGS, our reliable and efficient solutions meet international standards, earning trust from clients worldwide.
-
 Explosion Proof Conveyor Drum Factory Leading China Suppliers of Industrial Drive DrumsHigh-performance explosion proof external electric drums from a leading China factory. Our certified suppliers provide secure, durable drive solutions for mining and petrochemical industries.
-
 Custom Stainless Steel Conveyor Rollers Factory Leading China SuppliersLooking for premium stainless steel conveyor rollers? As leading China suppliers and a professional factory, we provide customizable, corrosion-resistant rollers for food, pharma, and mining industries to ensure maximum efficiency.
-
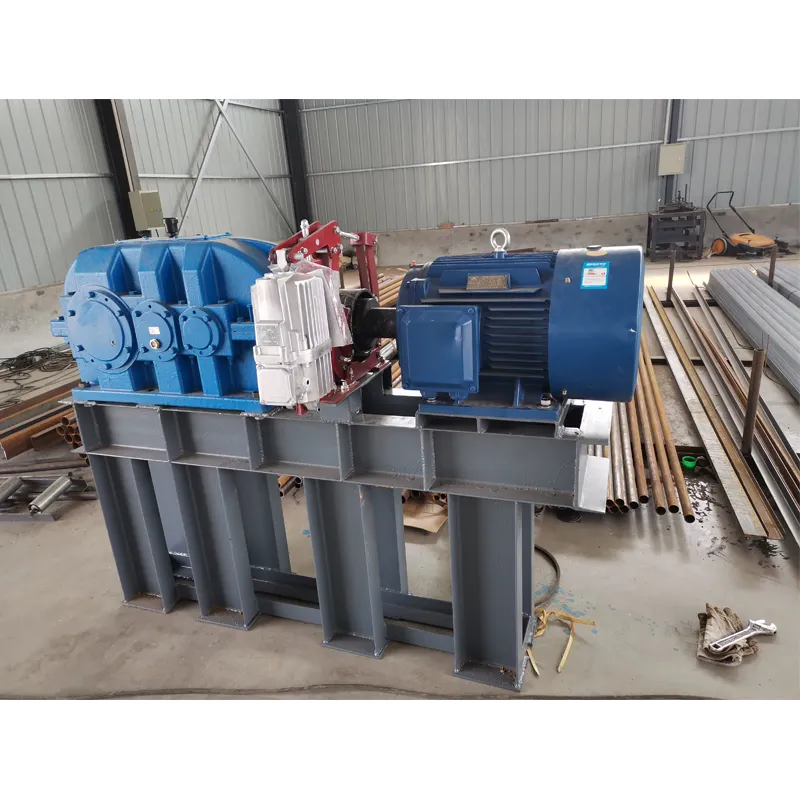 Industrial Belt Conveyor Drive Motor Reducer China Factory SuppliersHigh-performance belt conveyor drive systems consisting of motors and reducers. Leading China factory suppliers providing energy-efficient and durable transmission solutions for mining and logistics.
-
 Groove Type Friction Selfaligning Roller China Factory and SuppliersHigh-precision groove type friction self-aligning rollers from a leading China factory. Our professional suppliers provide automatic belt centering solutions to prevent deviation and reduce maintenance for fixed belt conveyors.
-
 Premium Head Polyurethane Belt Conveyor Cleaner China Factory SuppliersLooking for reliable China suppliers? Our factory provides high-performance head polyurethane cleaners. The unique formulation resists wear and deformation, delivering consistent cleaning performance in cement, coal and bulk handling operations.
-
 HighPerformance Ceramic Conveyor Drum China Factory and SuppliersLooking for durable ceramic rubber pulleys for belt conveyors? As leading China suppliers and a professional factory, we provide high-wear resistance ceramic conveyor drums designed to prevent slippage and extend equipment lifespan.
-
 Industrial Permanent Magnet Iron Remover Factory Leading China SuppliersHebei Roules is a leading China factory and suppliers of high-performance permanent magnet iron removers. Utilizing advanced neodymium magnets, our systems ensure material purity and equipment protection with zero energy consumption for heavy industries.
-
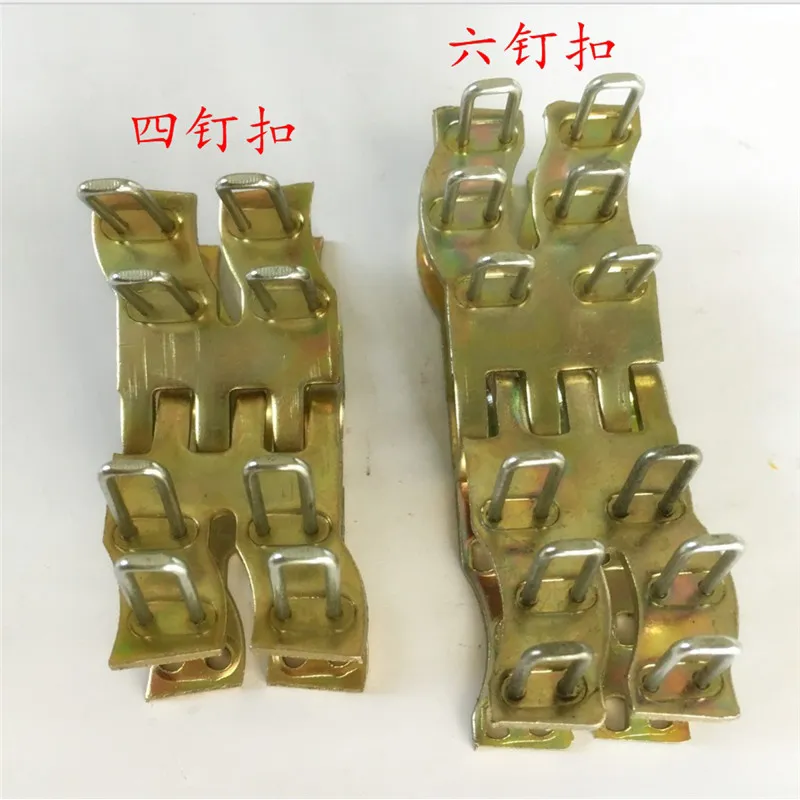 Heavy Duty Six Nail Buckle Conveyor Fasteners China Factory SuppliersLooking for reliable conveyor belt connecting buckles? Our China factory provides high-strength Six Nail Buckles for mining and logistics. As leading suppliers, we ensure superior stability and rapid installation for industrial conveyor systems.
Let's Get in Touch!
Send us a message and let our experts assist you with tailored solutions.


