- Tel: +8615128135888
- Email: hg@chinaconveyerbelt.com

Builtin Electric Conveyor Drum Manufacturers China Factory Suppliers
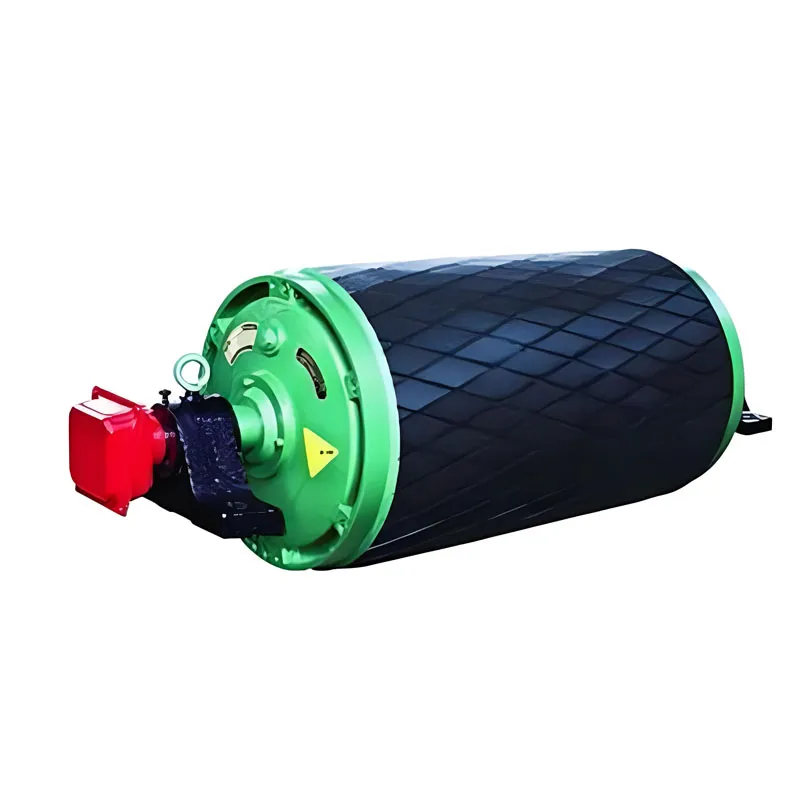
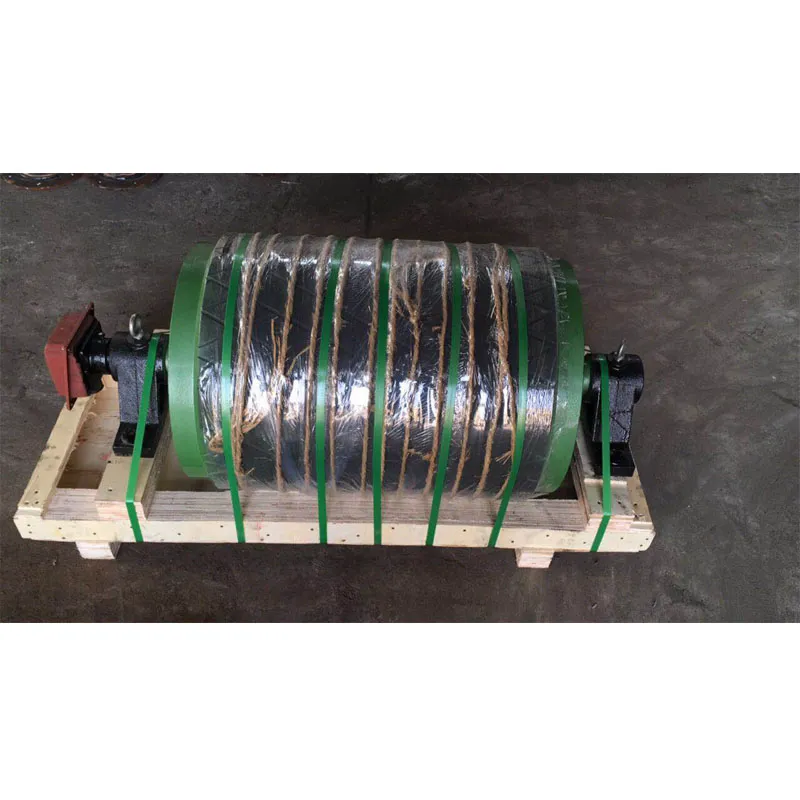
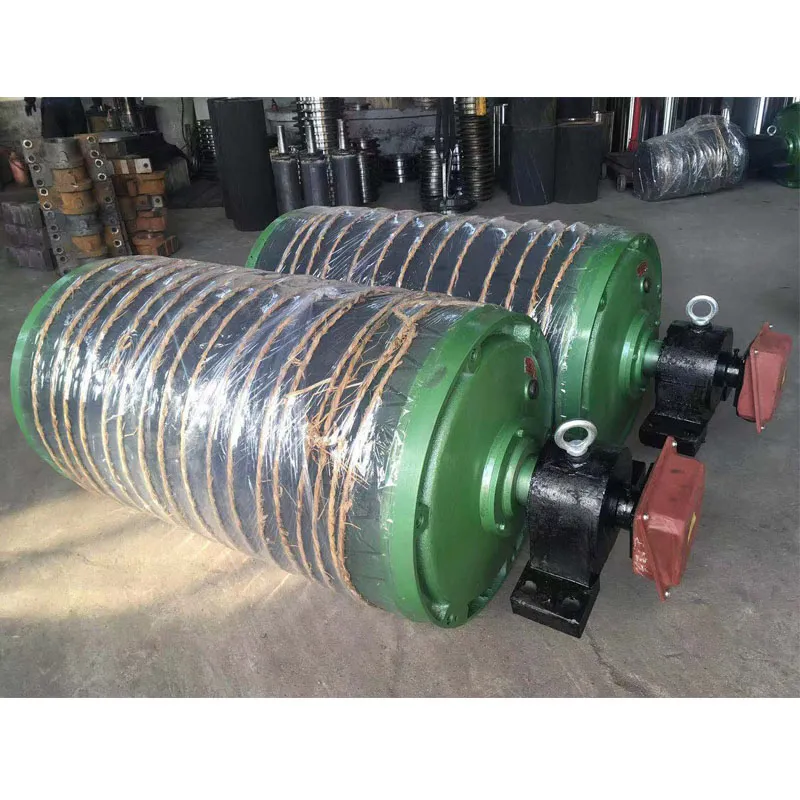
The Built-in Electric Conveyor Drum is a high-performance integrated power solution designed to replace traditional external motor-reducer drive systems. By combining the motor and the drum into a single, compact unit, it delivers exceptional transmission efficiency and smooth operational stability, making it an ideal choice for modern belt conveyors and lifting equipment.
Engineered for resilience, this electric drum is specifically built to withstand harsh industrial environments. Its superior sealing capabilities ensure reliable performance in areas with high dust concentrations, moisture, or muddy conditions, providing a streamlined installation process and significantly reducing the overall spatial footprint of your material handling system.
Detailed Parameters
| Operating Temperature | 15 ℃ to 40 ℃ | Max Altitude | 1000 Meters |
|---|---|---|---|
| Max Material Temp | 60 ℃ | Operating Voltage | 380V |
| Rated Frequency | 50Hz | Drive Type | Internal Electric Motor |
| Sealing Level | High-Grade Industrial Seal | Application | Bulk Material Transport |
| Control Options | Reverse, Braking, Centralized | Surface Finish | Rubber Wrapping Compatible |
Key Advantages
Superior Sealing
Engineered for extreme durability in damp, muddy, and high-dust environments, ensuring internal components remain protected.
Extended Lifespan
Low-friction operation and high-quality components result in a long service life and reduced maintenance intervals.
Compact Design
Eliminates the need for external reducers, drastically reducing the installation space and simplifying the system layout.
High Efficiency
Optimized power transmission minimizes energy loss and provides smooth, reliable torque for heavy-duty loads.
Easy Installation
The integrated structure allows for rapid deployment and straightforward integration into existing conveyor lines.
Versatile Control
Fully compatible with centralized control systems, supporting braking, reversing, and variable speed requirements.
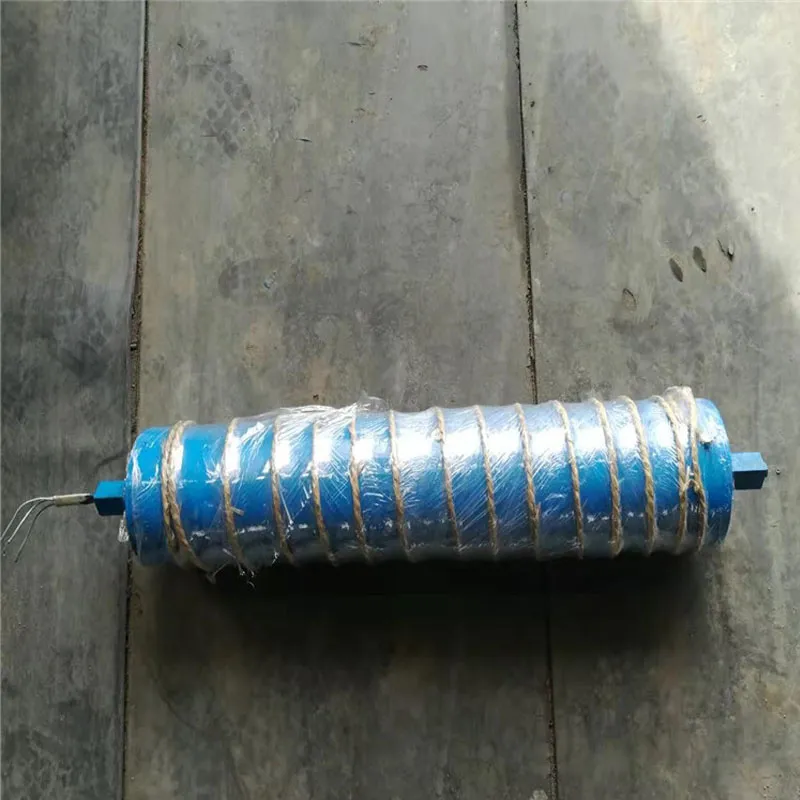
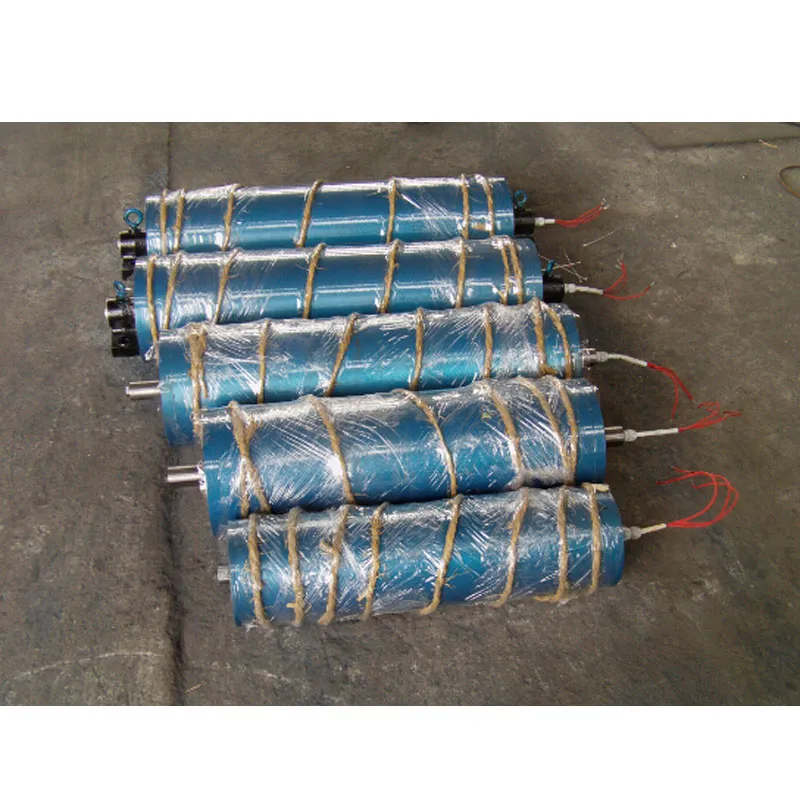
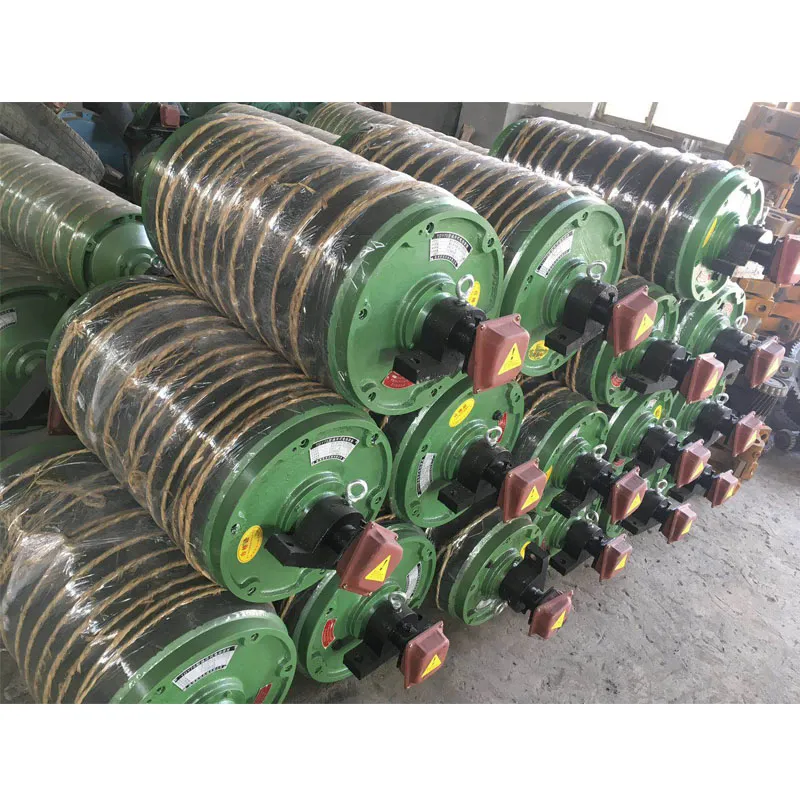
Product Gallery
Management Platforms
Material Logistics
Efficiently transport coal, ore, sand, and cement with optimized bulk handling capabilities.
Power Integration
Seamless replacement of motor-reducer drives for a more streamlined power source.
Noise Reduction
Engineered for low-noise operation to improve workplace safety and environment.
Energy Optimization
Reduced energy consumption through direct-drive efficiency and minimized friction.
Industrial Adaptability
Perfect for mining, metallurgy, chemical, and grain transportation sectors.
Maintenance Ease
Simplified structural design ensures fast troubleshooting and low-cost upkeep.
Investment Return Comparison
| Feature Metric | External Drive System | Built-in Electric Drum |
|---|---|---|
| Installation Space | Large (Motor + Reducer) | Ultra-Compact |
| Energy Efficiency | Medium (Transmission Loss) | High (Direct Drive) |
| Environmental Seal | Standard/Variable | Industrial Grade (High) |
| Maintenance Frequency | High (Couplings/Gears) | Low (Integrated Unit) |
| Noise Level | Moderate to High | Low/Smooth |
Frequently Asked Questions
The built-in electric drum offers a more compact structure, higher transmission efficiency, lower noise, and superior sealing, making it far more suitable for harsh industrial environments than traditional external drives.
It is widely used in mining, metallurgy, chemical industries, coal processing, building material production, electricity generation, grain handling, and general transportation.
Yes, the equipment is designed to handle conveyed materials with temperatures up to 60 ℃, provided the operating environment remains within the specified range of 15 ℃ to 40 ℃.
Absolutely. The built-in electric drum is designed to meet various operational needs, including reverse movement, braking, and rubber wrapping for enhanced grip.
Thanks to its professional-grade sealing, the electric drum is specifically engineered to operate reliably in workplaces with high dust concentrations and damp or muddy environments.
The standard operational requirement is a voltage of 380V and a frequency of 50Hz, ensuring compatibility with most industrial power grids.
Ready to Optimize Your Material Handling Efficiency?
Contact Us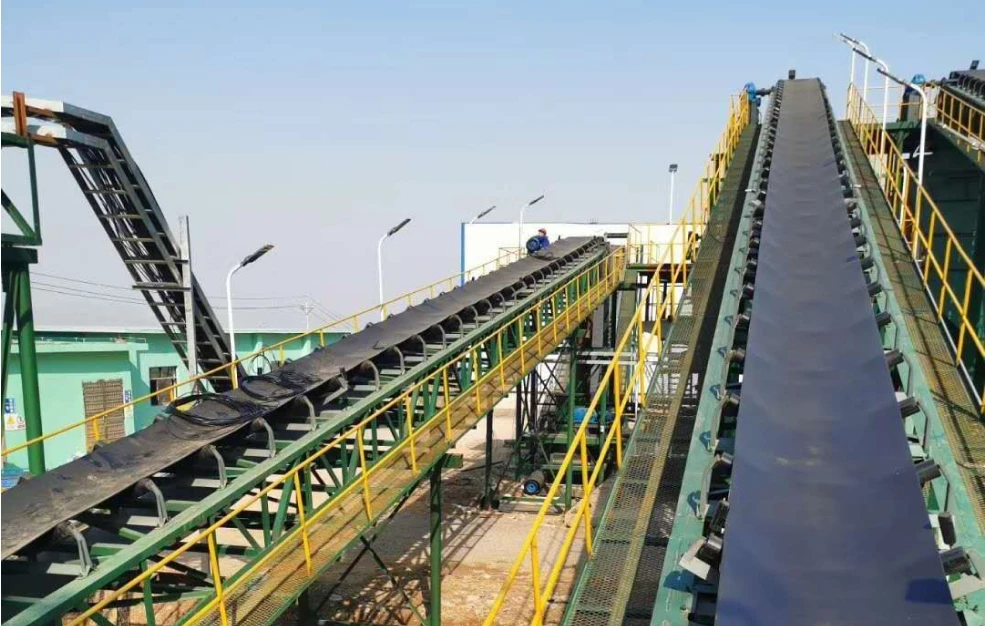
Global Reach of Our High-Quality Conveyor Solutions
Global Reach of Our High-Quality Conveyor SolutionsOur conveyor products, including rollers, belts, drums, and accessories, have been successfully exported to numerous countries across industries like mining, ports, metallurgy, coal, and chemicals. With certifications like ISO, CE, and SGS, our reliable and efficient solutions meet international standards, earning trust from clients worldwide.
-
 Heat Resistant Conveyor Belt China Factory and Leading SuppliersHigh-performance heat resistant conveyor belts from a leading China factory. Specialized suppliers providing durable solutions for transporting sintered ore and coke in metallurgy and construction.
-
 Mining Conveyor Roller Bracket China Factory and Trusted SuppliersLooking for high-quality mining conveyor roller brackets? As leading China suppliers and a professional factory, we provide durable, self-aligning and buffer brackets to optimize conveyor frame stability and reduce operational costs.
-
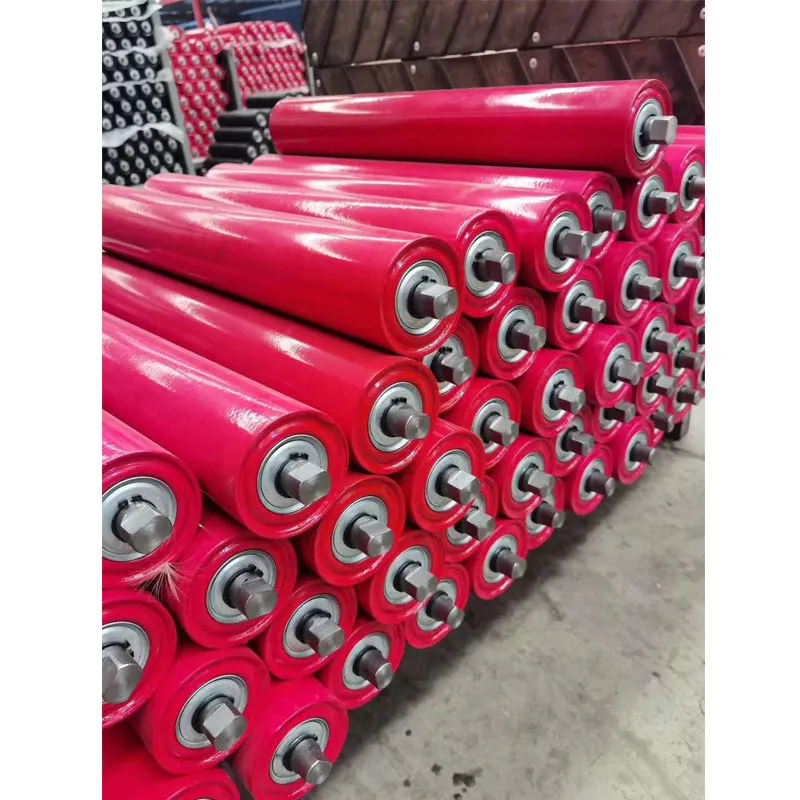 Parallel Return Rollers Manufacturer High Quality China Factory SuppliersLooking for reliable Parallel Return Rollers? As leading China factory suppliers, we provide high-performance rollers to support unloaded conveyor belts, ensuring smooth circulation and reducing maintenance costs for industrial operations.
-
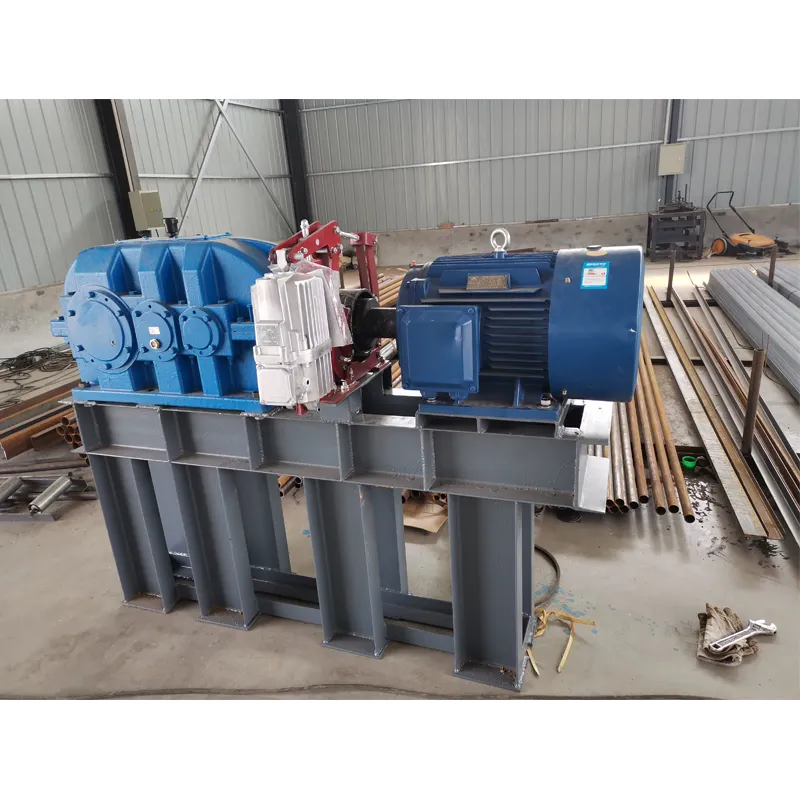 Industrial Belt Conveyor Drive Motor Reducer China Factory SuppliersHigh-performance belt conveyor drive systems consisting of motors and reducers. Leading China factory suppliers providing energy-efficient and durable transmission solutions for mining and logistics.
-
 HighStrength Stainless Steel Mining Roller Brackets China Factory SuppliersLooking for reliable conveyor supports? Our China factory provides high-strength stainless steel mining roller brackets engineered for corrosion resistance and heavy loads. As leading suppliers, we ensure maximum durability in harsh industrial environments to reduce your maintenance costs.
-
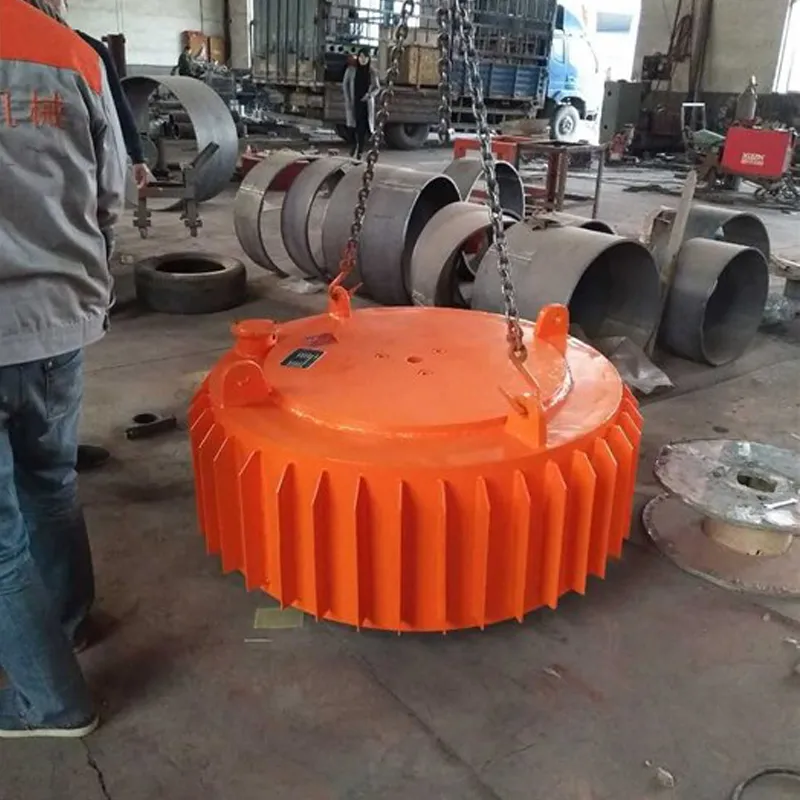 Industrial Electromagnetic Iron Remover China Factory and Leading SuppliersHebei Roule is a premier China factory and suppliers of electromagnetic iron removers. Our systems feature a quick-release cleaning mechanism that minimizes operational interruptions while maintaining maximum equipment protection.
-
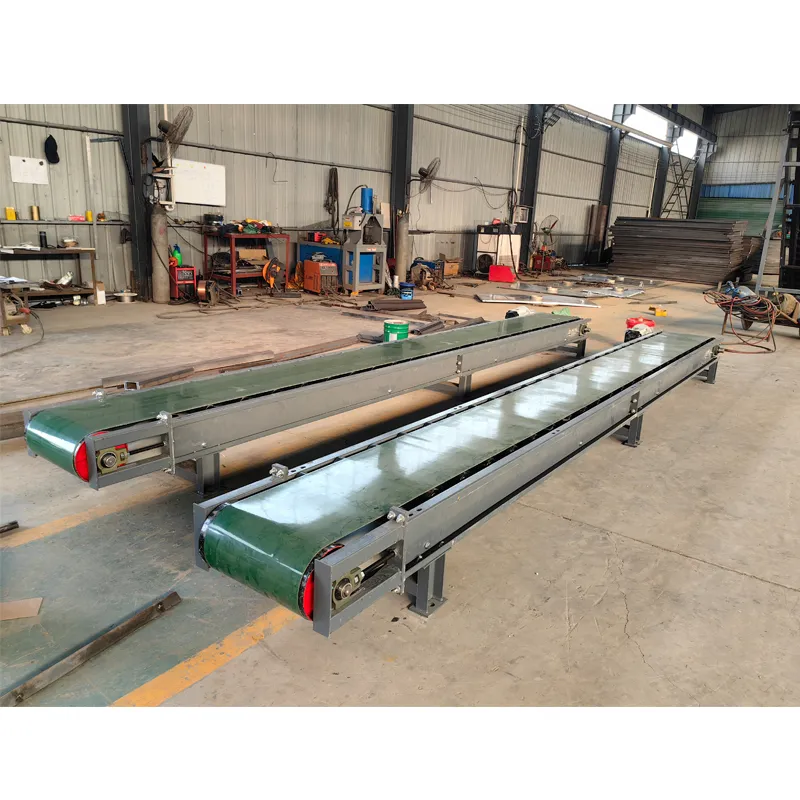 HighPerformance Parallel Conveyor Factory and Suppliers in ChinaLooking for reliable Parallel Conveyor suppliers in China? Our factory provides high-efficiency flat belt conveyors driven by motor drums for smooth material transport and minimal waste.
-
 HighPerformance Transmission Conveyor Reversing Drum China Factory SuppliersLooking for reliable reversing pulleys? Our China factory provides high-strength transmission conveyor drums for mining, metallurgy, and ports. As leading suppliers, we offer durable driving devices for various belt conveyors to ensure seamless material handling.
Let's Get in Touch!
Send us a message and let our experts assist you with tailored solutions.


