- Tel: +8615128135888
- Email: hg@chinaconveyerbelt.com

Explosion Proof Conveyor Drum Factory Leading China Suppliers of Industrial Drive Drums

The Explosion Proof Conveyor Drum is a high-performance industrial drive solution specifically engineered for hazardous environments. By integrating a precision-engineered drum with an external explosion-proof motor and reducer, this equipment ensures the seamless transportation of materials in areas where flammable gases or combustible dust are present, providing a critical layer of safety for large-scale material handling systems.
Designed to meet rigorous international safety standards, our explosion-proof drums are widely deployed across the mining, petrochemical, and energy sectors. The system utilizes an advanced sealing structure that prevents internal electrical sparks or heat from igniting the external atmosphere, ensuring continuous operational stability and maximum safety in high-risk industrial zones.
Detailed Parameters
| Explosion Proof Grade | dI, dIIAT4, dIIBT4 | Core Components | Drum, External Motor, Reducer |
|---|---|---|---|
| Application Zone | Methane/Coal Dust Hazardous Areas | Hazardous Mixtures | Class I, II Class A/B (T1-T4) |
| Drive Mechanism | External Electric Drive | Safety Features | Encapsulation & Backstop options |
| Primary Material | High-Strength Industrial Steel | Operational Role | Material Conveying & Driving |
| Industry Standards | Mining & Petrochemical Compliance | Cooling Method | Natural/Forced Air Cooling |
Key Advantages
Certified Safety
Compliant with dI, dIIAT4, and dIIBT4 standards to prevent explosions in hazardous environments.
Operational Stability
Precise design ensures consistent torque and rotation for efficient material transport.
Integrated Design
Seamlessly combines transmission, driving, and explosion-proofing in one compact unit.
Advanced Isolation
Prevents internal sparks and high temperatures from reaching the external environment.
Versatile Application
Ideal for coal mines, oil refineries, chemical plants, and other volatile workplaces.
Custom Configurations
Available with backstop and specialized encapsulation to meet specific project needs.
Product Gallery

Management Platforms
Logistics Control
Optimized material flow management for continuous conveyor systems.
Drive Monitoring
Real-time tracking of motor performance and reducer efficiency.
Safety Alerts
Instant notifications for temperature spikes or electrical anomalies.
Compliance Audit
Automatic logging of safety checks to ensure ATEX/explosion-proof compliance.
Asset Lifecycle
Predictive maintenance scheduling for drums and rollers to reduce downtime.
Energy Optimization
Adjustable drive parameters to reduce power consumption during low loads.
Investment Return Comparison
| Metric | Standard Conveyor Drum | Explosion Proof Drum |
|---|---|---|
| Safety Risk | High (in hazardous zones) | Ultra-Low (Certified) |
| Maintenance Cycle | Frequent (Manual Checks) | Extended (Robust Build) |
| Regulatory Compliance | Non-Compliant | Full Industrial Compliance |
| Operational Downtime | High Risk of Accident Stop | Planned Preventive Care |
| Long-term ROI | Low (due to Risk Cost) | High (Safe & Stable) |
Frequently Asked Questions
The dIIBT4 rating indicates that the equipment is suitable for environments containing Class I, IIA, and IIB explosive gas mixtures with a temperature class of T1-T4, ensuring the surface temperature remains below the ignition point.
It is achieved through a precise explosion-proof structure and encapsulation. The external motor and reducer are sealed to prevent any internal sparks or heat from escaping into the surrounding flammable atmosphere.
Yes, specifically the dI rated drums are designed for mines containing methane or coal dust explosion hazardous mixtures, making them ideal for safe coal transportation.
A backstop is a mechanical safety device that prevents the conveyor belt from sliding backward under the weight of the material when the motor stops, which is crucial for inclined conveyor systems.
It is widely used in the petrochemical industry to drive essential equipment like pumps and compressors, ensuring smooth production in explosive environments.
The external motor design allows for easier access to electrical components for inspections and repairs without needing to dismantle the entire drum assembly, reducing downtime.
Ready to Secure Your Material Handling System?
Contact Us
Global Reach of Our High-Quality Conveyor Solutions
Global Reach of Our High-Quality Conveyor SolutionsOur conveyor products, including rollers, belts, drums, and accessories, have been successfully exported to numerous countries across industries like mining, ports, metallurgy, coal, and chemicals. With certifications like ISO, CE, and SGS, our reliable and efficient solutions meet international standards, earning trust from clients worldwide.
-
 High Performance Casting Rubber Rollers China Factory and SuppliersHigh performance buffer roller groups from a leading China factory. Our casting rubber rollers reduce material impact at receiving sections to extend conveyor belt life. Contact top China suppliers for durable, low-friction solutions.
-
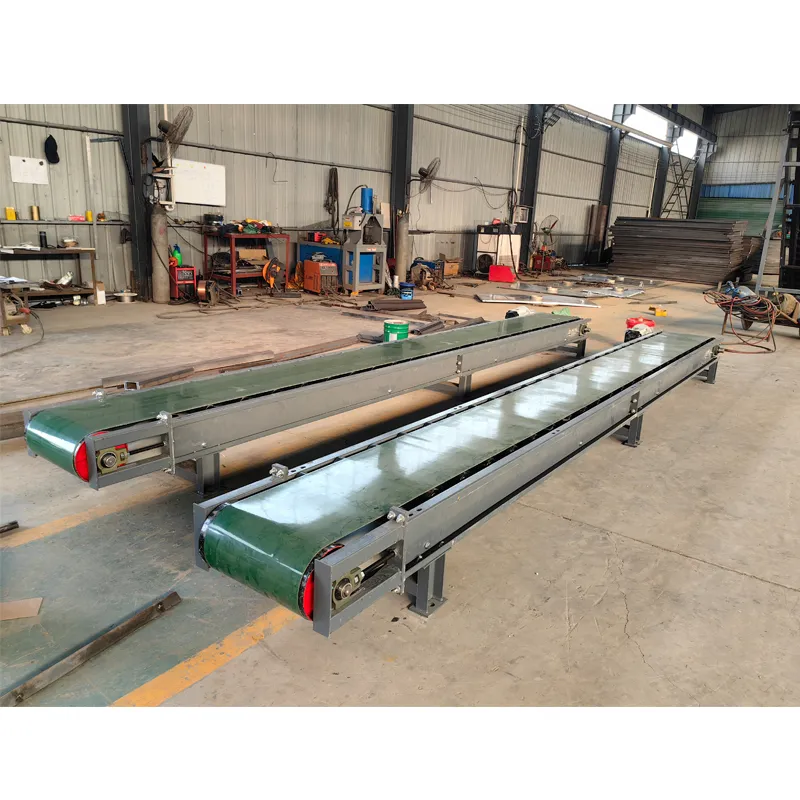 HighPerformance Parallel Conveyor Factory and Suppliers in ChinaLooking for reliable Parallel Conveyor suppliers in China? Our factory provides high-efficiency flat belt conveyors driven by motor drums for smooth material transport and minimal waste.
-
 HighStrength Stainless Steel Mining Roller Brackets China Factory SuppliersLooking for reliable conveyor supports? Our China factory provides high-strength stainless steel mining roller brackets engineered for corrosion resistance and heavy loads. As leading suppliers, we ensure maximum durability in harsh industrial environments to reduce your maintenance costs.
-
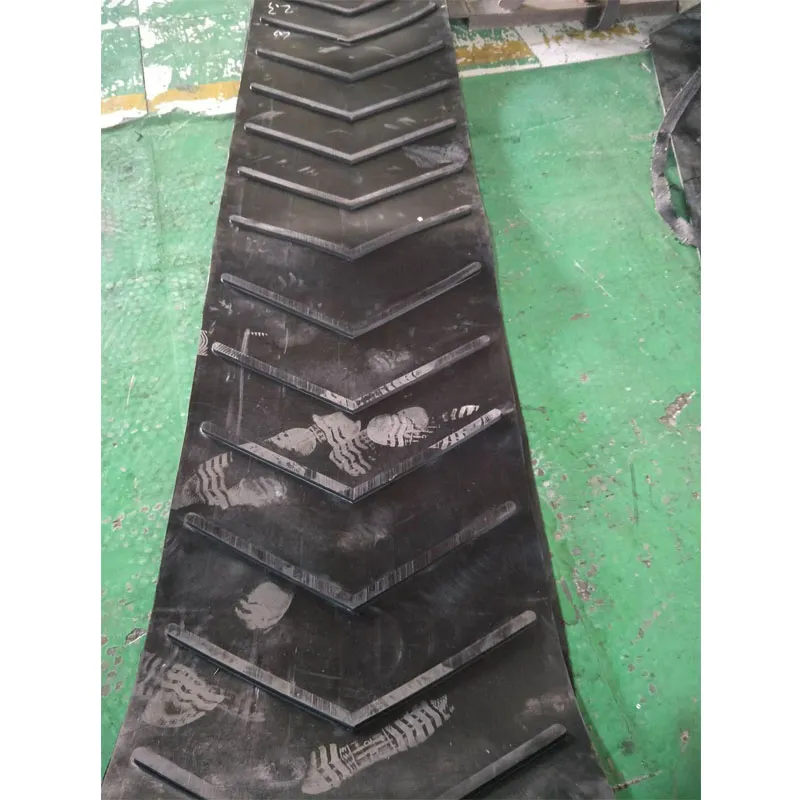 Convex Pattern Conveyor Belt China Factory and Leading SuppliersHigh-performance convex pattern conveyor belts from a leading China factory. Specialized inclined transport solutions from trusted suppliers to prevent material slippage up to 40 degrees.
-
 High Precision Climbing Light Conveyor Factory and Suppliers in ChinaLooking for reliable China suppliers? Our factory provides high-precision climbing light conveyors for chemical, electronics, and food processing industries, offering a stable and energy-efficient alternative to fixed belt conveyors.
-
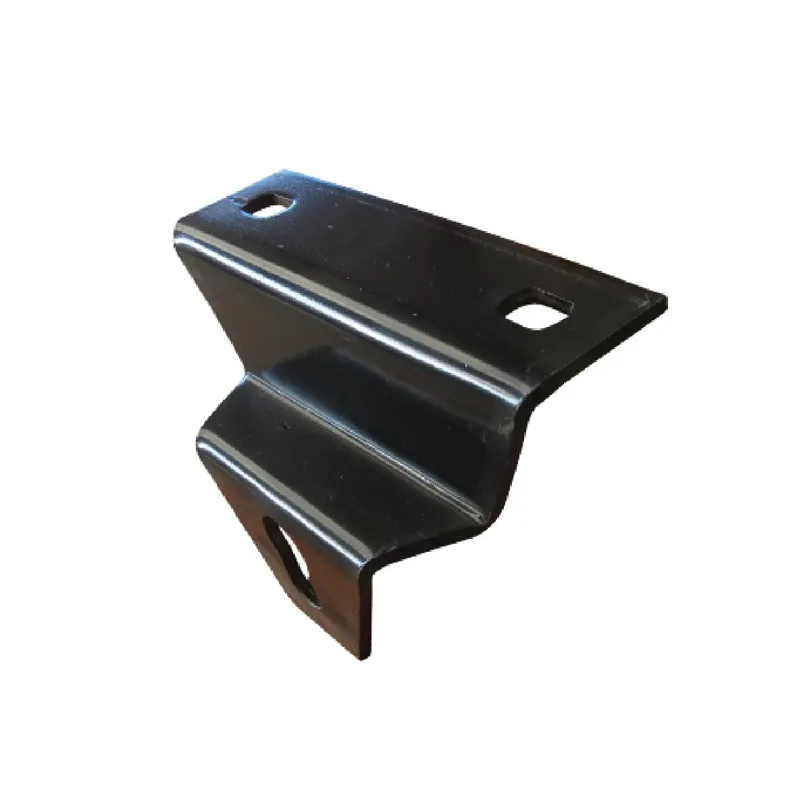 Industrial Conveyor Lower Roller Bracket China Factory and SuppliersPrevent belt deviation and sagging with high-quality conveyor lower roller brackets from our China factory. As leading suppliers, we offer durable return supports to ensure stability and efficiency.
-
 Industrial Belt Filter Conveyor Belt China Suppliers and FactoryHigh-performance belt filter conveyor belts from a leading China factory. Our suppliers provide eco-friendly, corrosion-resistant solutions to optimize filtration efficiency and simplify maintenance.
-
 HighEfficiency Large Angle Corrugated Edge Conveyor Factory and Suppliers in ChinaLooking for reliable China suppliers? Our factory provides high-performance large angle corrugated edge conveyors, also known as wave type edge conveyors, ideal for vertical transport in mining, metallurgy, chemical, and cement industries.
Let's Get in Touch!
Send us a message and let our experts assist you with tailored solutions.


