- Tel: +8615128135888
- Email: hg@chinaconveyerbelt.com

Industrial Mining Conveyor Systems China Suppliers and Factory

Our industrial-grade Mining Conveyor systems are engineered for high-capacity, heavy-duty material handling, specifically optimized for the rigorous demands of coal mines, metallurgy, chemical engineering, power plants, and port logistics. By integrating advanced continuous transport technology, these systems ensure the seamless movement of bulk materials with exceptional efficiency and reliability.
Designed to handle a wide array of materials—including coal, gravel, sand, cement, and fertilizers—our conveyors excel in transporting powder, granular, and small-piece materials with a bulk density under 1.67t/m³. With a focus on durability and environmental adaptability, our equipment is built to maintain peak performance even in the most challenging high-temperature and high-humidity industrial settings.
Detailed Parameters
| Belt Width | B500 - B2500 (Customizable) | Transmission Power | 1.5KW - 800KW |
|---|---|---|---|
| Belt Speeds | 0.8, 1.0, 1.25, 1.6, 2.0, 2.5m/s | Bulk Density Limit | < 1.67 ton/cubic meter |
| Material Suitability | Low abrasive & bagged materials | Transport Distance | Several hundred meters to kilometers |
| Application Fields | Mining, Chemical, Power Plants, Ports | Design Focus | High capacity & High efficiency |
| Environmental Suitability | High Temperature / High Humidity | Cleaning System | Blockage detection & cleaning device |
Key Advantages
Wear Resistant Design
Utilizing premium materials and specialized engineering to resist corrosion and wear, significantly extending the equipment's operational lifespan.
High Volume Transport
Capable of continuous, high-capacity material movement to meet the most demanding industrial throughput requirements.
Stable Operation
A robust and stable structural design ensures reliable material transport without damage, minimizing unplanned downtime.
Dustproof Engineering
Integrated enclosed conveying mechanisms effectively reduce dust scattering, creating a safer and cleaner working environment.
Intelligent Detection
Equipped with advanced blockage detection and cleaning devices to ensure smooth, uninterrupted operation of the belt.
Cost Efficiency
Simplified operation modes lead to lower maintenance costs and reduced labor expenses over the system's lifecycle.
Product Gallery


Management Platforms
Inventory Management
Optimize spare parts like rollers and belts for zero-downtime maintenance.
Operational Control
Precision control of transmission speeds and power output across the line.
Real-time Monitoring
Instant alerts for material blockage or mechanical anomalies via sensors.
Predictive Maintenance
Schedule wear-and-tear checks based on actual running hours and load.
Logistics Coordination
Synchronize belt transport with loading and unloading port schedules.
Energy Optimization
Monitor power consumption to reduce electricity costs during peak loads.
Investment Return Comparison
| Metric | Standard Conveyors | Our Mining Conveyors |
|---|---|---|
| Lifespan | Medium (Standard wear) | Extended (Wear-resistant) |
| Maintenance Cost | Frequent replacements | Reduced (Longer intervals) |
| Operational Efficiency | Moderate Capacity | Ultra-High Capacity |
| Environmental Impact | Higher dust emissions | Low dust (Enclosed design) |
| ROI Period | Longer payback | Faster ROI via efficiency |
Frequently Asked Questions
It is ideal for low abrasive and bagged materials with a bulk density under 1.67t/m³, including coal, sand, gravel, cement, and grains.
Yes, while we offer standard widths from B500 to B2500, other dimensions and speeds (from 0.8 to 2.5m/s) can be fully customized.
Our equipment is equipped with a specialized blockage detection and cleaning device that promptly identifies and removes obstructions to maintain workflow.
Absolutely. We use materials and designs specifically adapted for high-temperature and high-humidity environments to ensure stability in harsh conditions.
Our systems are engineered for long-distance efficiency, capable of transporting materials over several hundred meters or even several kilometers.
We implement a dustproof design using enclosed conveying mechanisms to minimize material scattering and improve the working air quality.
Ready to Optimize Your Material Handling Efficiency?
Contact Us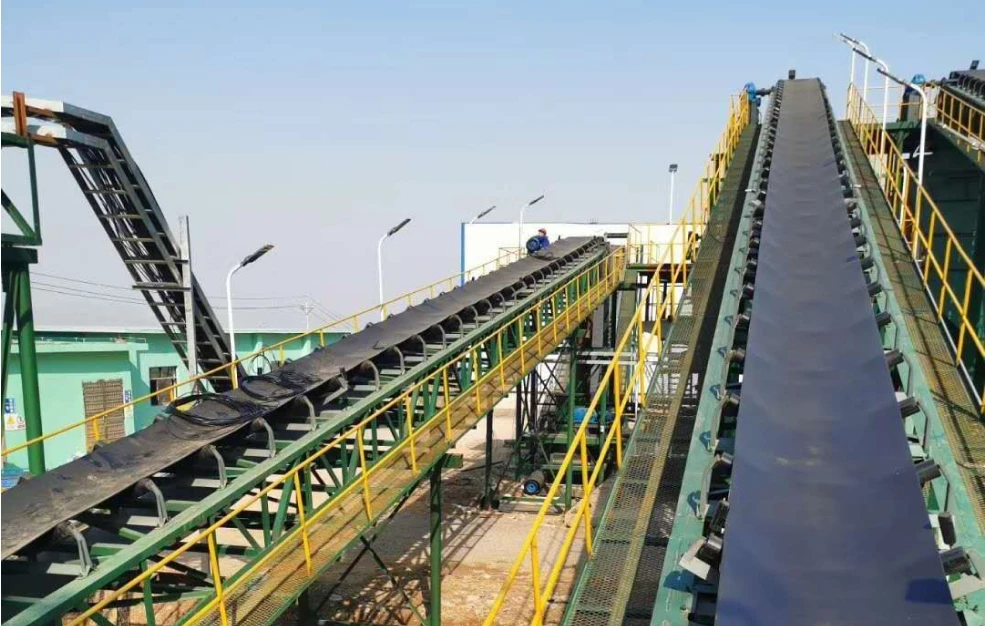
Global Reach of Our High-Quality Conveyor Solutions
Global Reach of Our High-Quality Conveyor SolutionsOur conveyor products, including rollers, belts, drums, and accessories, have been successfully exported to numerous countries across industries like mining, ports, metallurgy, coal, and chemicals. With certifications like ISO, CE, and SGS, our reliable and efficient solutions meet international standards, earning trust from clients worldwide.
-
 UHMWPE Wear Resistant Polymer Rollers China Factory and SuppliersLooking for high-performance polymer rollers? Our China factory provides premium UHMWPE rollers as leading suppliers, offering superior wear resistance, corrosion protection, and low friction for industrial conveyor systems.
-
 Heat Resistant Conveyor Belt China Factory and Leading SuppliersHigh-performance heat resistant conveyor belts from a leading China factory. Specialized suppliers providing durable solutions for transporting sintered ore and coke in metallurgy and construction.
-
 Mining Conveyor Roller Bracket China Factory and Trusted SuppliersLooking for high-quality mining conveyor roller brackets? As leading China suppliers and a professional factory, we provide durable, self-aligning and buffer brackets to optimize conveyor frame stability and reduce operational costs.
-
 Friction SelfAligning Bracket Factory Leading China Suppliers for Belt ConveyorsLooking for a reliable conveyor centering bracket? As a premier China factory and one of the top suppliers, we provide professional friction self-aligning brackets to ensure belt stability and reduce downtime.
-
 Industrial Belt Filter Conveyor Belt China Suppliers and FactoryHigh-performance belt filter conveyor belts from a leading China factory. Our suppliers provide eco-friendly, corrosion-resistant solutions to optimize filtration efficiency and simplify maintenance.
-
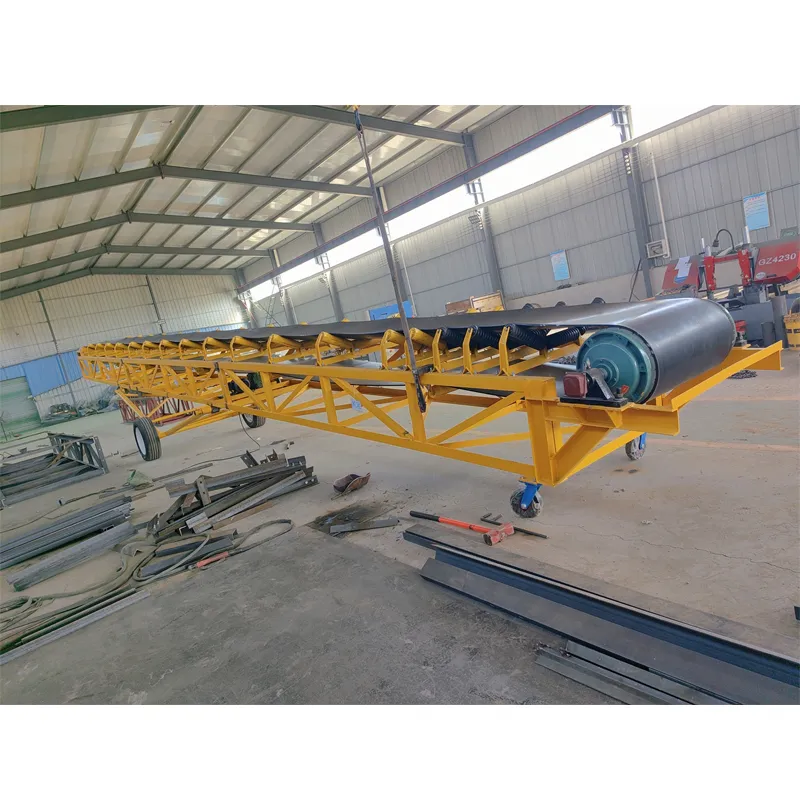 Mobile Lifting Conveyor Factory in China Reliable Loading Unloading SuppliersLooking for high-performance mobile lifting conveyors? As leading China suppliers and a professional factory, we provide flexible, efficient conveying solutions for logistics, mining, and construction to reduce labor costs.
-
 Explosion Proof Conveyor Drum Factory Leading China Suppliers of Industrial Drive DrumsHigh-performance explosion proof external electric drums from a leading China factory. Our certified suppliers provide secure, durable drive solutions for mining and petrochemical industries.
-
 Premium Head Polyurethane Belt Conveyor Cleaner China Factory SuppliersLooking for reliable China suppliers? Our factory provides high-performance head polyurethane cleaners. The unique formulation resists wear and deformation, delivering consistent cleaning performance in cement, coal and bulk handling operations.
Let's Get in Touch!
Send us a message and let our experts assist you with tailored solutions.


