In high-throughput packaging facilities, automated warehousing networks, and multi-level manufacturing plants, optimizing vertical parcel elevation while maintaining package integrity is critical to plant profitability. Procuring a High-Quality Box Elevator Conveyor directly from an advanced Manufacturer in China empowers global OEMs, system integrators, and industrial distributors to secure Advanced, CE Certified vertical transport infrastructure while strictly controlling CapEx and boosting production line yield rates by up to 40%.
Table of Contents: B2B Sourcing Guide
- Structural Engineering & Reinforced Cleat Metallurgy
- Industrial Applications & Multi-Floor Integration
- Wholesale Cost Analysis & ROI
- OEM Customization & Distributor FAQ
Structural Engineering & Reinforced Cleat Metallurgy
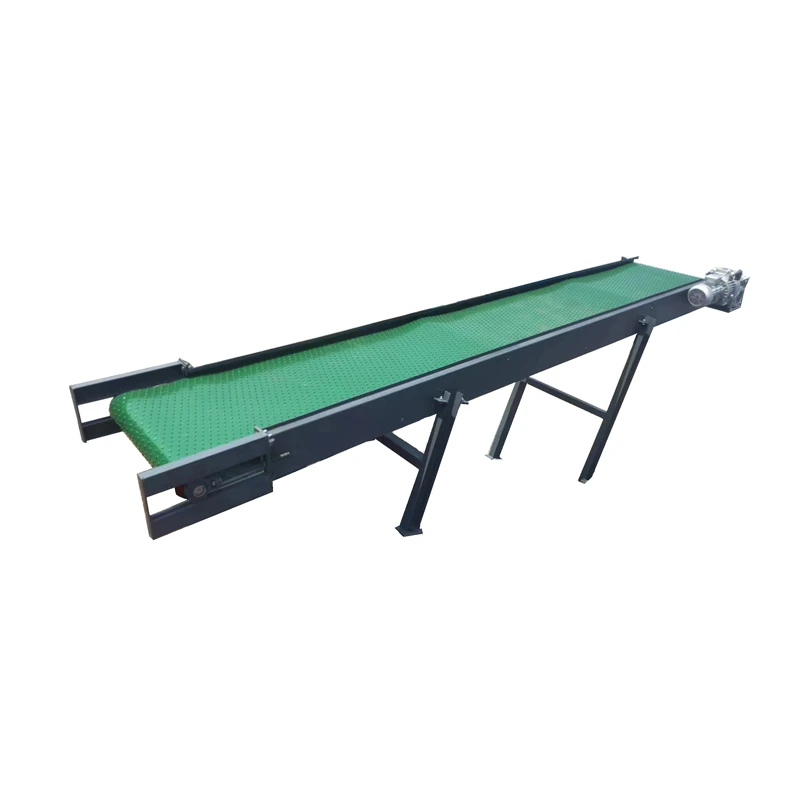
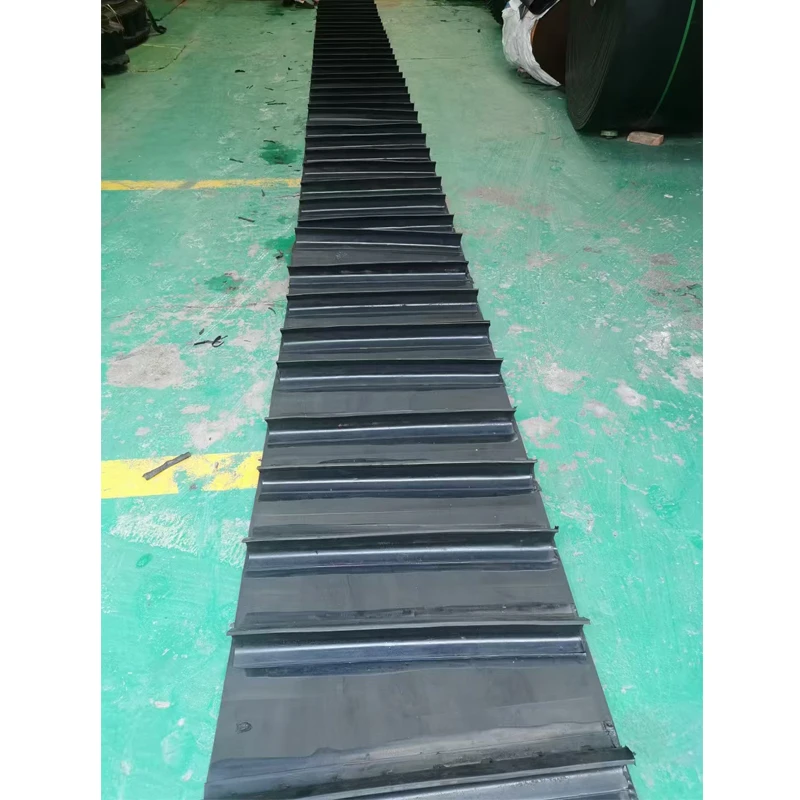
A resilient warehousing network relies on vertical material handling machinery that is both Durable and Easy-maintainable under continuous 24/7 operating schedules. Modern vertical lifting systems integrate robust modular belts featuring reinforced cleats and specialized molded pockets designed to grip cuboid boxes and cartons securely without tilting or surface deformation.
- CE Certification Compliance: Our manufactured vertical lift assemblies meet rigorous international safety standards, featuring servo-driven speed controllers and self-cleaning mechanisms.
- Latest design Modularity: Standardized belt designs accommodate box dimensions up to 600×400 mm and load weights reaching 50 kg, offering seamless adaptability to diverse production layouts.
- Advanced Material Composites: High-strength polyurethane and rubber composite belts resist abrasive wear and impact forces during high-speed vertical elevation.
Industrial Applications & Multi-Floor Integration
Facilities managing e-commerce sorting, beverage packaging, and pharmaceutical distribution require uncompromised structural reliability. Deploying a precision-engineered vertical lifting network is the most Cost-Effective method for moving boxed inventory between floors without utilizing space-wasting inclined ramps or hazard-prone manual lifts.
| Conveyor Specification | Material & Engineering Standard | Primary Industrial Application | B2B Sourcing Advantage |
|---|---|---|---|
| Standard Box Elevator Line | Polyurethane with Reinforced Cleats | E-Commerce Fulfillment, Food Packaging | Low Price, High-Volume Buy Discount |
| Servo-Controlled Vertical Unit | Servo Motor & Adjustable Speed Controller | Beverage Bottling, Pharmaceutical Sortation | High Precision, CE Certified, Ready In Stock |
| Heavy-Duty Multi-Floor System | High-Capacity Composite & Modular Belts | Heavy Industrial Staging, Warehousing | Custom OEM Sizing, Durable Construction |
B2B Supply Chain & Distributor FAQ
- Can your Company accommodate Custom OEM/ODM orders for box elevator conveyors?
- Yes. As a primary Manufacturer and Exporter, we specialize in comprehensive OEM/ODM fabrication, tailoring box size parameters, speed ranges (0.2 to 1.0 m/s), and drive configurations to meet your exact plant specifications.
- Do you provide a Free Sample or pilot evaluation prior to bulk purchase?
- Absolutely. We encourage engineering teams and Vendor networks to request component data packages or pilot testing. Once evaluated, our sales team will issue a formal Quotation tailored to your Wholesale volume.
- What are the typical lead times for international Exporter logistics?
- Standard modular components are kept In Sales inventory and can be dispatched rapidly. For fully engineered, large-scale vertical systems, our production facilities require 4-6 weeks to fulfill full container loads for export.
Optimize Your Facility's Vertical Box Handling Infrastructure
Partner with an industry-leading Manufacturer to protect your supply chain and streamline your procurement budget. Contact our engineering sales division to discuss technical specs and secure your competitive Wholesale pricing.
Request a Custom B2B Quotation