Understanding Sling Conveyors: A Comprehensive Guide
In the world of material handling, efficiency and reliability are paramount. Sling conveyors offer a versatile solution for transporting bulk materials, often providing a cost-effective and adaptable alternative to traditional conveyor systems. This article delves into the intricacies of sling conveyors, exploring their applications, benefits, design considerations, and maintenance requirements. Whether you're involved in agriculture, mining, recycling, or another industry reliant on bulk material movement, understanding sling conveyors can optimize your operations and enhance productivity.

What is a Sling Conveyor?
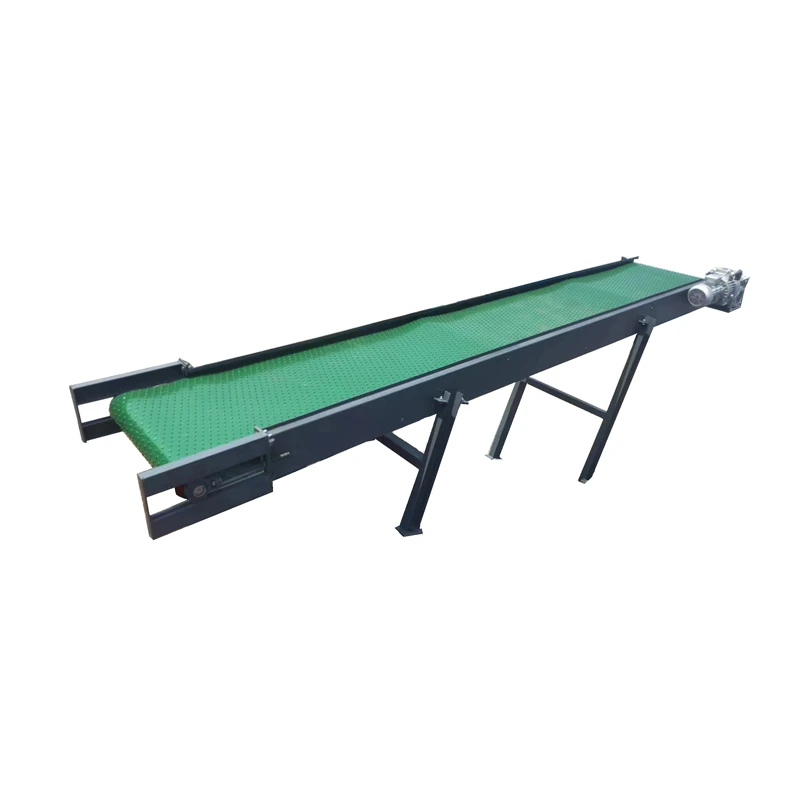
A sling conveyor, also known as a friction conveyor, utilizes a continuous belt or series of belts traveling on a low-friction surface to move materials. Unlike belt conveyors that rely on rollers, sling conveyors leverage the friction between the belt and the material itself to propel the load. This design is particularly effective for handling dry, free-flowing bulk materials like agricultural products, wood chips, sand, gravel, and recycled materials. The simplicity of the system minimizes moving parts, leading to reduced maintenance and increased reliability. You can explore various sling conveyor options to find the right fit for your specific needs.
Key Highlights: Simple design with minimal moving parts, effective for dry, free-flowing materials, and reduced maintenance requirements.
Key Benefits of Using Sling Conveyors
Sling conveyors provide several advantages over other material handling systems. They are exceptionally cost-effective, especially for longer distances, due to their lower energy consumption and reduced component count. Their adaptability is another key benefit; they can be easily configured to navigate inclines, declines, and curves. Furthermore, the gentle handling of materials minimizes product damage, which is crucial for sensitive agricultural products or recyclable materials. The simple design leads to lower maintenance costs and fewer potential points of failure, increasing uptime and overall operational efficiency.
Benefits at a Glance:
• Cost-effective for long distances
• Adaptable to inclines, declines, and curves
• Gentle material handling
• Low maintenance requirements
Sling Conveyor Applications: Diverse Industries Served
The versatility of sling conveyors makes them suitable for a broad spectrum of industries. In agriculture, they efficiently move grain, seeds, and fertilizer. The recycling industry utilizes them for handling shredded materials, plastic flakes, and metal scrap. Mining operations benefit from their ability to transport ore, coal, and aggregate. Wood processing facilities use them for moving wood chips, sawdust, and lumber. Even the cement and concrete industries employ sling conveyors for handling dry materials. From moving bulk agricultural products to processing recyclable waste, a sling conveyor system offers an efficient and reliable transportation solution.

Sling Conveyor Design Considerations and Types
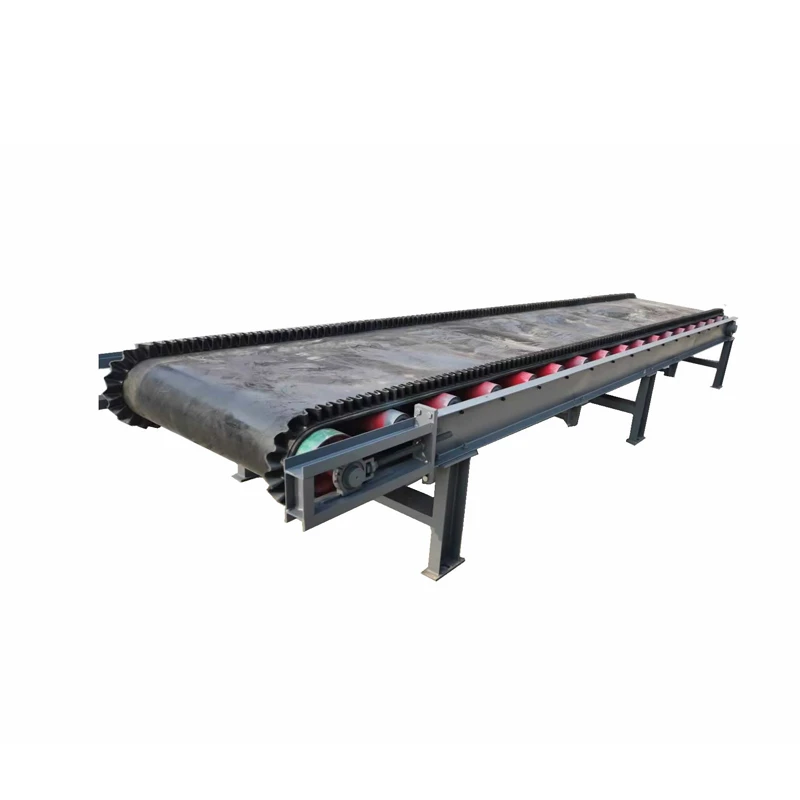
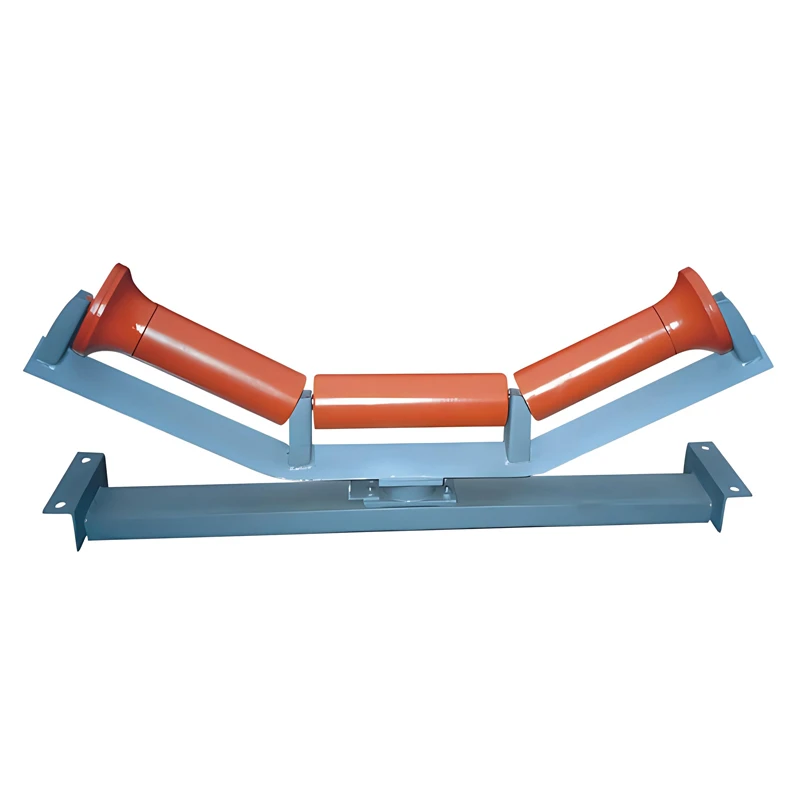
Designing a sling conveyor involves considering several factors, including material characteristics (density, particle size, abrasiveness), conveying distance, and capacity requirements. Several types of sling conveyors exist, including flat belt sling conveyors, troughed belt sling conveyors, and cleated belt sling conveyors. Flat belt conveyors are suitable for relatively flat surfaces and free-flowing materials. Troughed belt conveyors provide increased capacity by forming a trough shape with the belt. Cleated belt conveyors are designed for handling materials that require additional traction or support, such as steep inclines. Choosing the right type depends on the specific application and material properties.
Maintenance and Longevity of Sling Conveyors
While sling conveyors are known for their low maintenance requirements, regular inspections and preventative maintenance are essential for optimal performance and longevity. This includes checking belt tension, cleaning the sliding surface, and lubricating moving parts. Monitoring belt wear and tear and replacing worn components promptly is crucial. Proper alignment of the conveyor is also important to prevent premature wear. Working with a reputable supplier like HG Conveyor Belt can provide you with expert support and quality replacement parts.
Conclusion: The Efficient Choice for Bulk Material Handling
Sling conveyors represent a reliable, cost-effective, and versatile solution for a wide range of bulk material handling applications. Their simplicity, adaptability, and low maintenance requirements make them an attractive option for businesses looking to optimize their operations and improve efficiency. By understanding the different types of sling conveyors and implementing a proactive maintenance program, you can ensure years of trouble-free performance.
Frequently Asked Questions (FAQs)
What materials can a sling conveyor handle?
Sling conveyors are best suited for dry, free-flowing bulk materials like grain, wood chips, sand, gravel, recycled plastics, and agricultural products. They aren't ideal for very wet, sticky, or highly abrasive materials, as these can cause buildup and excessive wear. However, different belt materials and configurations can be utilized to accommodate a wider range of material properties. Careful consideration of the material's characteristics is essential when selecting a sling conveyor system.
What is the maximum conveying distance for a sling conveyor?
Sling conveyors can handle relatively long conveying distances, often exceeding 100 feet, and in some cases reaching several hundred feet. The maximum distance depends on factors such as material density, conveying angle, and belt tension. Longer distances may require intermediate support structures to maintain belt alignment and prevent excessive sag. Proper design and engineering are crucial for ensuring reliable operation over extended distances.
What are the key maintenance requirements for a sling conveyor?
Regular maintenance includes inspecting the belt for wear and tear, cleaning the sliding surface to remove material buildup, checking belt tension, and lubricating moving parts. It’s important to regularly align the conveyor and address any issues promptly. Replacing worn components, such as the belt or bearings, prevents more significant problems. A preventative maintenance schedule will maximize the conveyor's lifespan and minimize downtime.
How does a sling conveyor compare to a traditional belt conveyor in terms of cost?
Sling conveyors are generally more cost-effective than traditional belt conveyors, especially for longer distances. This is due to their simpler design, which requires fewer components and less energy to operate. However, the specific cost will vary depending on the application, capacity, and materials used. For applications requiring precise material control or handling of fragile materials, a traditional belt conveyor may be more suitable, but for many bulk material handling tasks, a sling conveyor offers a significant cost advantage.