The Ultimate Guide to Choosing a Dust Proof Conveyor for Industrial Efficiency
In many industrial environments, airborne particulates and dust are more than just a nuisance; they are a significant threat to machinery longevity, product purity, and worker health. Implementing a high-quality dust proof conveyor is the most effective way to mitigate these risks. By enclosing the transport process, these systems prevent hazardous dust from escaping into the workspace while protecting the materials being moved from external contamination. Whether you are dealing with pharmaceutical powders, chemical granules, or food ingredients, selecting the right conveyor system is critical for maintaining a sterile and safe operational flow. In this guide, we will explore the technical advantages and strategic implementations of dust-containment conveying technology.

How a Dust Proof Conveyor Enhances Workplace Safety
The primary objective of a dust proof conveyor is to create a sealed environment for material transport. Dust accumulation in an industrial setting can lead to severe respiratory issues for employees and, in extreme cases, create a risk of combustible dust explosions. By utilizing airtight seals and enclosed housings, these conveyors ensure that fine particles remain trapped within the system. Advanced filtration and negative pressure systems are often integrated to further purify the air, ensuring that the surrounding environment remains clean. This not only meets stringent health and safety regulations but also reduces the frequency and cost of facility-wide cleaning.
Safety Impact: Enclosed conveying systems can reduce airborne dust concentrations by up to 95%, significantly lowering the risk of occupational asthma and enhancing overall visibility within the production plant.
Key Design Features of Modern Dust Proofing Systems
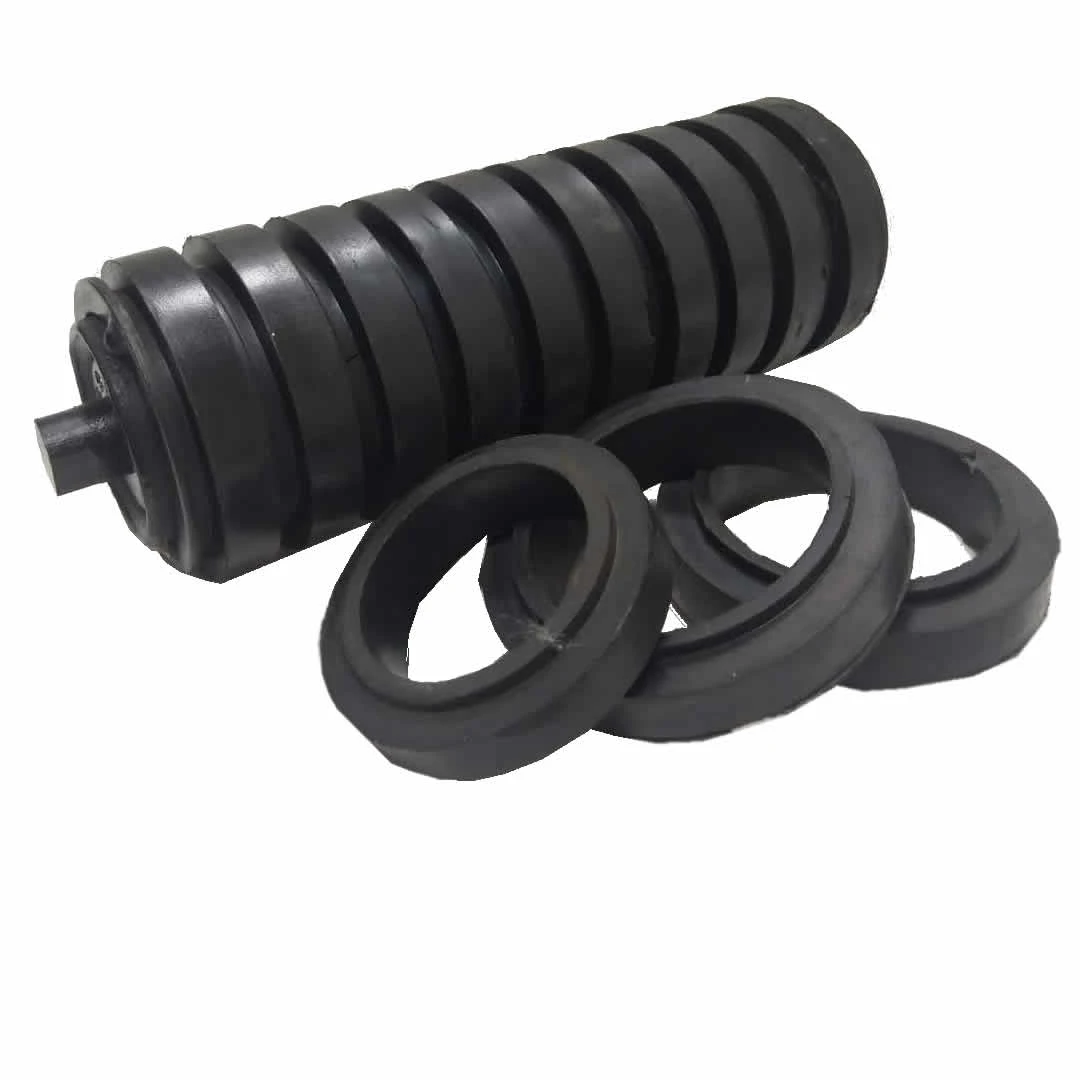
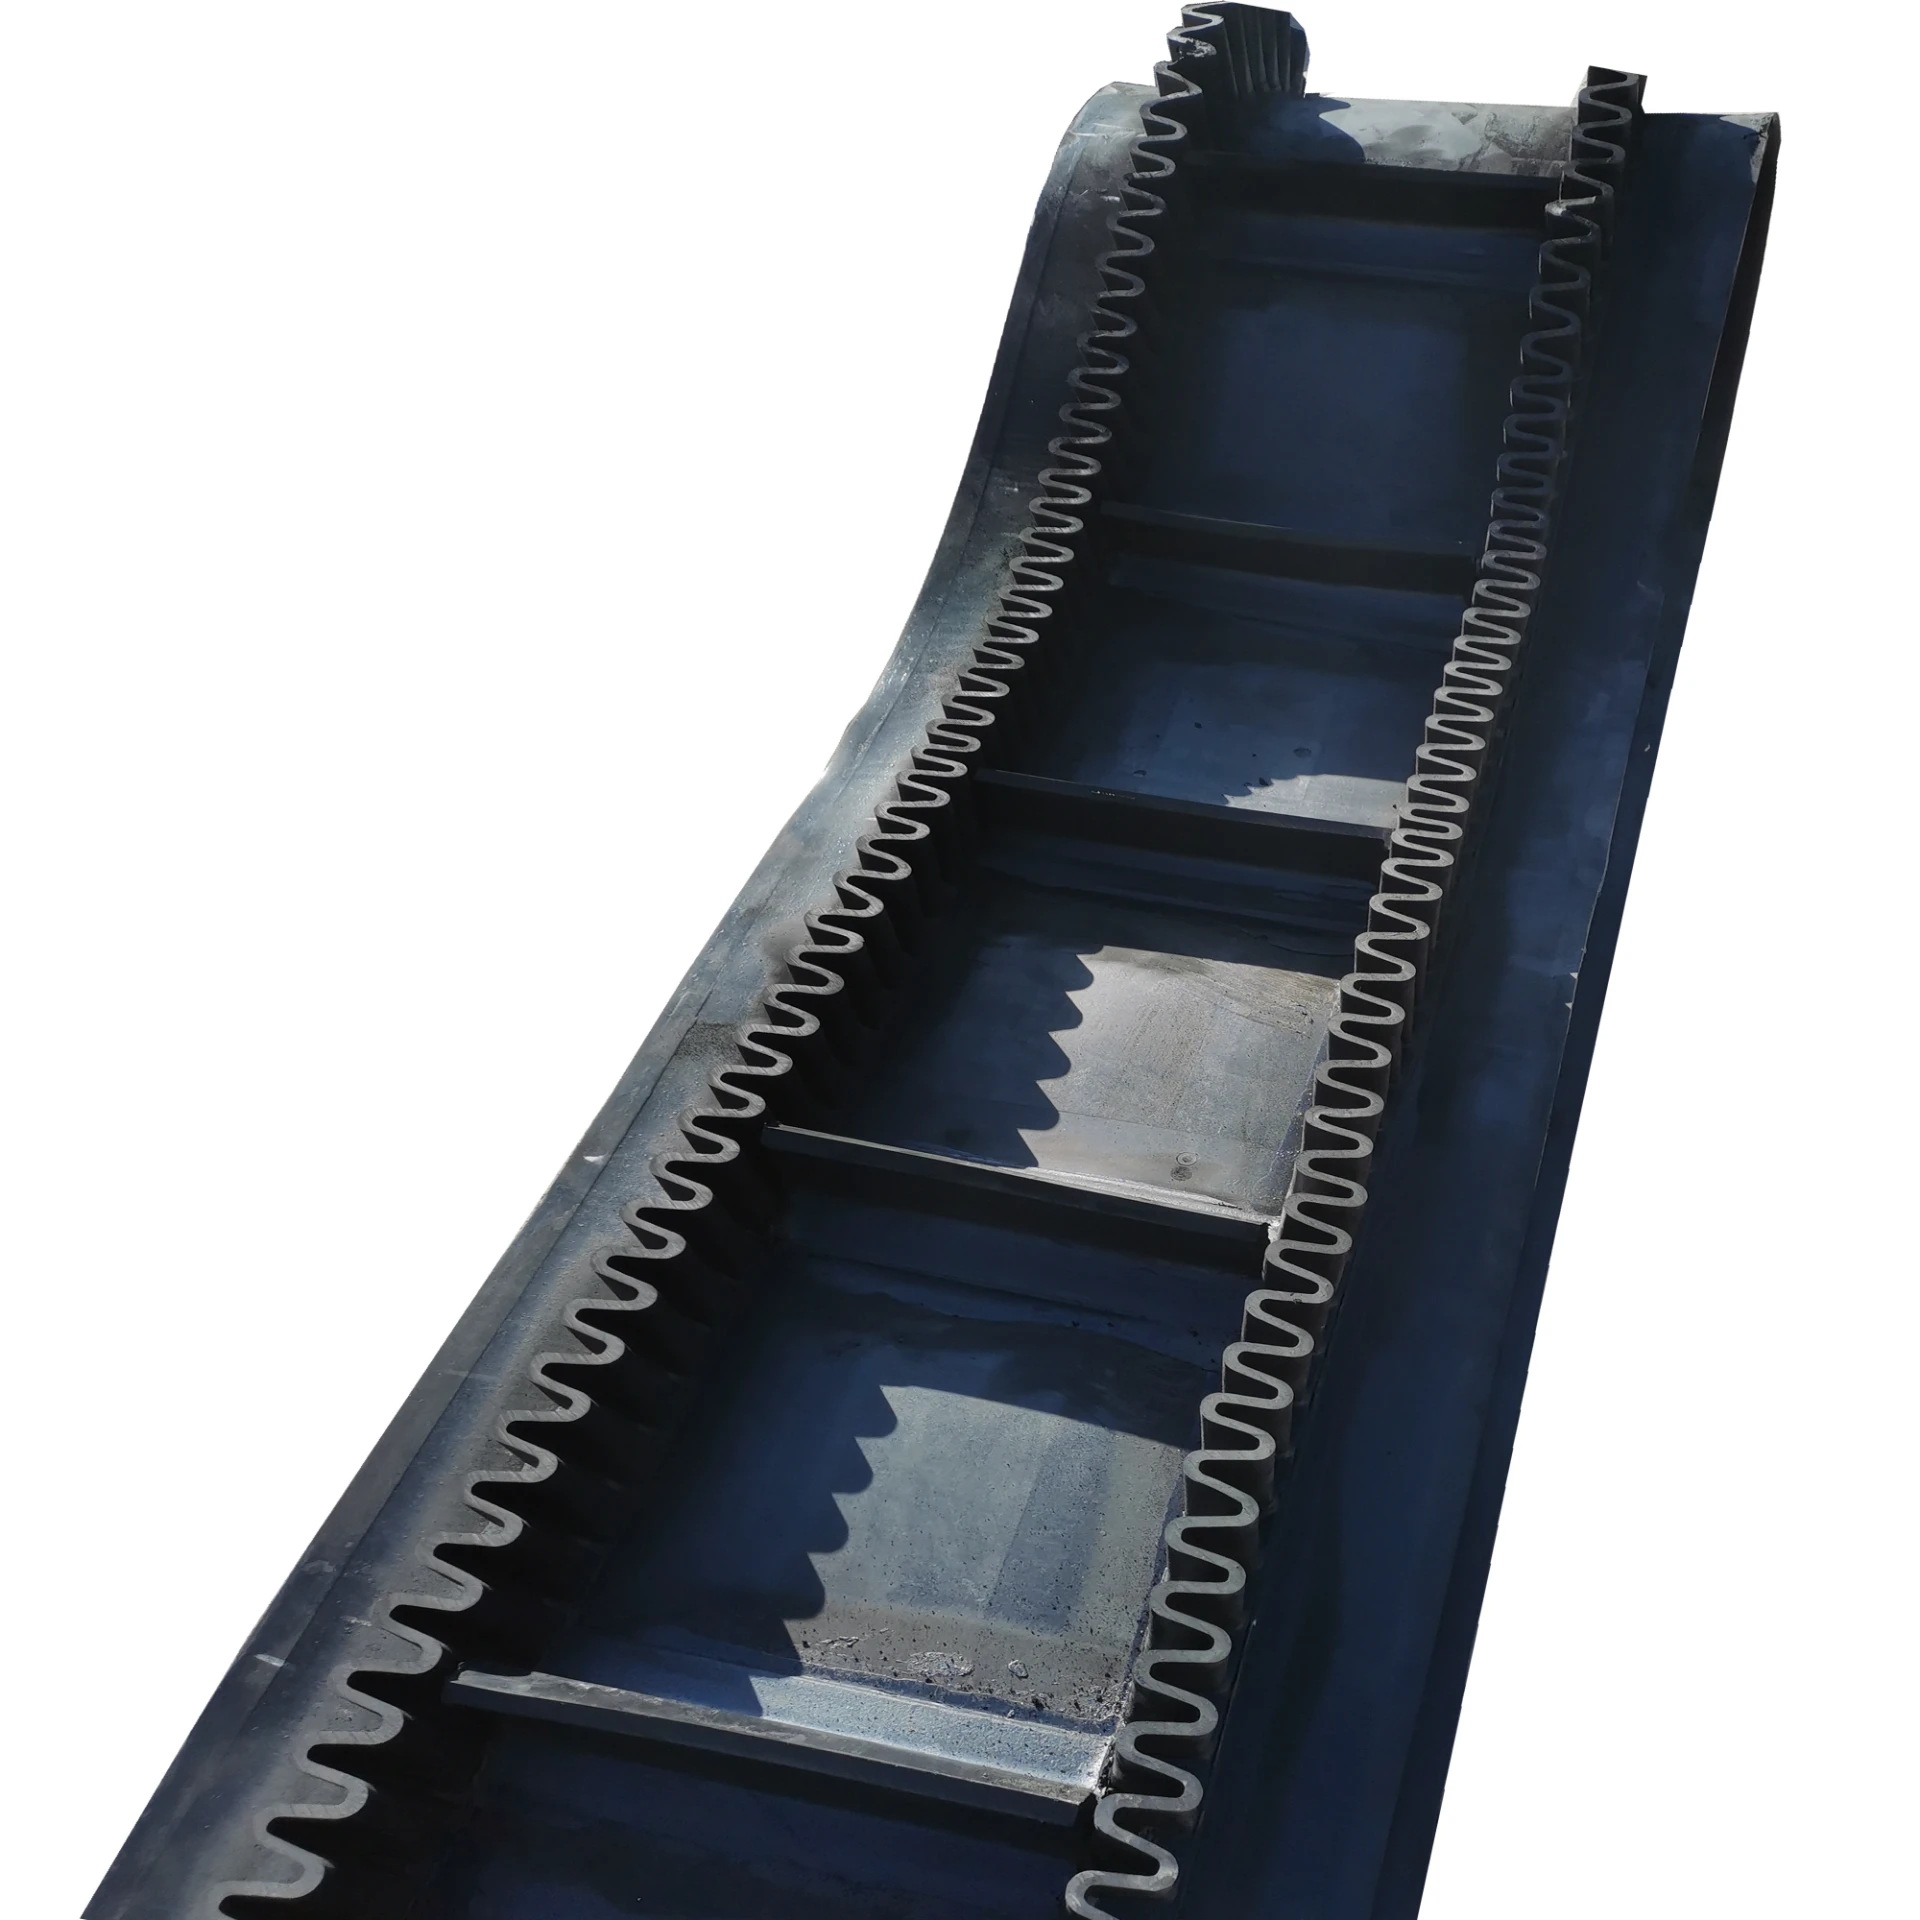
Not all enclosed conveyors are created equal. A professional-grade dust proof conveyor incorporates specific engineering elements to ensure a total seal. This includes the use of specialized skirt rubber to prevent leakage at loading points and high-precision gaskets at all joint interfaces. Furthermore, the choice of belt material is crucial; anti-static belts are often used to prevent the buildup of static electricity, which could otherwise ignite flammable dust. The integration of smooth internal surfaces also prevents material buildup, which reduces friction and prevents the "clogging" effect common in low-end systems.
Critical Engineering Components:
• Airtight Covers: High-grade stainless steel or polymer housings.
• Precision Sealing: Specialized gaskets that maintain vacuum or pressure.
• Anti-Static Materials: Reducing spark risks in volatile environments.
• Modular Design: Allowing for easy access during maintenance without compromising the seal.
Comparing Dust Proof Conveyor Options vs. Open Systems
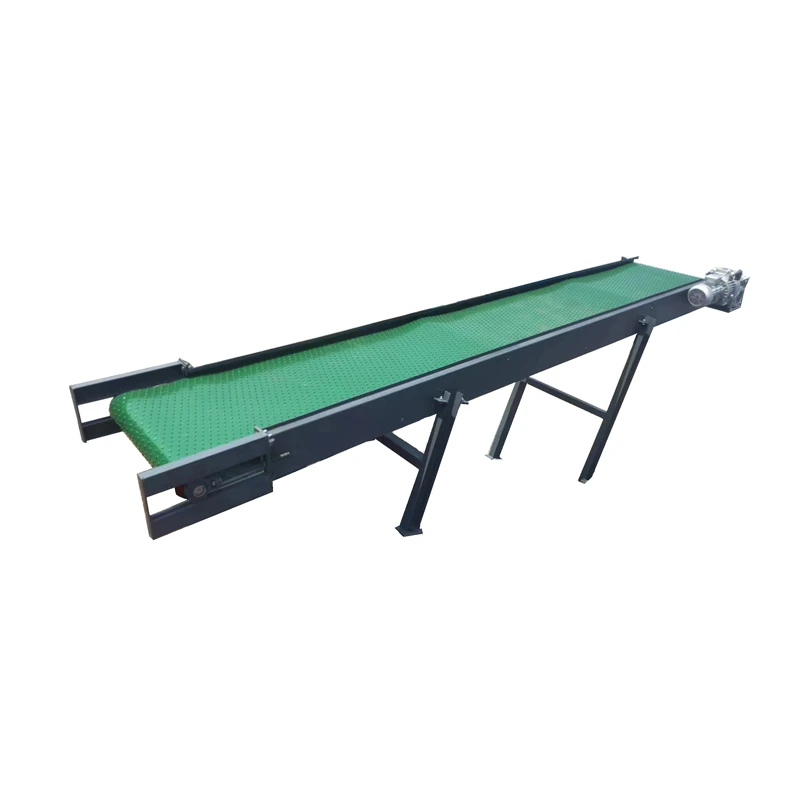
When deciding between an open belt and a dust proof conveyor, the decision usually comes down to the nature of the material. Open systems are cheaper to install but lead to significant product loss through "windage" and contamination. In contrast, enclosed systems protect the product from moisture and external debris, ensuring that the final output meets high quality standards. The long-term ROI of a dust-proof system is realized through lower waste, reduced cleaning labor, and eliminated downtime caused by dust-related machinery failure.
Industrial Applications of the Dust Proof Conveyor
The application of a dust proof conveyor spans across multiple high-precision sectors. In the pharmaceutical industry, preventing cross-contamination between different medicine batches is a legal requirement. In food processing, keeping flour, sugar, or spices contained ensures hygiene and prevents pests. Additionally, the mining and chemical sectors utilize these systems to transport abrasive or toxic powders that would otherwise compromise the structural integrity of the plant or endanger personnel. The versatility of these systems allows them to be integrated into existing production lines with minimal disruption.

Technical Specifications for Optimal Performance
To achieve maximum efficiency, a dust proof conveyor must be customized based on the material density, flow rate, and environmental conditions. Choosing the correct belt tension and drive motor is essential to prevent belt slippage, which can cause dust to leak at the drive pulley. Below are the typical technical specifications for a medium-to-heavy duty industrial dust-proof system:
Conclusion: Optimizing Production with Dust Containment
Investing in a professional dust proof conveyor is a strategic decision that pays dividends in safety, quality, and operational efficiency. By eliminating airborne contaminants and protecting the product stream, businesses can significantly reduce waste and ensure a healthier environment for their workforce. From the pharmaceutical lab to the industrial mine, the right containment system is the foundation of a modern, clean production line. Upgrade your facility today for a cleaner, safer tomorrow.
Frequently Asked Questions (FAQs)
How does a dust proof conveyor differ from a standard enclosed conveyor?
While a standard enclosed conveyor simply has a cover, a true dust proof conveyor is engineered for airtightness. This involves precision-machined joints, specialized skirt rubber to prevent "blow-back" of dust at the loading point, and specific gaskets. A standard cover prevents large debris from falling in, but a dust-proof system prevents microscopic particles from escaping, making it suitable for hazardous or sterile environments.
Which materials are best for the belt in a dust-proof system?
The choice of belt depends on the material being conveyed. For food and pharma, FDA-approved PU or PVC belts are used to ensure hygiene. In chemical plants, oil-resistant and heat-resistant elastomers are preferred. Crucially, for fine powders, anti-static belts are mandatory to prevent electrostatic discharge (ESD), which could lead to sparks in a dust-rich environment. We recommend consulting with specialists to match the belt chemistry with your specific material.
How do I maintain the seals on a dust proof conveyor?
Maintenance is key to ensuring the system remains airtight. We recommend a weekly inspection of the skirt rubber for wear and tear, as this is the most common leak point. Gaskets should be checked monthly for cracks or compression sets. Additionally, clearing any material buildup around the pulleys prevents belt misalignment, which can create gaps in the sealing. Using a modular cover design allows maintenance teams to access the interior quickly without permanently damaging the seals.
Can these systems be integrated into an existing production line?
Yes, most dust proof conveyor systems are designed with a modular approach. This means they can be installed in sections or as a retrofit over existing belts (though a full replacement is often more efficient for a perfect seal). By coordinating the transition points—such as chutes and hoppers—with specialized seals, we can convert an open system into a dust-contained system with minimal downtime for your facility.