Maximizing Efficiency with Advanced Conveyors Equipment
In the fast-paced world of modern logistics and manufacturing, the seamless movement of materials is the heartbeat of operational success. Investing in high-quality conveyors equipment is no longer just an upgrade—it is a necessity for businesses aiming to reduce manual labor, minimize errors, and accelerate throughput. Whether you are managing a massive warehouse or a precision assembly line, the right conveying system can transform your bottom line by optimizing workflow and enhancing workplace safety. This guide explores the essential aspects of industrial conveying systems to help you make an informed investment.

Types of Conveyors Equipment for Diverse Applications
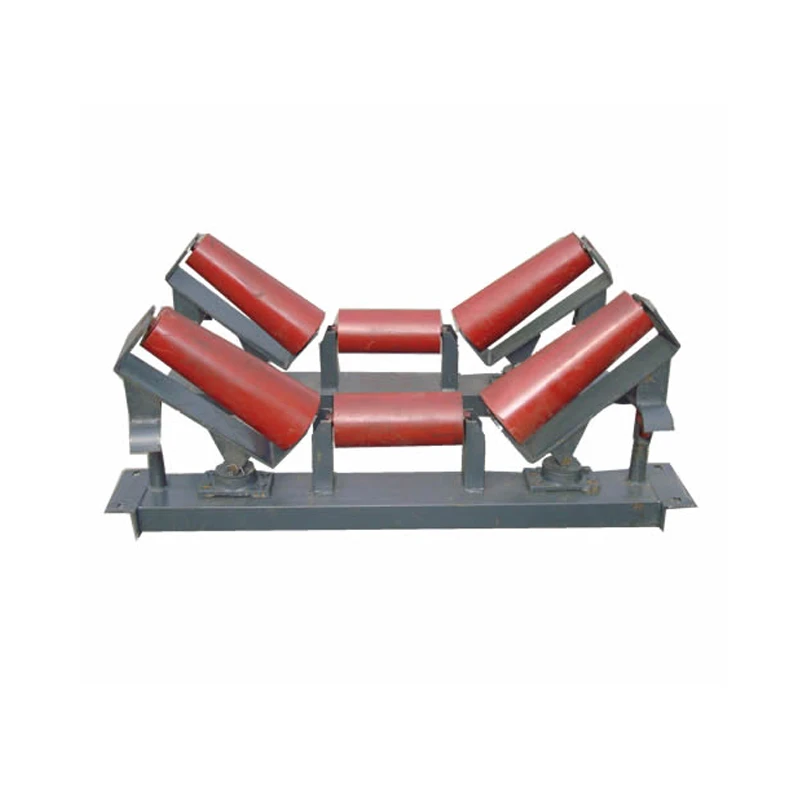
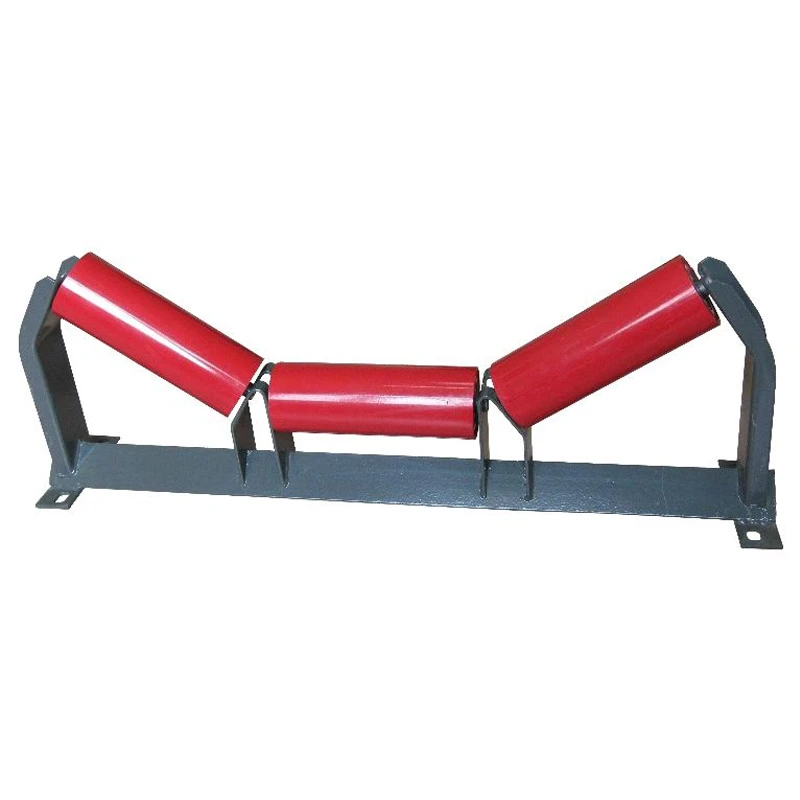
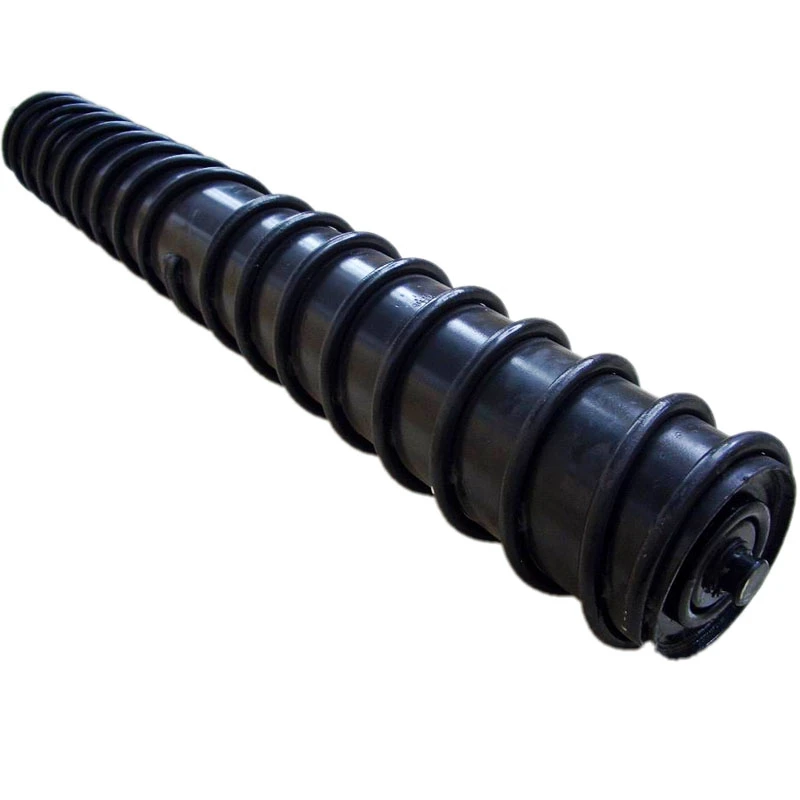
Not all materials are created equal, and neither are the systems used to move them. Depending on the weight, fragility, and destination of your goods, different conveyors equipment will offer varying degrees of efficiency. Belt conveyors are the most versatile, ideal for general purpose transport, while roller conveyors excel in handling heavy boxes and pallets. For steep inclines, bucket elevators or screw conveyors provide the necessary lift. Understanding these distinctions ensures that your facility avoids bottlenecks and reduces wear and tear on the machinery, ultimately extending the lifespan of your hardware.
Industry Insight: Modular belt systems are becoming increasingly popular due to their ease of maintenance; a single damaged module can be replaced without needing to replace the entire belt, drastically reducing downtime.
Comparing Belt vs. Roller Conveyors Equipment
Choosing between a belt and a roller system often depends on the nature of the load. Belt systems provide a continuous surface, making them perfect for small items or bulk materials like grain. On the other hand, roller systems are designed for rigid items with a flat bottom. By analyzing the specific needs of your production line, you can select the conveyors equipment that offers the best ROI. Below is a detailed comparison to assist your decision-making process.
Key Components of High-Performance Conveyors Equipment
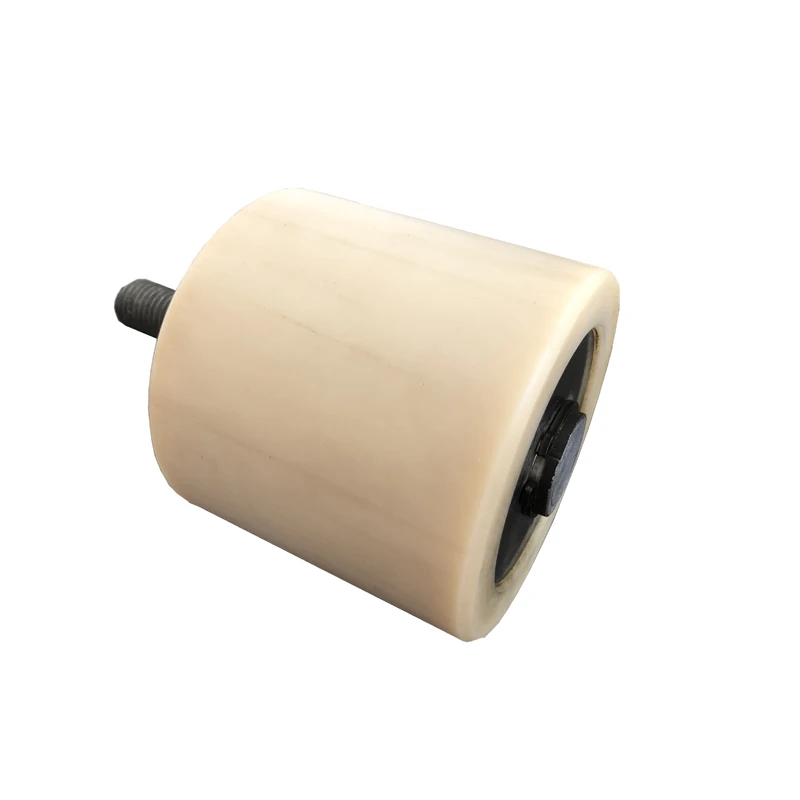
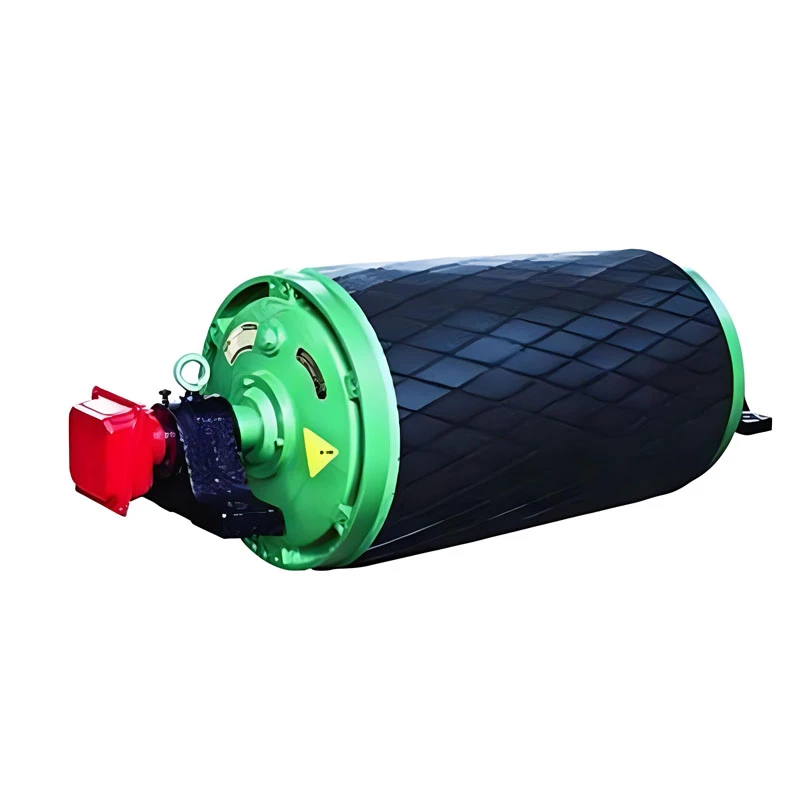
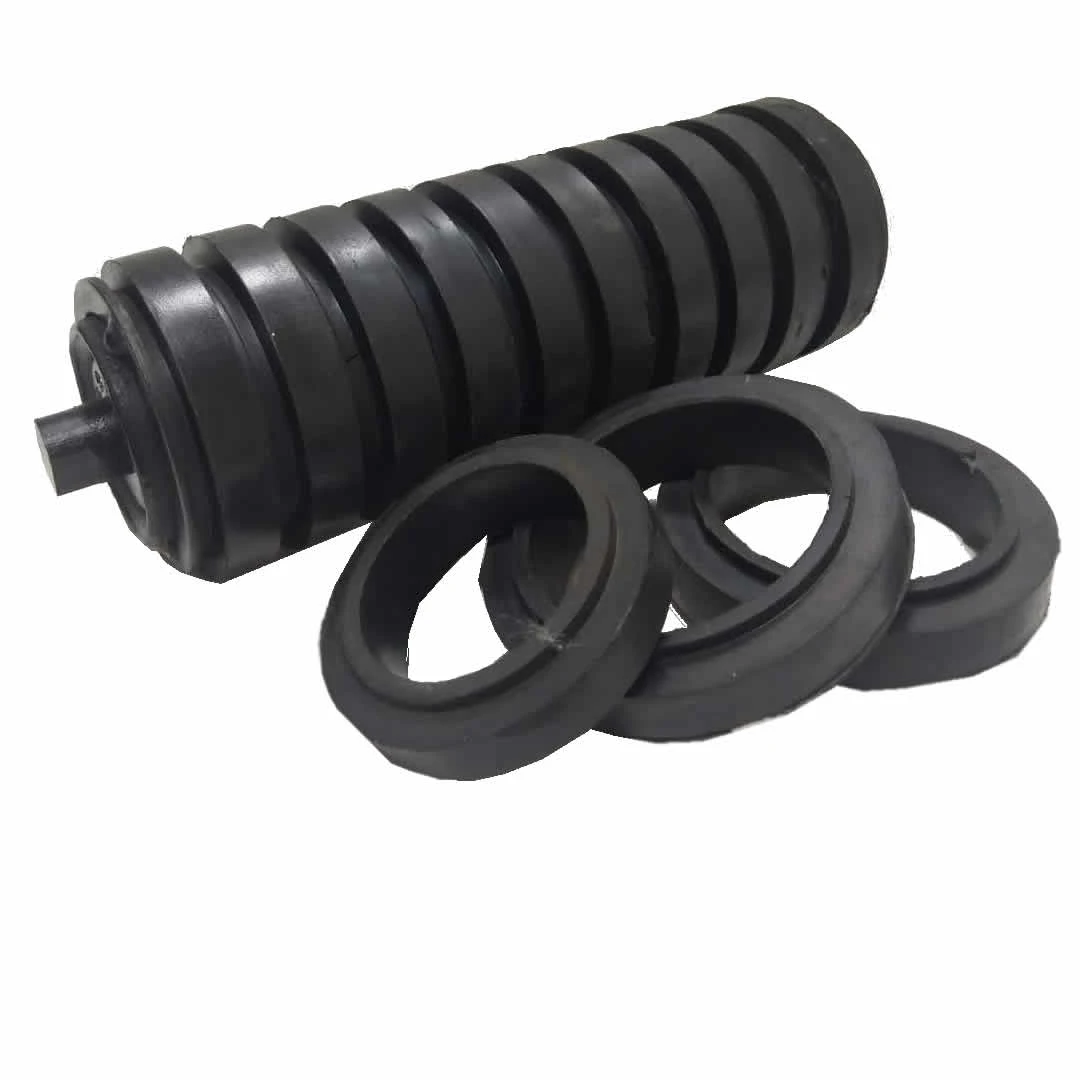
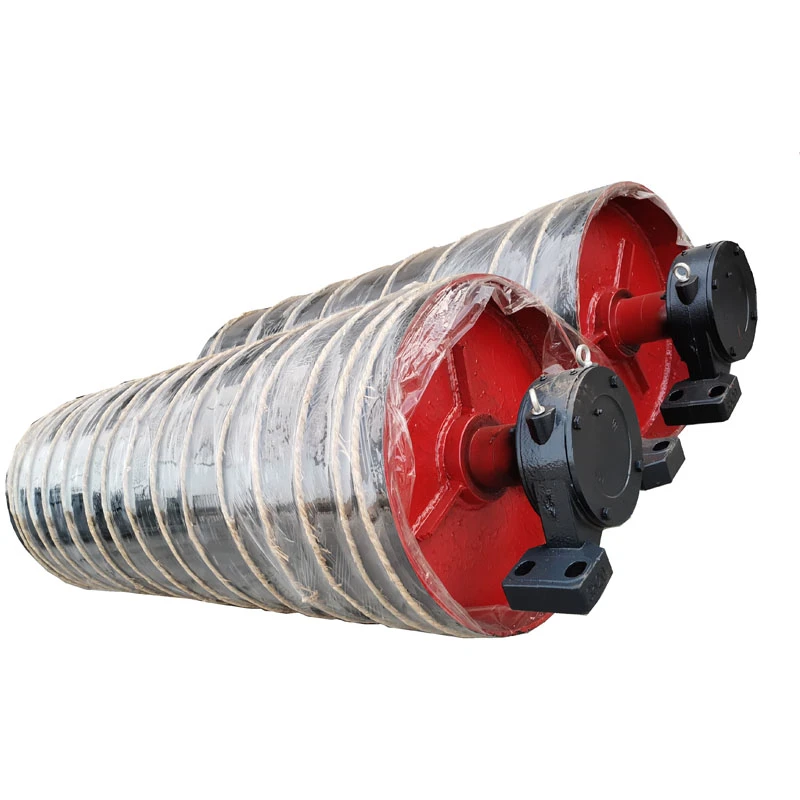
The efficiency of any conveyor system is only as strong as its weakest component. High-performance conveyors equipment consists of several critical parts working in harmony. The drive motor provides the power, the pulleys guide the direction, and the conveyor belt serves as the transport medium. Using premium materials like reinforced rubber or PVC ensures that the belt can withstand abrasive materials and extreme temperatures. Furthermore, integrating sensors and PLC (Programmable Logic Controllers) allows for automated sorting and speed adjustment, reducing the risk of human error and increasing overall output.

Maintenance Strategies for Industrial Conveyors Equipment
Preventive maintenance is the key to avoiding costly unplanned downtime. For those operating conveyors equipment, a scheduled inspection routine is vital. This includes checking for belt misalignment, lubricating bearings, and inspecting drive belts for signs of wear. Overloaded systems often suffer from premature belt failure; thus, ensuring that the load capacity is never exceeded is critical. Implementing a digital monitoring system can provide real-time alerts on motor heat or belt slippage, allowing maintenance teams to intervene before a total system failure occurs.
Maintenance Checklist:
• Weekly: Check belt tension and alignment
• Monthly: Lubricate all moving joints and rollers
• Quarterly: Inspect motor brushes and electrical connections
• Annually: Comprehensive structural integrity audit
Technical Specifications for Custom Conveyors Equipment
When ordering custom conveyors equipment, technical precision is paramount. You must consider the belt width, speed, and the environment in which the machine will operate. For example, food-grade conveyors require stainless steel frames and FDA-approved belt materials to prevent contamination. In contrast, mining equipment requires heavy-duty steel and abrasion-resistant rubber. The following table outlines standard specifications for common industrial configurations.
Conclusion: Elevating Production with the Right Conveyors Equipment
Choosing the correct conveyors equipment is a strategic decision that impacts every facet of your production chain. From selecting the appropriate belt material to implementing a rigorous maintenance schedule, each detail contributes to a more efficient and safer work environment. By leveraging modern technology and high-quality engineering, your business can achieve unprecedented levels of productivity and scalability. Invest in quality today to ensure a seamless flow of operations tomorrow.
Frequently Asked Questions (FAQs)
How do I choose the right belt material for my conveyors equipment?
Choosing the right material depends on three primary factors: the product being transported, the environment, and the load weight. If you are handling food, you must use FDA-approved, non-toxic materials like polyurethane. For industrial chemicals, oil-resistant rubber is necessary to prevent the belt from degrading. If you are moving heavy ores or stones, a steel-cord reinforced belt is the best choice for strength and longevity. Always consult with a specialist at hgconveyorbelt.com to ensure the material matches your specific chemical and physical requirements.
What are the most common causes of conveyor belt failure?
The most frequent cause of failure is improper belt tracking, which leads to the belt rubbing against the frame and fraying the edges. Overloading the system beyond its rated capacity also causes stretching and eventual snapping. Additionally, lack of lubrication in the rollers increases friction and heat, which can melt synthetic belts or seize motors. Regular inspections and the use of high-quality conveyors equipment can mitigate these risks and ensure a much longer operational lifespan.
Can I upgrade my existing conveyor system to be automated?
Yes, most traditional conveyor systems can be retrofitted for automation. This typically involves adding Variable Frequency Drives (VFDs) to control motor speed, installing photo-eye sensors to detect product presence, and integrating a PLC system to coordinate the flow between different conveyor sections. Automation not only increases speed but also significantly reduces labor costs and eliminates human error in sorting and routing. For professional integration and hardware upgrades, visiting a specialized provider of conveyors equipment is the recommended first step.
How often should I replace the belts in my conveying system?
There is no one-size-fits-all answer, as it depends entirely on the wear and tear. However, light-duty PVC belts in a clean warehouse may last several years, while heavy-duty rubber belts in a quarry might need replacement every 6 to 12 months. The key is to monitor for "witness marks" such as cracks, thinning of the cover, or visible reinforcement cords. If the belt begins to slip frequently despite tensioning, it is likely stretched beyond its limit and should be replaced immediately to avoid a sudden production halt.