- Engineering Architecture & Incline Drive Mechanics
- OEM/ODM Custom Manufacturing Matrix & Specifications
- TCO Economics & Vertical Space Footprint Optimization
- B2B Sourcing Comparison: Direct China Factory vs. Distributors
- Heavy-Duty Multi-Tier Logistics & Assembly Integration
- B2B Procurement FAQ & Technical Sourcing Guide
Multi-level packaging facilities, mezzanine storage transfers, and continuous production lines require robust vertical transport systems capable of continuous incline handling without load slippage or structural fatigue. For factory automation engineers, plant operations directors, and OEM procurement managers, installing an industrial-grade Elevating Conveyor eliminates manual lifting bottlenecks, maximizes vertical factory cube utilization, and ensures reliable material flow across high-capacity production cells.
Engineering Architecture & Incline Drive Mechanics
Standard horizontal conveyor belts experience severe load slippage and motor back-drive risks when elevated past slight angles. A heavy-duty Elevating Conveyor combines high-tensile carcass materials, positive mechanical cleats, and electromagnetic brake motors to ensure smooth vertical transport without continuous product rollback.
- Structural Metallurgy: Frames are fabricated from heavy-gauge structural carbon steel (Q235B) with hot-dip galvanization or laser-cut AISI 304/316 stainless steel to deliver long service life in abrasive and washdown environments.
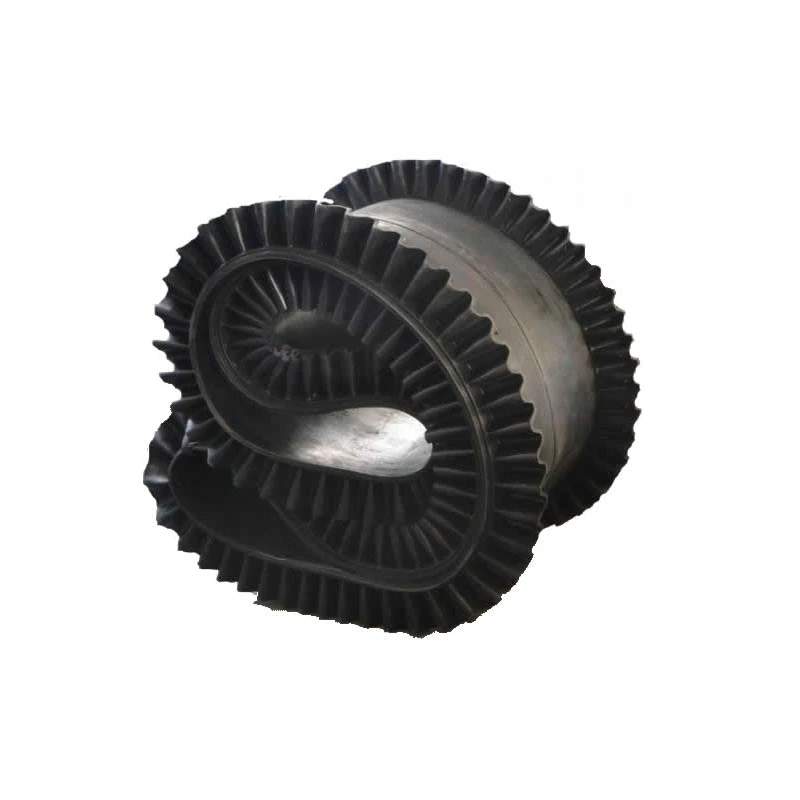
- Positive-Grip Belting: Integrates multi-ply synthetic rubber, high-density PVC, or modular plastic belting equipped with high-frequency (RF) welded cross-cleats (heights 20 mm to 100 mm) to contain discrete items and loose bulk parts.
- Fail-Safe Drivetrain Engineering: Equipped with precision worm or helical-bevel gearmotors (0.37 kW to 7.5 kW) matched with automatic electromagnetic holding brakes to prevent gravitational rollback during unplanned power loss.
- Sanitary Clean-In-Place (CIP) Options: Available with quick-release belt tensioning levers and open stainless side channels, allowing complete washdown sanitization in compliance with FDA and EU food safety standards.
Procurement Insight: Sourcing direct from a specialized China manufacturing plant allows procurement managers to customize cleat pitch, belt durometer, and side-skirt containment profiles to match exact material bulk densities and prevent edge jamming.
OEM/ODM Custom Manufacturing Matrix & Specifications
To support system integrators and packaging line builders, our manufacturing lines produce customized Elevating Conveyor assemblies based on client CAD layouts and payload requirements:
| Engineering Parameter | Standard Factory Spec | Custom OEM/ODM Capabilities |
|---|---|---|
| Conveyor Length (Span) | 2.0 m – 30.0 m | Modular linked sections engineered beyond 50 m |
| Incline Angle Range | 15° – 45° Standard | Steep incline up to 60° (Corrugated sidewall designs) |
| Effective Belt Width | 300 mm – 1,500 mm | Custom wide-bed formats up to 2,200 mm |
| Motor Power Rating | 0.37 kW – 7.5 kW Gearmotor | High-efficiency IE3/IE4 or Explosion-Proof (ATEX) |
| Frame Construction | Galvanized Steel / Powder-Coated Steel | AISI 304/316 Stainless Steel, Anodized Aluminum |
| Carrying Surface Options | Flat, Cleated PVC/Rubber, Modular POM | Textured high-friction grip-top, Silicone release |
TCO Economics & Vertical Space Footprint Optimization
Procuring a rugged Elevating Conveyor delivers direct economic returns by optimizing facility floor space utilization and minimizing manual material handling costs:
- Vertical Footprint Compression: Elevating goods at steep angles (up to 45° or greater) reduces horizontal floor space consumption by up to 50% compared to extended low-incline conveyor runs.
- Zero Product Impact & Rollback Loss: Positive cleat containment prevents fragile cartons, glass bottles, and bulk parts from sliding backward and sustaining impact damage during elevation.
- Lower Maintenance Overhead: Sealed precision bearings and high-frequency welded cleats eliminate premature delamination, driving down routine maintenance labor and replacement costs.
B2B Sourcing Comparison: Direct China Factory vs. Distributors
Partnering directly with a primary conveyor manufacturer ensures complete metallurgical traceability, tailored engineering designs, and tiered wholesale pricing. Review the comparison below between regional resellers and direct manufacturing via HG Conveyor Belt:
| Procurement Factor | HG Conveyor Belt (Direct OEM Factory) | Regional Conveyor Distributors | General Workshop Fabricators |
|---|---|---|---|
| Pricing Structure | Direct Tiered Factory Wholesale Pricing | 30% – 50% Middleman Markup Added | Low Initial Quote / High Weld Failure Risk |
| Material Verification | 100% Mill Test Certificates (MTC) & COA | Secondary trading documentation | Mixed uncertified carbon steel stock |
| OEM Customization | Full 3D STP/DWG modeling & cleat tooling | Standard off-the-shelf catalog only | Limited cleat heights & tooling capability |
| Export Lead Times | 2 – 4 Weeks (Factory dynamic tested) | 6 – 10 Weeks (Backordered sourcing) | 5 – 8 Weeks (Inconsistent delivery) |
| Quality Assurance | ISO 9001 certified, 48-hr full-load burn-in | Visual packaging inspection only | No pre-shipment dynamic load testing |
Heavy-Duty Multi-Tier Logistics & Assembly Integration
Engineering teams and system integrators install precision elevating conveyor sections across demanding production environments:
- Food & Beverage Packaging: Elevating bottled drinks, canned goods, and snack pouches from primary packaging to multi-head weighers and case packers.
- Automated E-Commerce & Mezzanines: Continuous vertical carton and tote transfers between ground-floor sorting lines and upper-level picking mezzanines.
- Automotive Parts & Stamping: Transferring stamped metal blanks, fasteners, and heavy hardware from press pits into mobile parts bins.
- Agriculture & Bulk Grain Handling: Elevating harvested crops, bulk pellets, and seeds with gentle-handling food-grade cleated belts.
B2B Procurement FAQ & Technical Sourcing Guide
Our production facility accommodates single custom conveyor orders (MOQ: 1 turnkey unit) as well as continuous volume supply contracts for system integrators and automation line builders.
Yes. We supply free sample swatches of cleated PVC, synthetic rubber, and modular plastic belt links to qualified engineering and procurement teams for material validation and chemical compatibility testing.
Every incline drive unit includes an integrated electromagnetic fail-safe brake motor or backstop bearing that engages instantly upon power loss, mechanically locking the belt in place.
Every factory export shipment includes CE Machinery Directive compliance declarations, ISO 9001 quality audit sheets, raw material Mill Test Certificates (MTC), motor test sheets, and complete electrical schematics.
Request a Factory Wholesale Quotation
Partner directly with an established China conveyor manufacturing plant. Submit your project floor plans, elevation parameters, and payload targets to receive detailed 3D CAD integration drawings and competitive wholesale pricing.
Contact Our Engineering Sales Team