In modern industrial manufacturing, bulk distribution, and heavy material processing, supply chain continuity and equipment uptime dictate profitability. Procurement managers and OEMs understand that integrating a High-Quality material conveyor is critical to minimizing operational downtime and maximizing yield rates. Sourcing directly from an established Manufacturer in China allows global supply chains to secure Advanced, CE Certified infrastructure components while maintaining strict cost control.
Table of Contents: B2B Sourcing Guide
- Engineering High-Performance Material Conveyor Systems
- Applications of the Bulk Material Conveyor
- Flexibility & Deployment of the Portable Material Conveyor
- Wholesale Procurement FAQ

Engineering High-Performance material conveyor systems
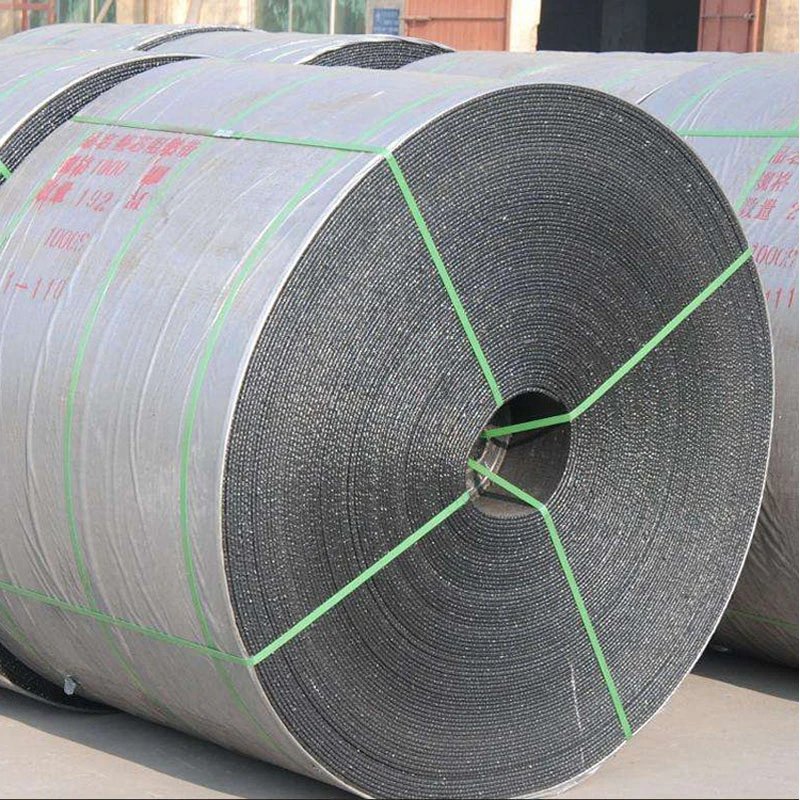
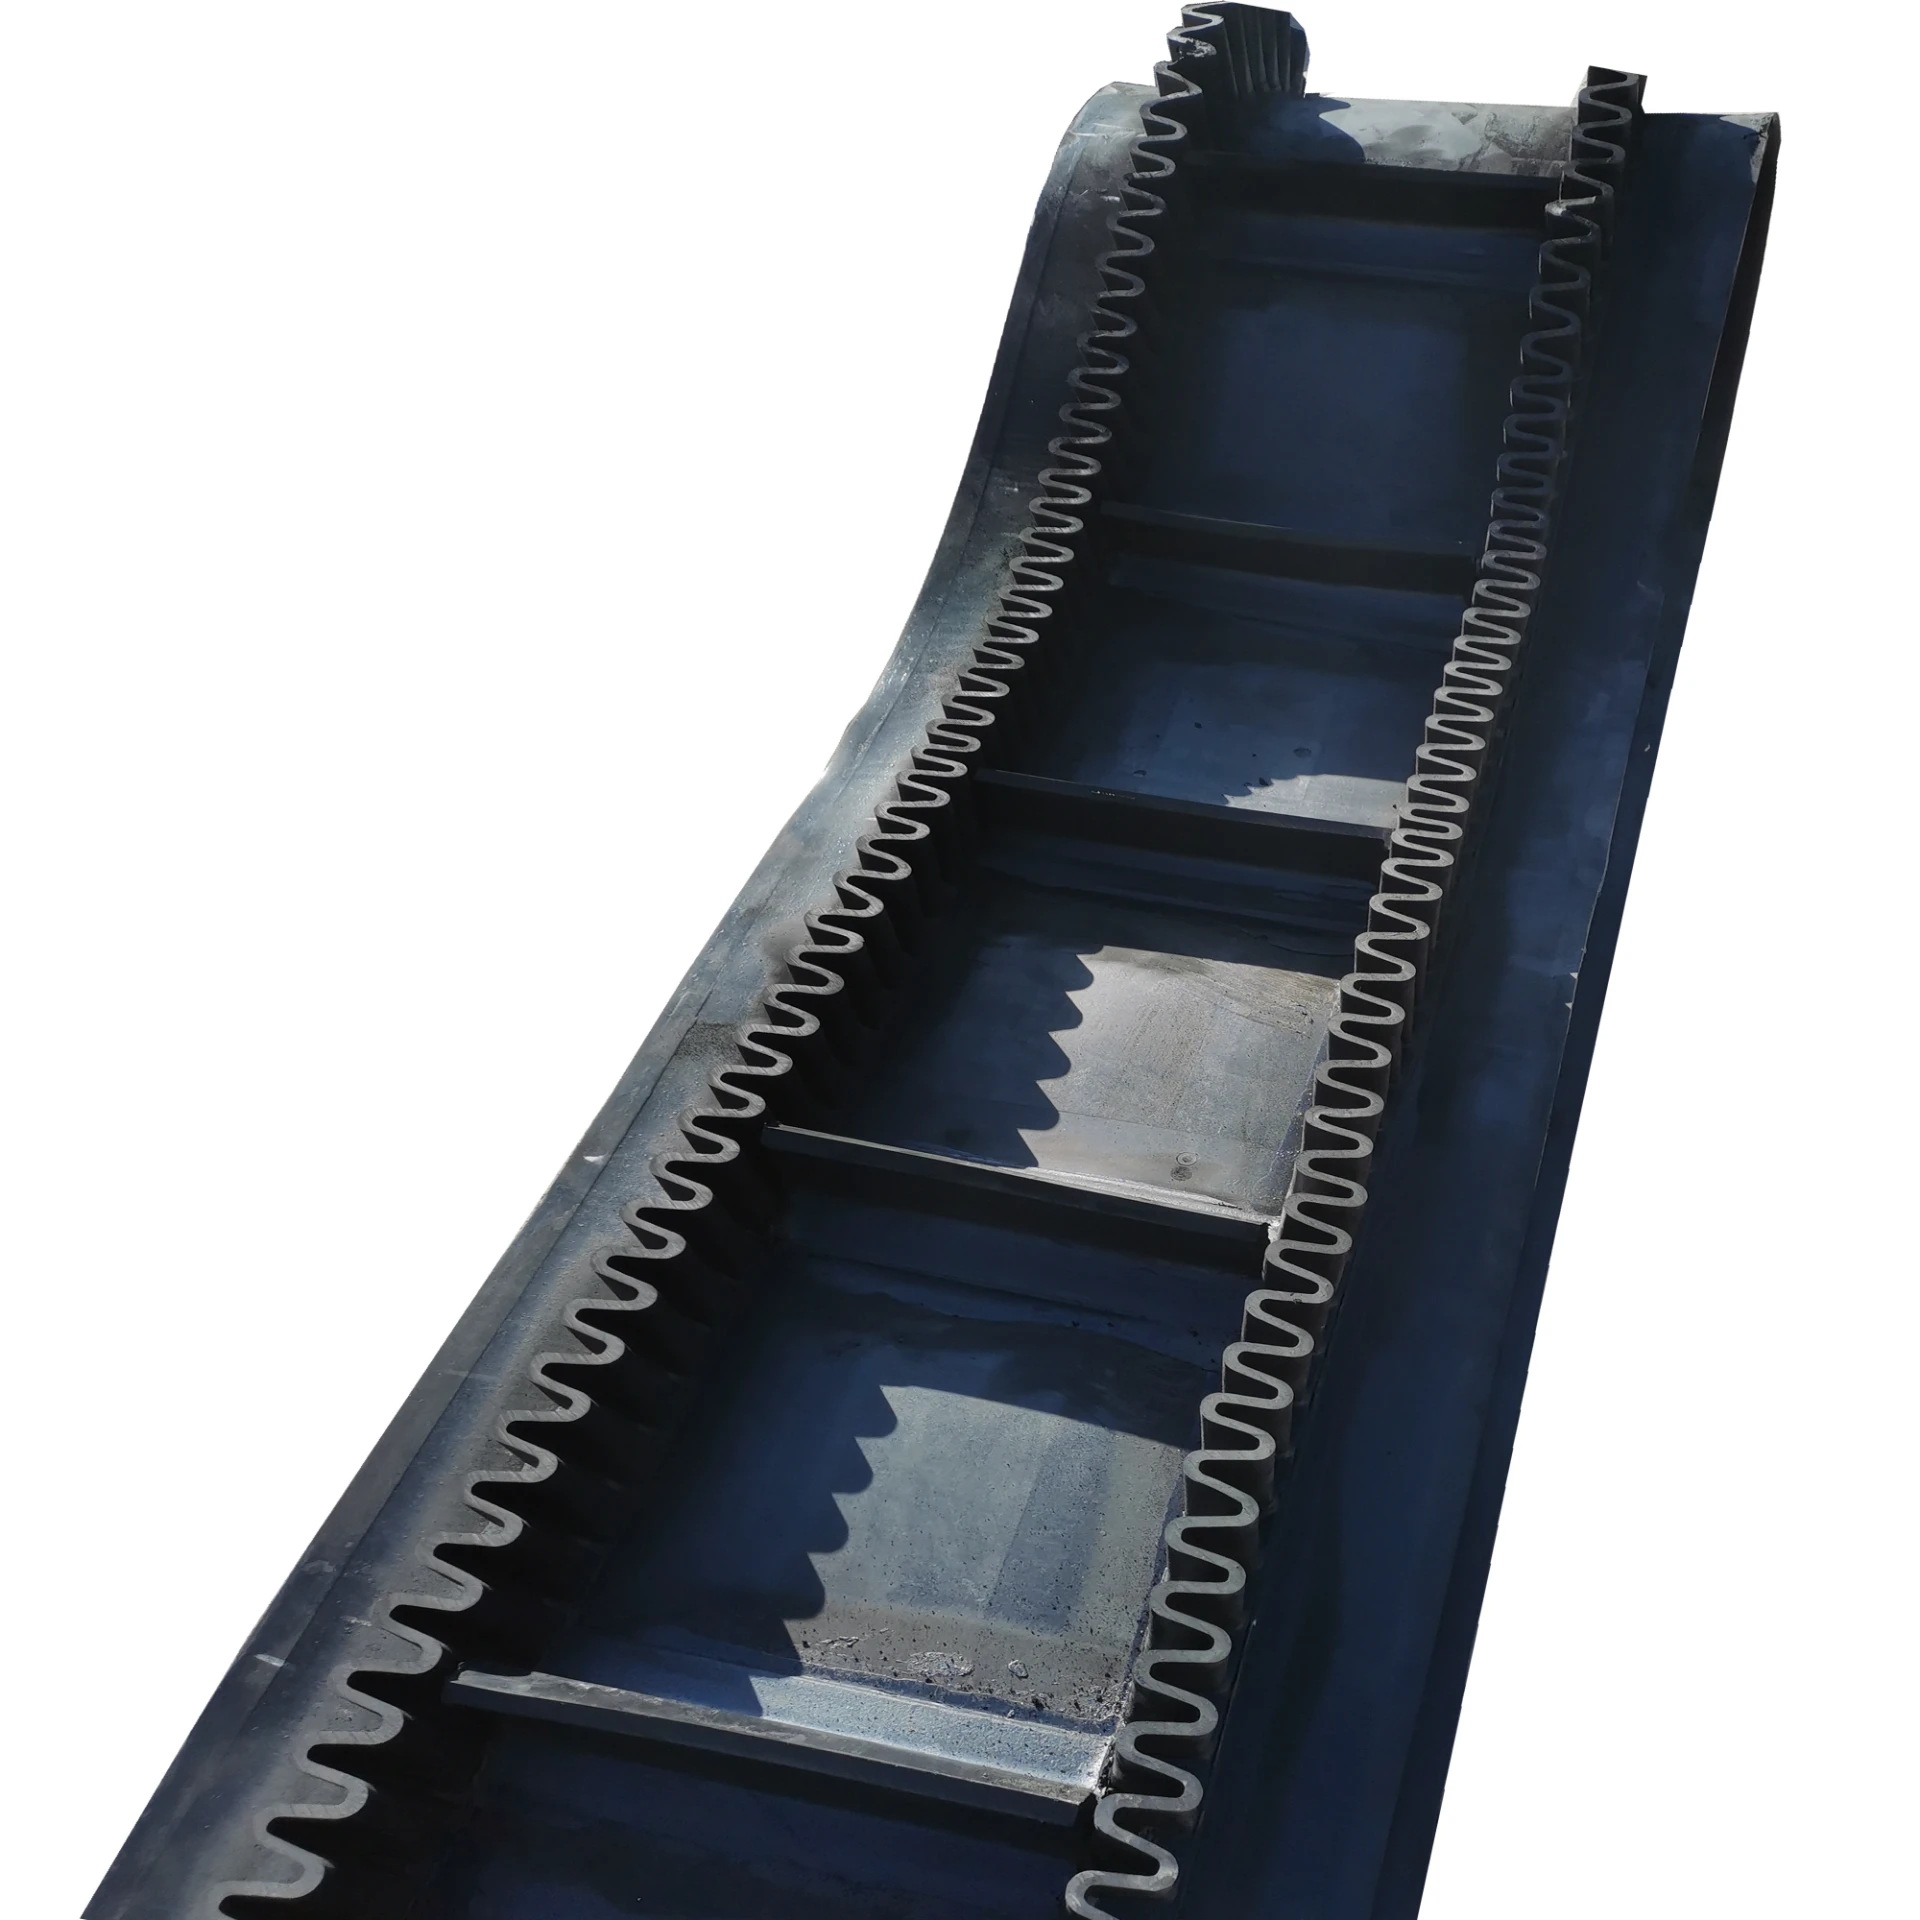
A resilient manufacturing plant relies on machinery that is both Durable and Easy-maintainable. Modern material conveyor systems incorporate advanced polymer composites, high-tensile nitrile rubber compounds, and reinforced polyester cores to withstand aggressive 24/7 load cycles without premature splice fatigue.
- CE Certification Compliance: Infrastructure designed with flame-retardant and anti-static properties, meeting strict international safety standards for enclosed industrial zones.
- Latest design Modularity: Standardized components allow for rapid on-site reconfiguration, drastically minimizing installation downtime.
- Advanced Material Science: Belts formulated for extreme abrasion and impact resistance, ensuring consistent throughput across diverse payloads.
Applications of the bulk material conveyor
Facilities managing raw extraction, aggregate processing, or heavy assembly require uncompromised structural integrity. Deploying a heavy-duty bulk material conveyor is the most Cost-Effective method for moving high-tonnage materials over long distances. We provide competitive Wholesale pricing models, ensuring that scaling your heavy-duty infrastructure remains Budget Friendly.
Flexibility & Deployment of the portable material conveyor
For dynamic logistics operations, warehousing units, and temporary staging areas, a portable material conveyor offers unmatched operational agility. These units allow plant managers to rapidly shift conveying lines where needed, reducing material handling bottlenecks and optimizing floor space utilization.
| Conveyor Type / Specification | Material Engineering | Primary Industrial Application | B2B Sourcing Advantage |
|---|---|---|---|
| Standard Industrial Belt | Nitrile Rubber / Polyester Core | Manufacturing Assembly, Warehousing | Low Price, High-volume Buy Discount |
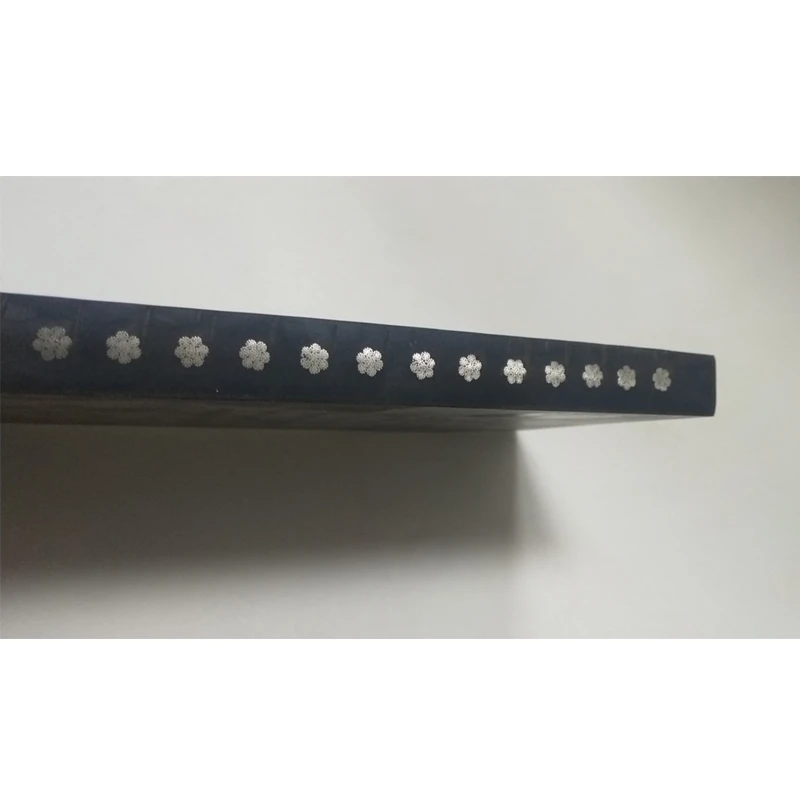
| Heavy-Duty Bulk Line | Steel Cord / Abrasion-Resistant Rubber | Mining, Cement, Aggregates | Custom OEM Sizing, Low Price per meter |
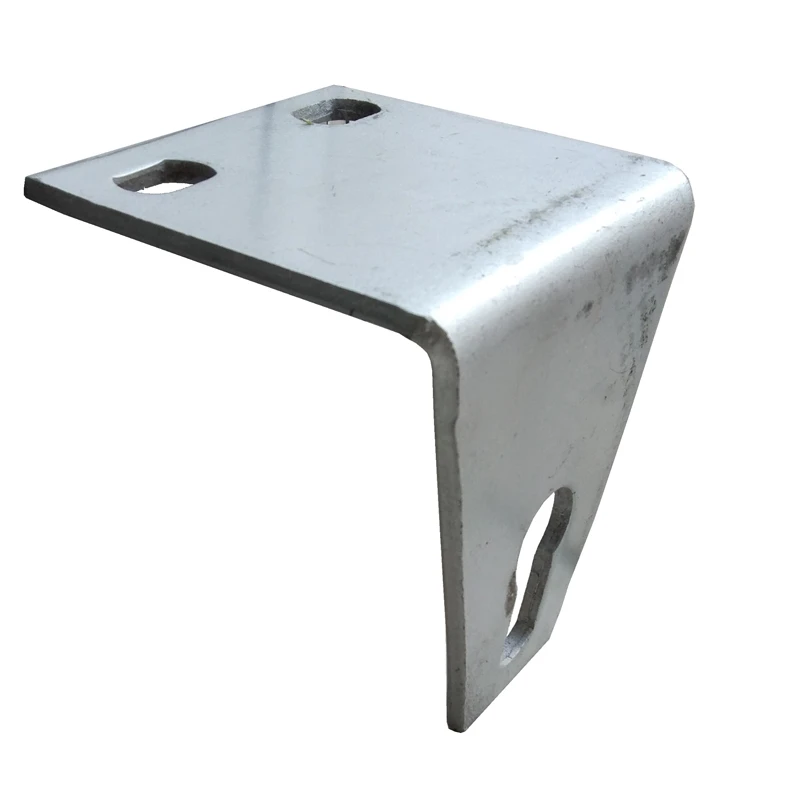
| Mobile Transfer Unit | Galvanized Carbon Steel Frames | Logistics Staging, Temporary Loading | Ready In Sales, Easy-maintainable |
B2B Supply Chain & Distributor FAQ
- Can our Company request a Free Sample of the belting material before confirming a bulk Purchase?
- Absolutely. We encourage engineering teams and Vendor networks to evaluate our material compounds for abrasion resistance and tensile strength. Once validated, our technical sales team will issue a comprehensive Quotation tailored to your project scope.
- Do you provide any material conveyor for sale with international warranties?
- Yes. Every material conveyor for sale in our catalog comes with up to a 3-year warranty and full CE Certification, ensuring complete reliability for your international distribution network.
- What are the typical lead times for bulk Wholesale orders?
- Standard modular components are kept In Sales inventory and can be dispatched within 7-10 days. For highly Custom engineered production runs, our efficient supply chain requires 20-30 days to fulfill full container loads for export.
Optimize Your Facility's Material Handling Infrastructure
Partner with an industry-leading Exporter to protect your supply chain and optimize your procurement budget. Contact our engineering sales division to discuss technical specs and secure your competitive Wholesale pricing.
Request a B2B Quotation