Why Stainless Steel Conveyors Are Essential in Modern Industry
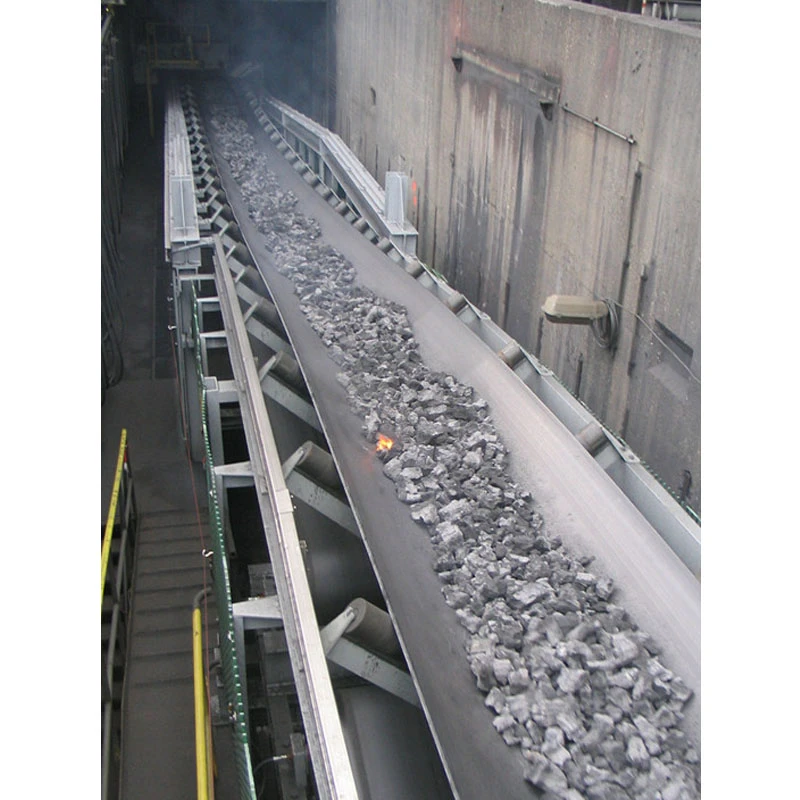
Having spent a fair number of years amidst factories and production lines, I can say that stainless steel conveyors have quietly become the unsung heroes of industrial workflows. You might be surprised how integral they are, especially when dealing with demanding environments, from food processing plants to pharmaceutical setups. stainless steel conveyor systems aren’t just about moving stuff—they’re about reliability, hygiene, and longevity.
What’s interesting is that stainless steel’s resistance to corrosion often means these conveyors outlast many other components on the line. I remember working in a meat processing facility where regular plastic belts just wouldn’t hold up to the constant moisture and cleaning regimes. Switching to stainless steel conveyors was a game changer—fewer breakdowns, less downtime, and frankly, easier sanitation.
From my perspective, the choice of material affects so many downstream factors — contamination control, maintenance schedules, even worker safety. It’s not just the surface you see; it’s an entire design philosophy that prioritizes durability and efficiency. Many engineers I know insist on 304 or 316 stainless steel grades, especially where food contact or harsh chemicals are involved.
Key Product Specifications of Stainless Steel Conveyors
| Specification | Typical Value | Notes |
|---|---|---|
| Material Grade | 304 / 316 Stainless Steel | Depends on corrosion resistance needs |
| Belt Width | 100mm to 2000mm | Custom sizes available |
| Surface Finish | #4 Brushed, Mirror, or Matte | Affects cleaning & appearance |
| Load Capacity | Up to 500 kg/m | Varies by design & belt type |
| Temperature Range | -20°C to +150°C | Suitable for various industries |
| Sanitization | Clean-In-Place (CIP) compatible | Essential for food & pharma sectors |
Customization is another fascinating area. Over the years, I’ve seen designs tailored with modular belts, side guards, or even sensors embedded for automated monitoring. Oddly enough, many companies underestimate the value of adaptable conveyors until they’re faced with production line changes or new product launches.
Comparing Leading Stainless Steel Conveyor Vendors
| Feature | Vendor A | Vendor B | Vendor C |
|---|---|---|---|
| Lead Time | 4 weeks | 6 weeks | 3 weeks |
| Customization Options | High (modular belts, sensors) | Medium (standard add-ons) | Low (mostly standard models) |
| After-Sales Support | Comprehensive training & spare parts | Limited remote support | Basic support only |
| Price Range | $$$ (Premium) | $$ (Mid-range) | $ (Budget) |
| Compliance Certifications | ISO 22000, FDA | ISO 9001 | None reported |
One more thing — in real terms, the logistics around installation and maintenance can make or break how these conveyors perform on the shop floor. I recall a client who was initially skeptical about investing heavily but ended up saving costs by reducing downtime by over 30% within a year.
Ultimately, stainless steel conveyors offer robust, hygienic, and versatile solutions that keep industries moving forward with greater confidence. If you’re considering an upgrade, it's worth checking out the options at stainless steel conveyor specialists who really get the balance between engineering precision and practical needs.
To wrap up—whether you’re in food processing, pharmaceuticals, or even automotive parts, investing in a quality stainless steel conveyor pays dividends in productivity and peace of mind.
References:
1. Food Engineering Magazine - Conveyor Sanitation Best Practices (2022)
2. International Stainless Steel Forum - Industry Guidelines (2023)
3. Interview with Plant Manager, Midwest Food Processors (2021)