In high-capacity mining operations, bulk processing plants, and strict environmental compliance facilities, transporting hazardous or dusty bulk materials across varying topographies while eliminating dust emissions is critical to plant profitability. Sourcing a High-Quality tunnel conveyor directly from an advanced Manufacturer in China empowers global OEMs, system integrators, and industrial distributors to secure Advanced, CE Certified enclosed transport infrastructure while strictly controlling CapEx and ensuring zero material loss.
Table of Contents: B2B Sourcing Guide
- Structural Engineering & Enclosed Casing Metallurgy
- Mechanical Specifications & High-Tonnage Performance
- Wholesale Cost Analysis & ROI
- OEM Customization & Distributor FAQ
Structural Engineering & Enclosed Casing Metallurgy
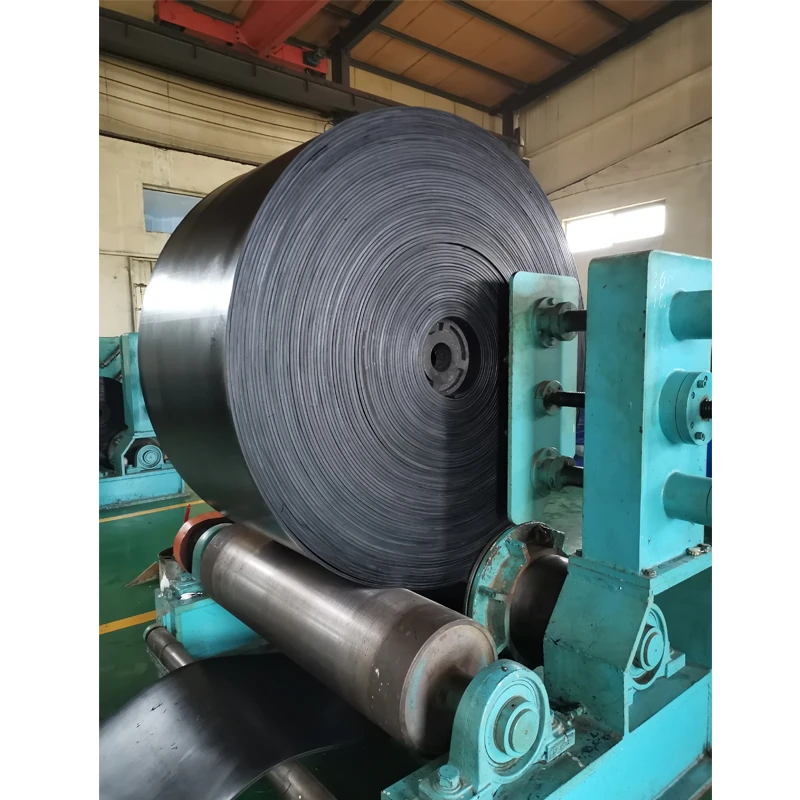
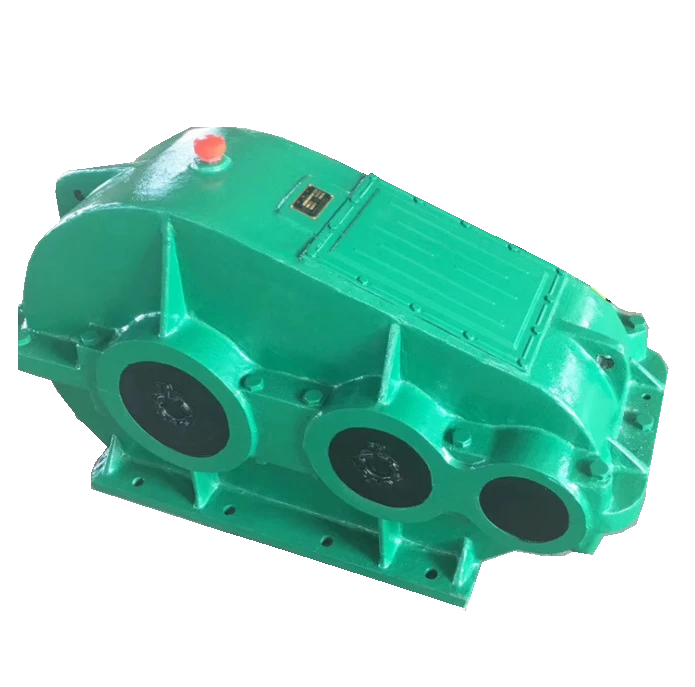
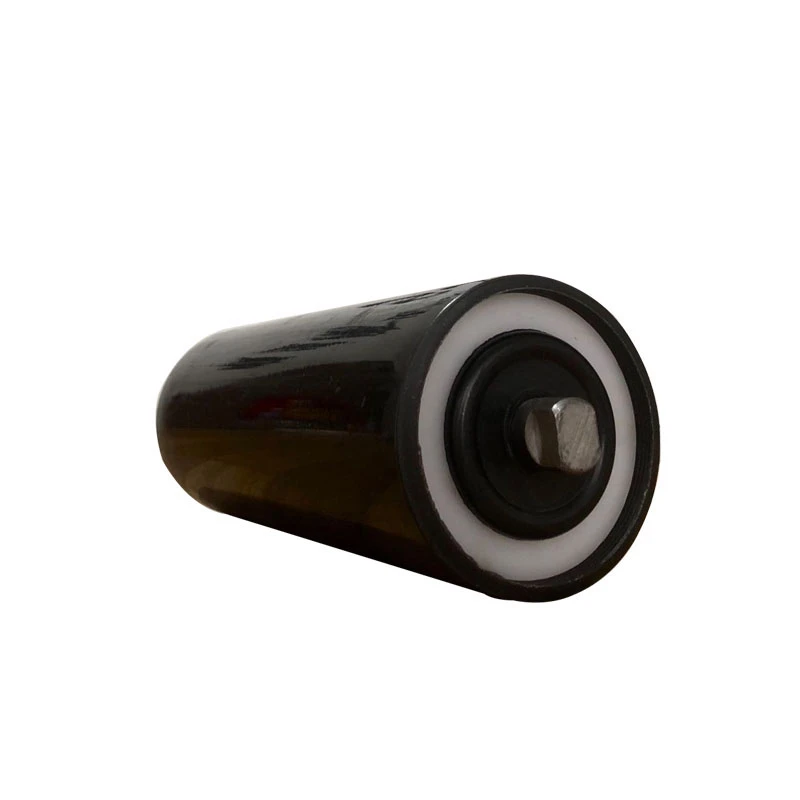
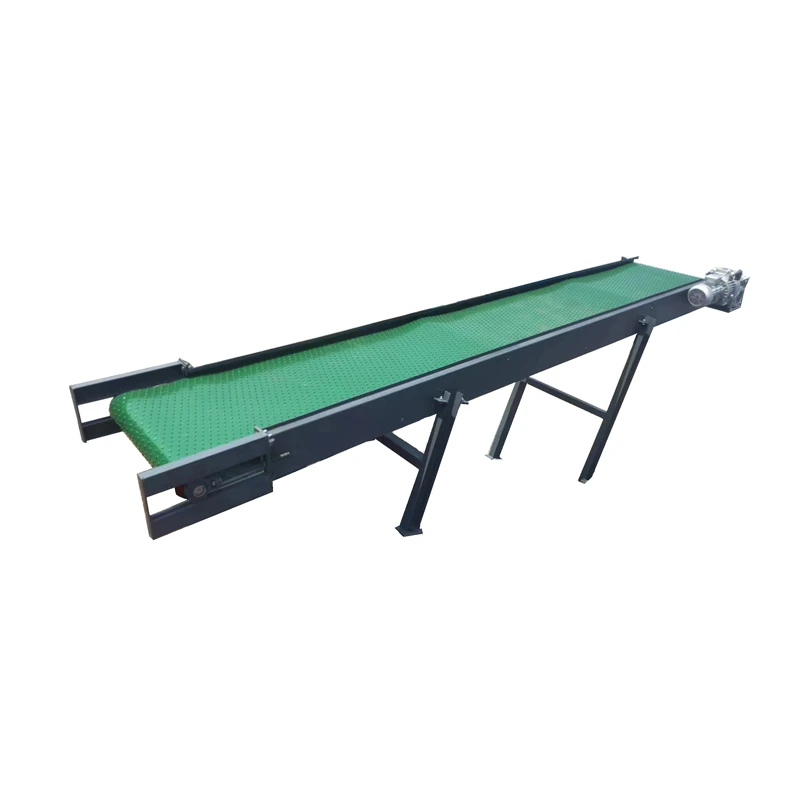
A resilient processing plant relies on bulk transport machinery that is both Durable and Easy-maintainable under continuous 24/7 operating schedules. Modern tunnel conveyor systems incorporate robust steel enclosures, impact-resistant belting, and heavy-duty rollers housed within protective casings, shielding transported solids from weather elements while containing fugitive dust and regulating environmental factors.
- CE Certification Compliance: Our manufactured enclosed transport assemblies meet rigorous international safety and environmental regulations, featuring superior dust suppression.
- Latest design Modularity: Standardized belt widths ranging from 500 mm to 2000 mm and custom conveying lengths up to 1000 meters allow facility engineers to scale bulk transport smoothly.
- Advanced Thermal Tolerance: Engineered specifically to operate reliably across extreme temperature ranges from -20°C to 60°C under heavy multi-shift workloads.
Mechanical Specifications & High-Tonnage Performance
Facilities managing coal, mineral ores, bulk solids, or packaged goods require uncompromised structural reliability. Deploying an engineered enclosed conveying line guarantees stable, high-volume throughput up to 1,200 tons per hour across uphill, downhill, or restricted space topographies.
| Conveyor Specification | Material Engineering & Parameters | Primary Industrial Application | B2B Sourcing Advantage |
|---|---|---|---|
| Standard Enclosed Transport Line | 500 mm – 2000 mm Width, Cased Housing | Bulk Mineral Processing, Coal Transfer | Low Price, High-Volume Buy Discount |
| High-Capacity Long-Span Unit | Up to 1,000 m Length, 1,200 tons/hour Capacity | Mining Operations, Aggregates Staging | CE Certified, High Durability, Ready In Stock |
| Extreme Weather Enclosed System | Impact-Resistant Belts, -20°C to 60°C Rating | Outdoor Industrial Terminals, Chemical Plants | Custom OEM Sizing, Advanced Design |
B2B Supply Chain & Distributor FAQ
- Can your Company accommodate Custom OEM/ODM orders for tunnel conveyors?
- Yes. As a primary Manufacturer and Exporter, we specialize in comprehensive OEM/ODM fabrication, tailoring belt widths, casing configurations, and total conveying lengths to meet your exact plant site constraints.
- Do you provide a Free Sample or pilot evaluation prior to bulk purchase?
- Absolutely. We encourage engineering teams and Vendor networks to request component data packages or technical specification blueprints. Once evaluated, our sales team will issue a formal Quotation tailored to your Wholesale volume.
- What are the typical lead times for international Exporter logistics?
- Standard modular components are kept In Sales inventory and can be dispatched rapidly. For fully engineered, large-scale systems backed by a 24-month warranty, our production facilities ensure reliable container loading for export.
Optimize Your Facility's Enclosed Bulk Material Transport
Partner with an industry-leading Manufacturer to protect your supply chain and streamline your procurement budget. Contact our engineering sales division to discuss technical specs and secure your competitive Wholesale pricing.
Request a Custom B2B Quotation